Selection guide
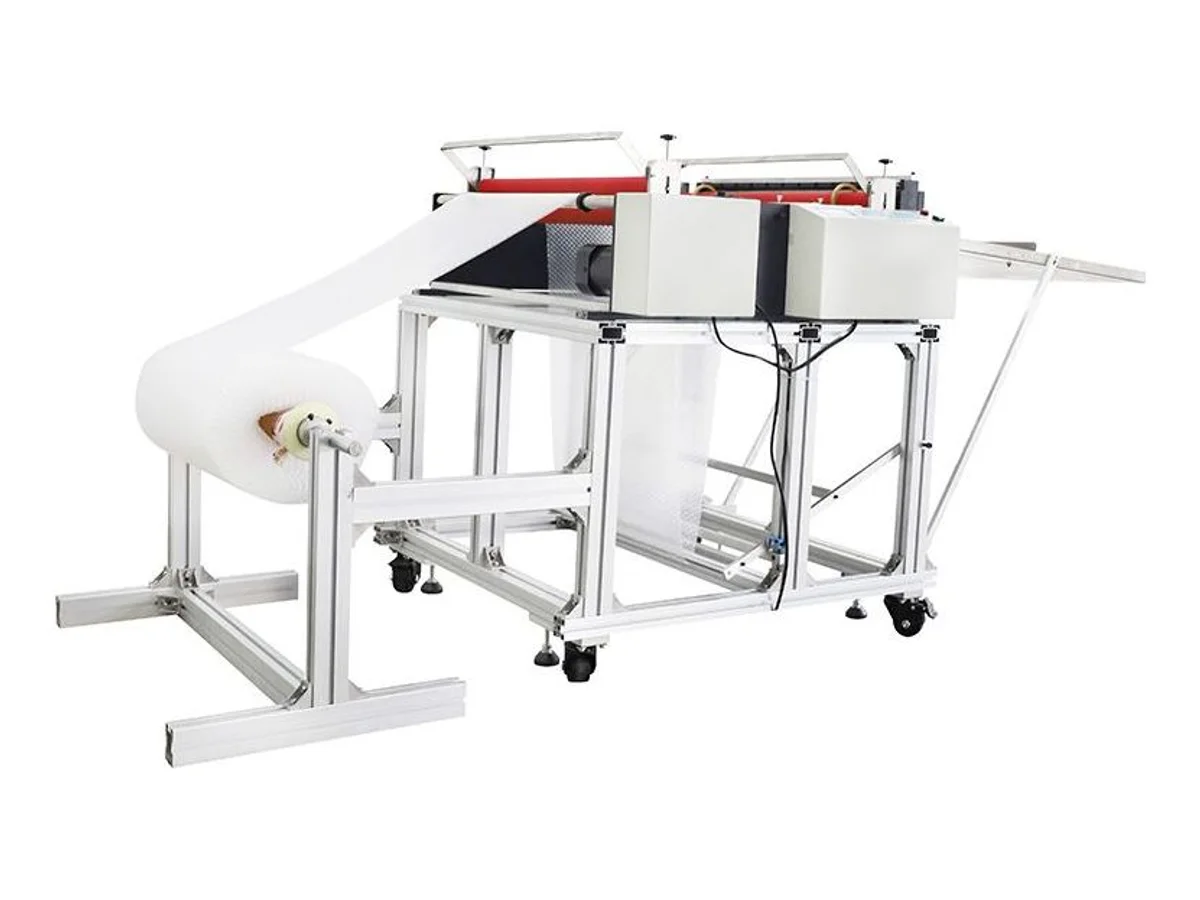
Can One Cutter Process Bubble Wrap and Paper Rolls?
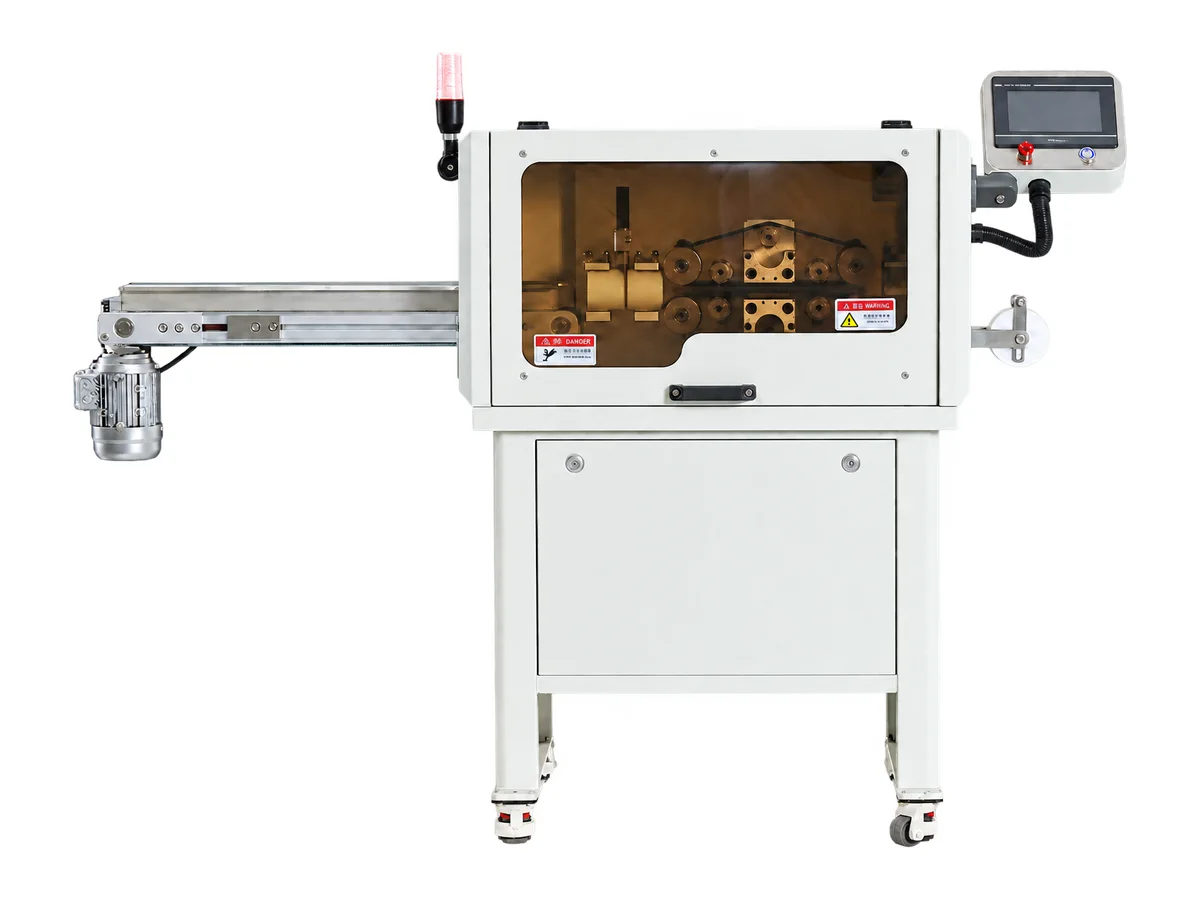
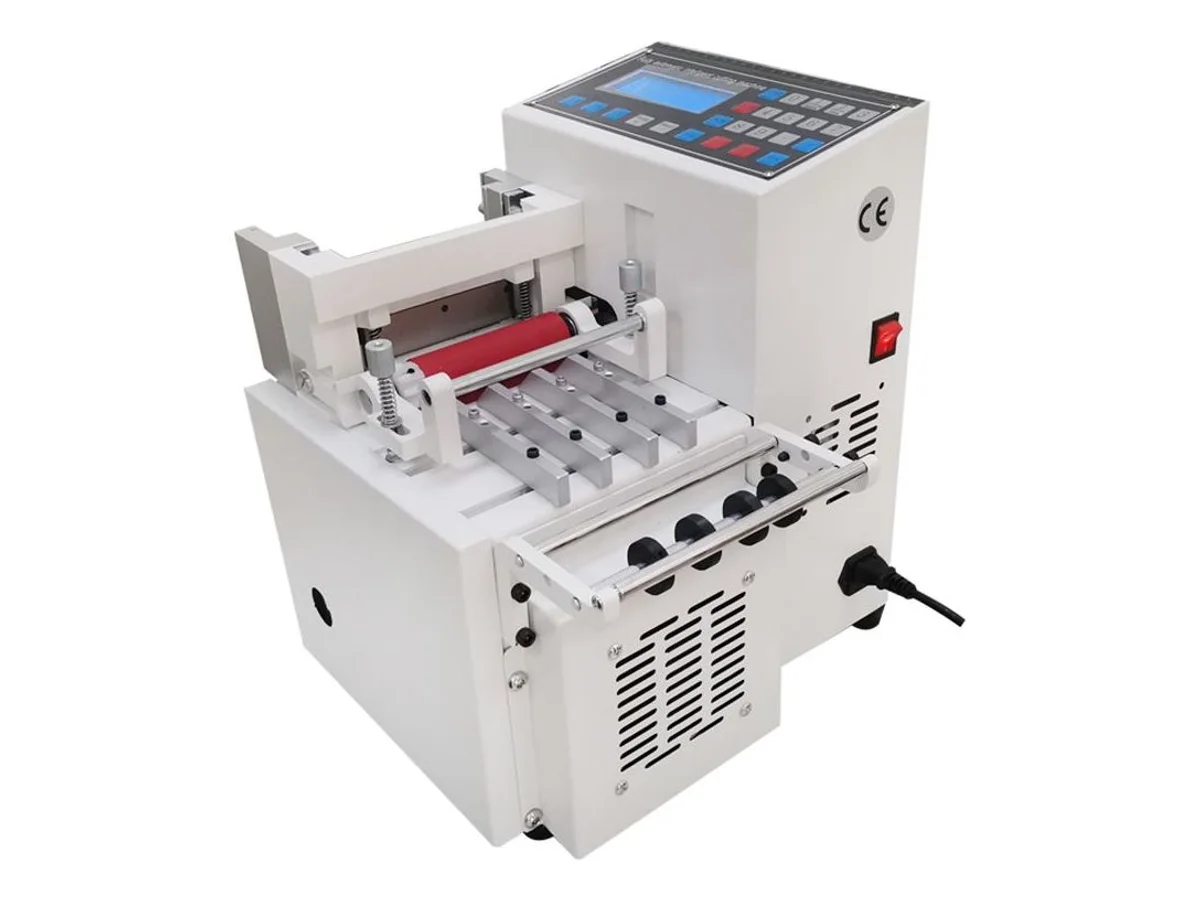
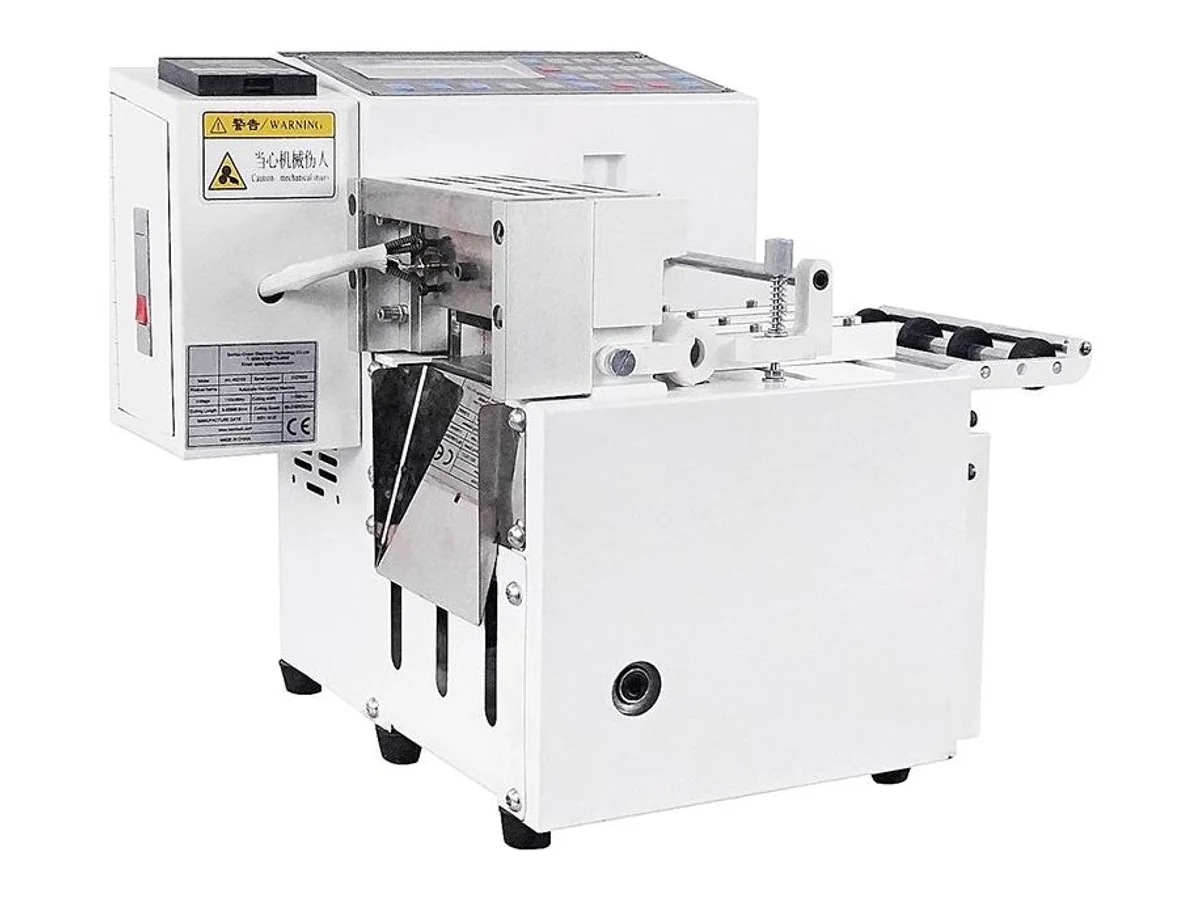
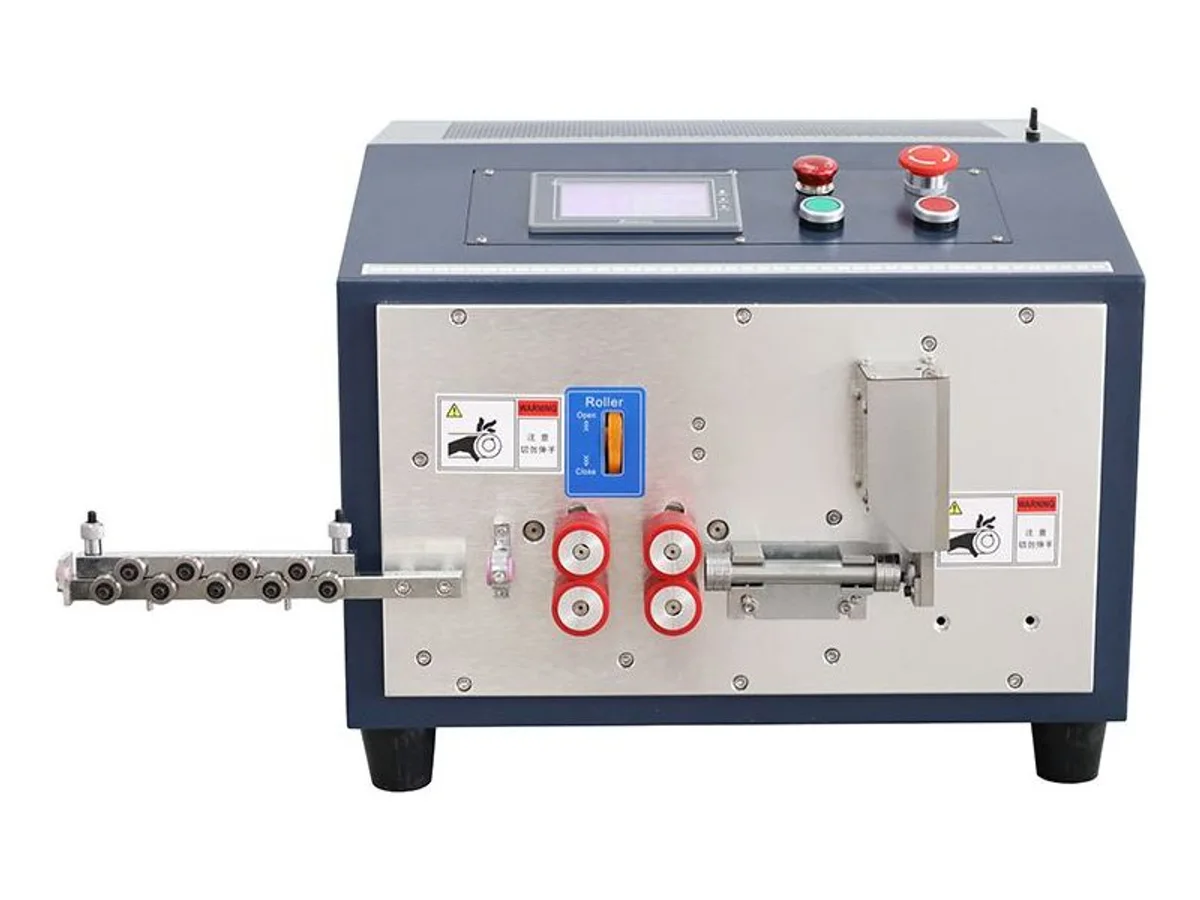
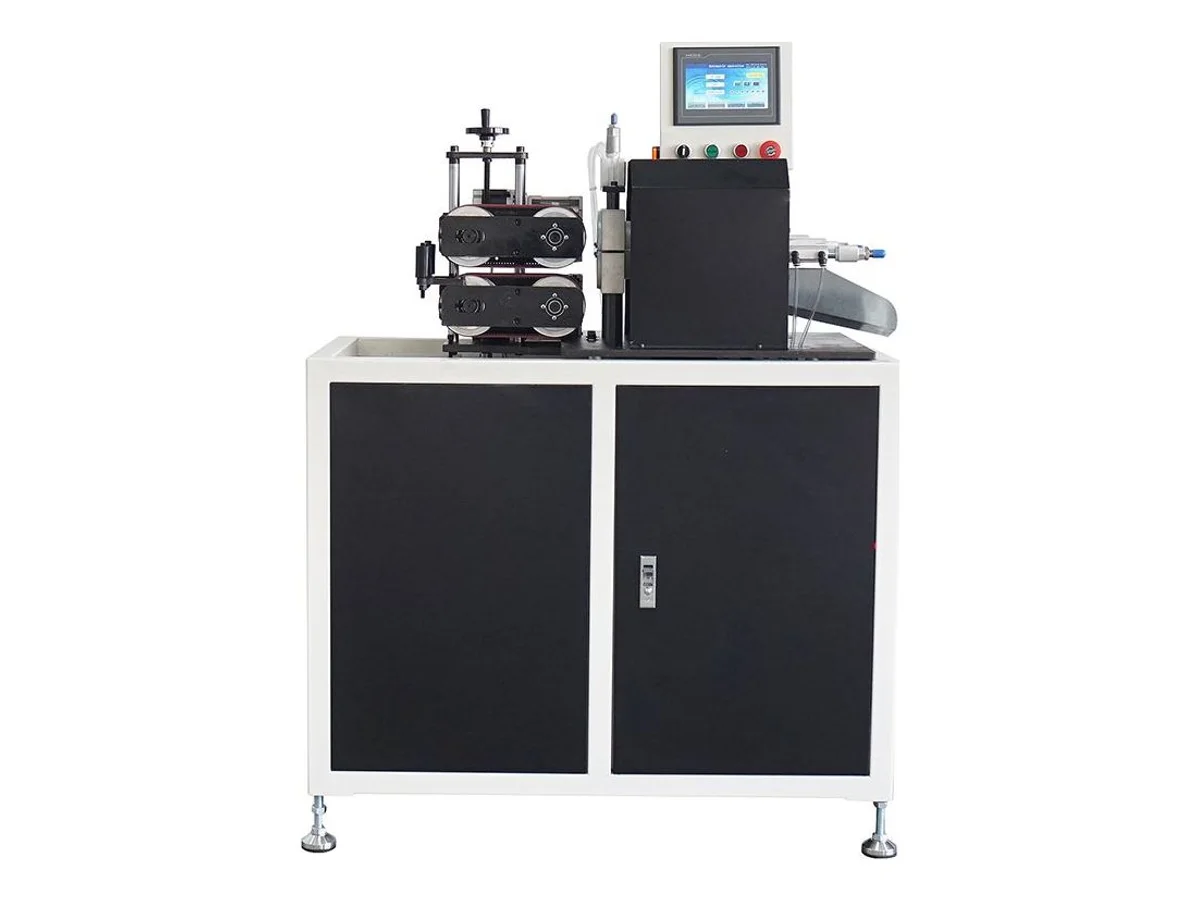
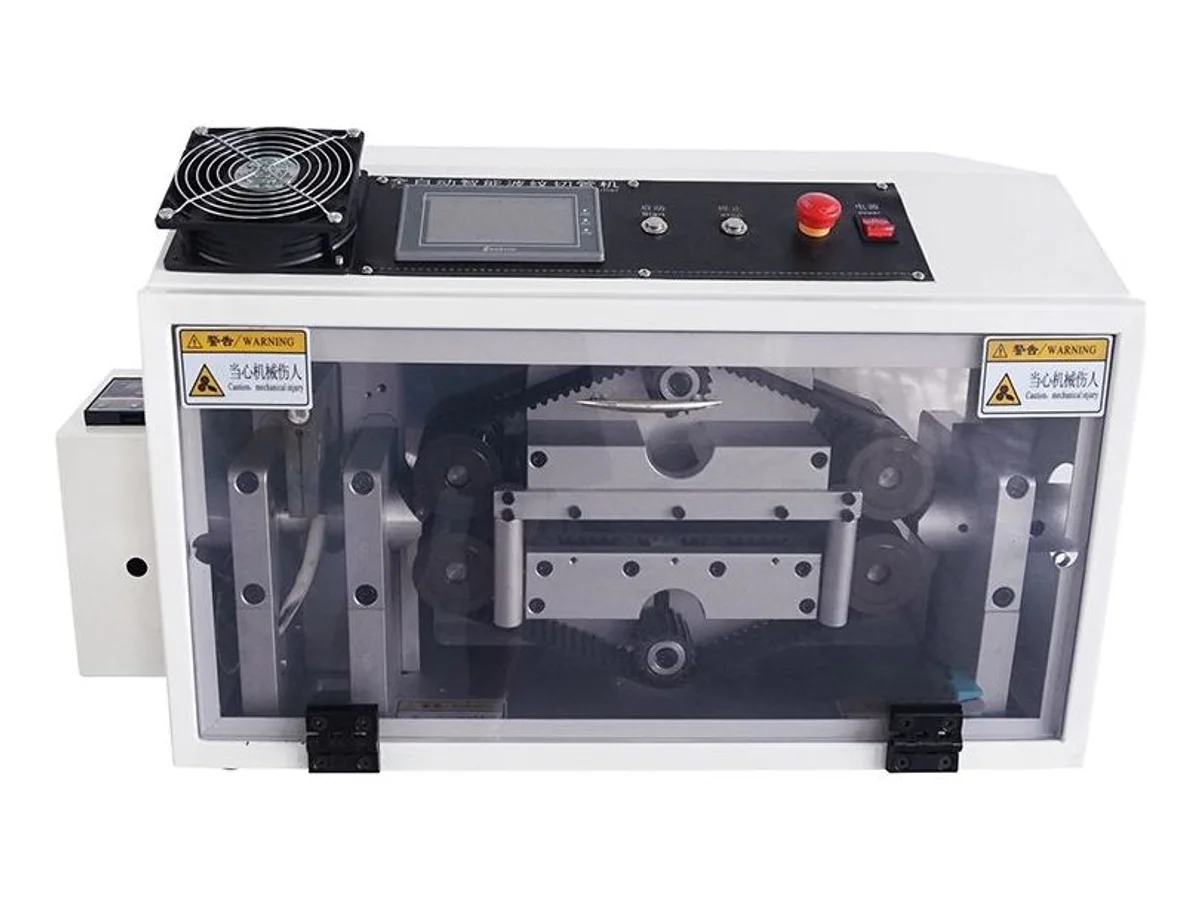
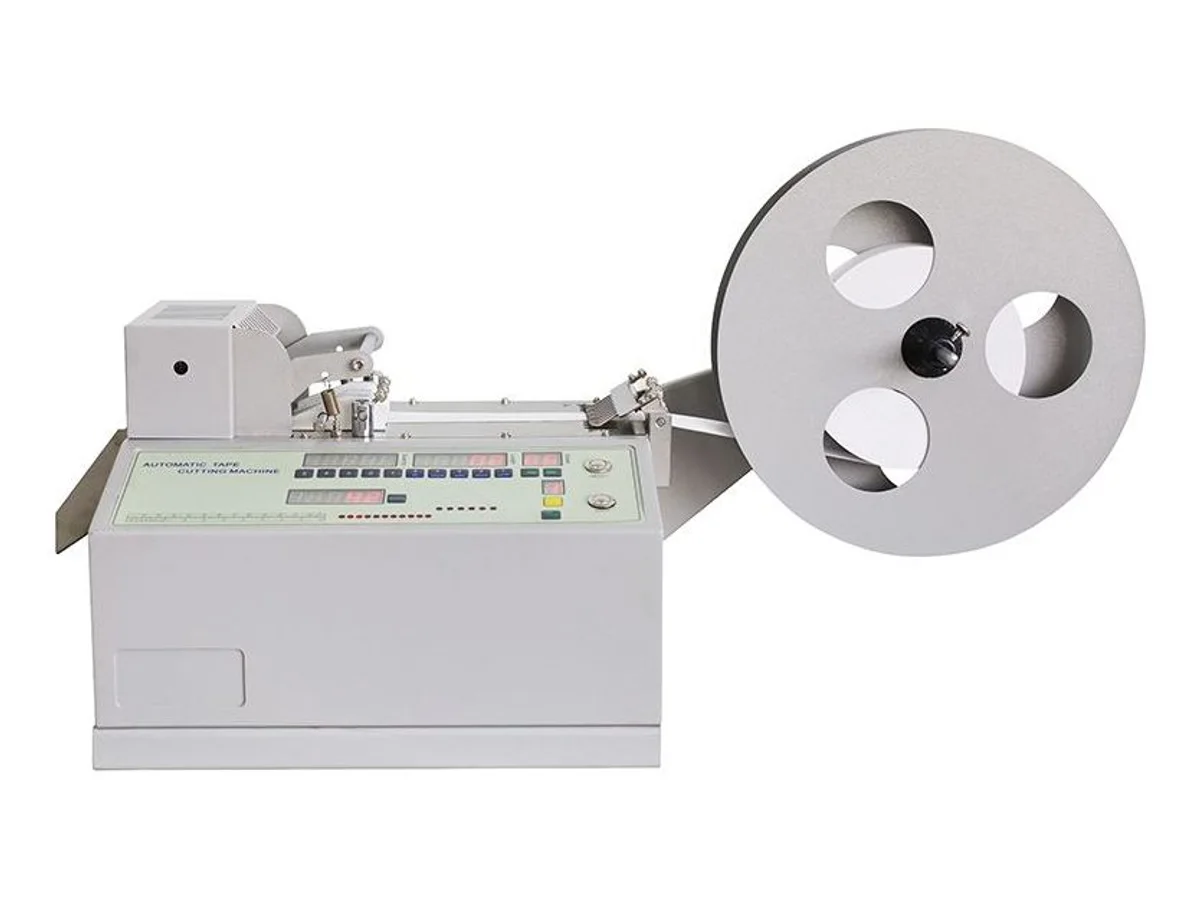
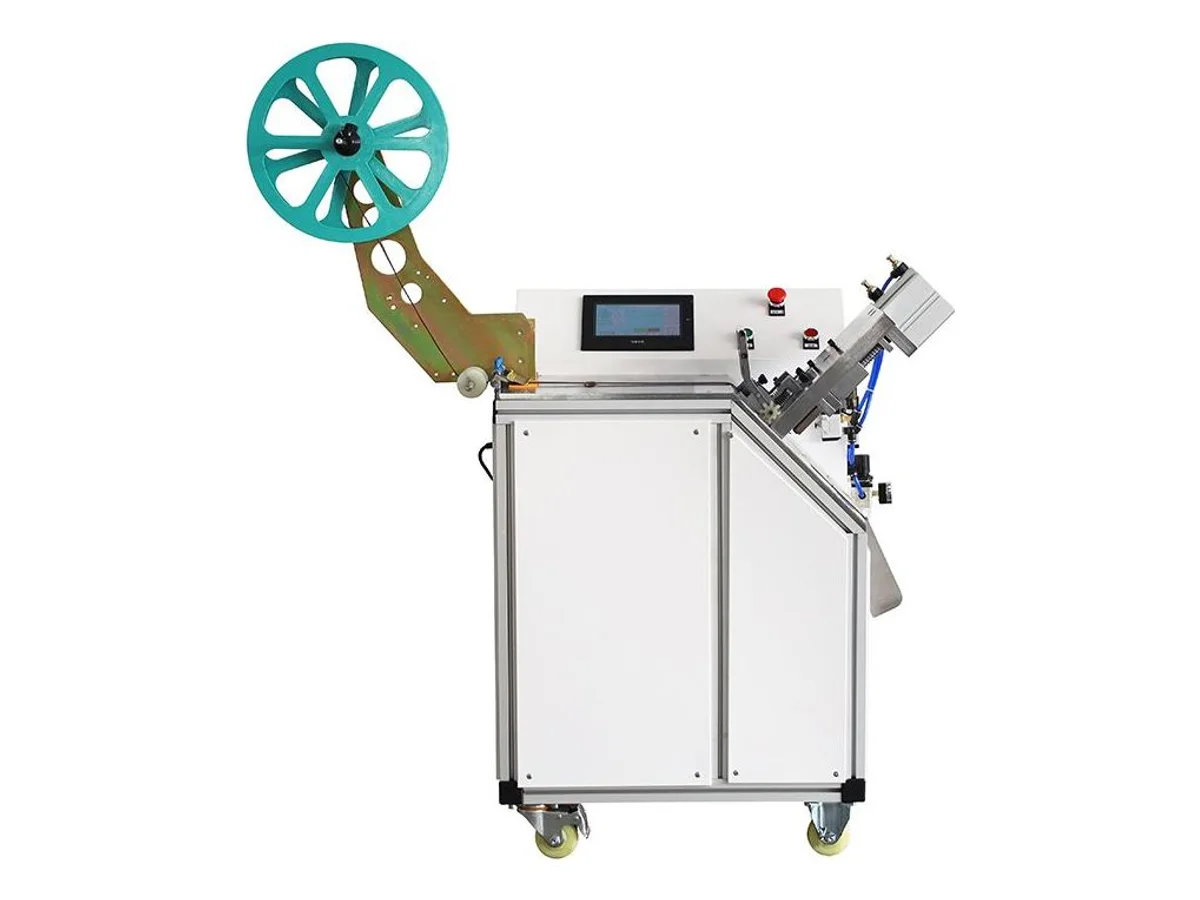
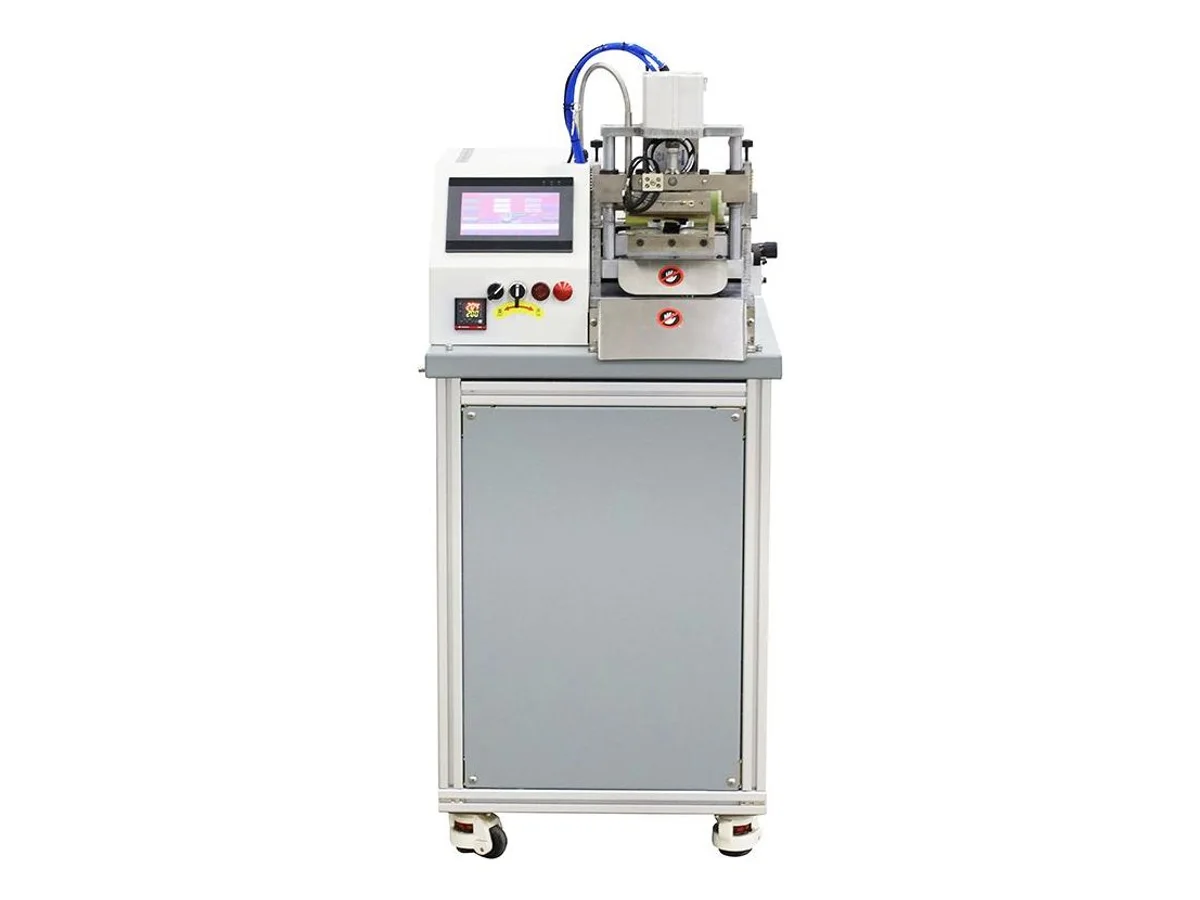
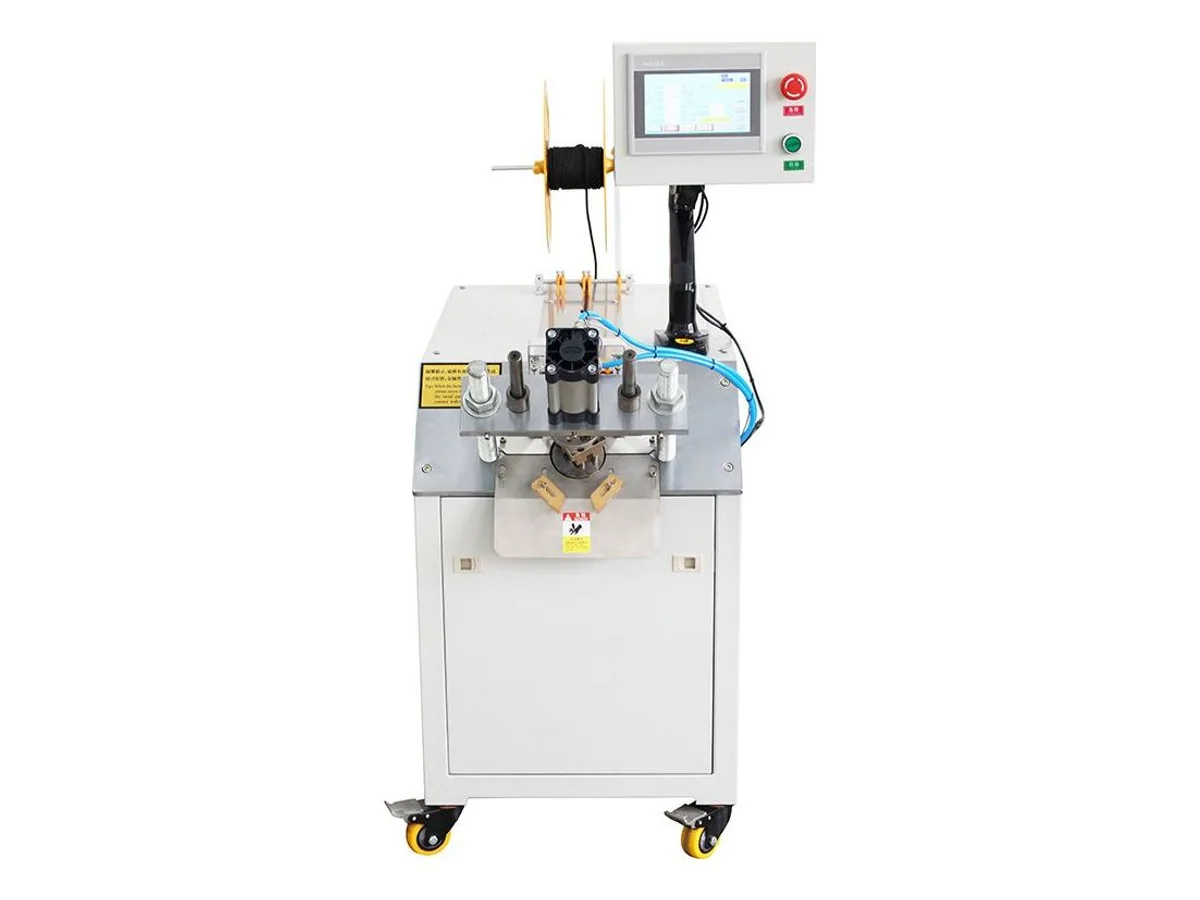
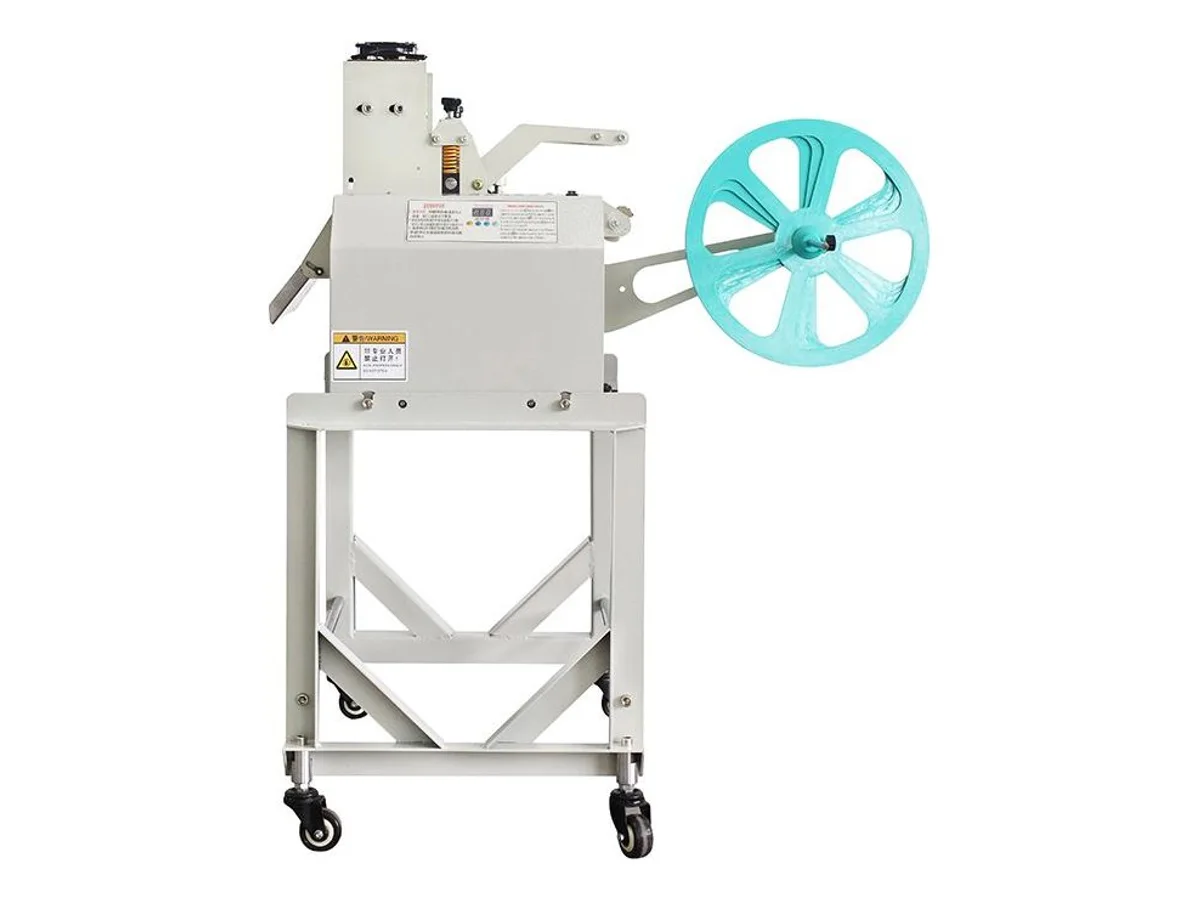
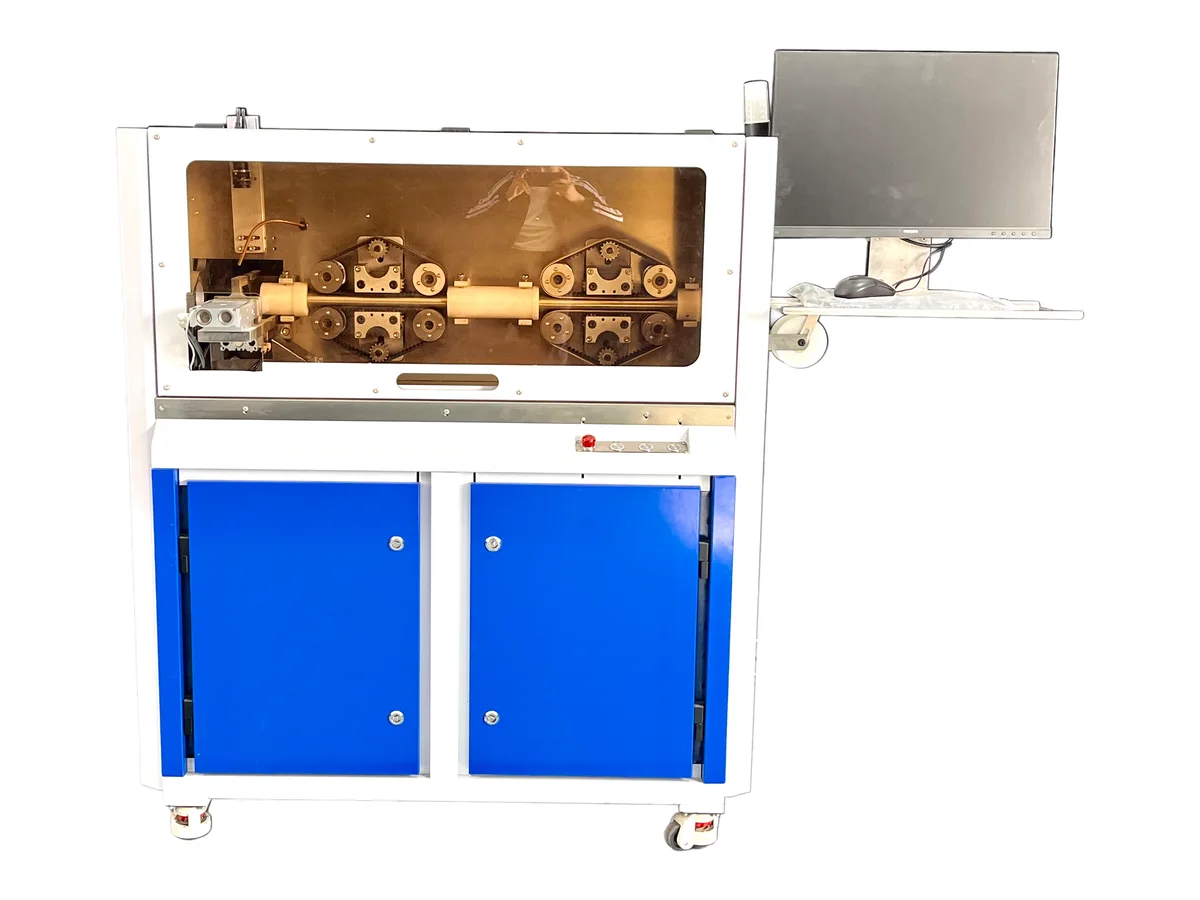
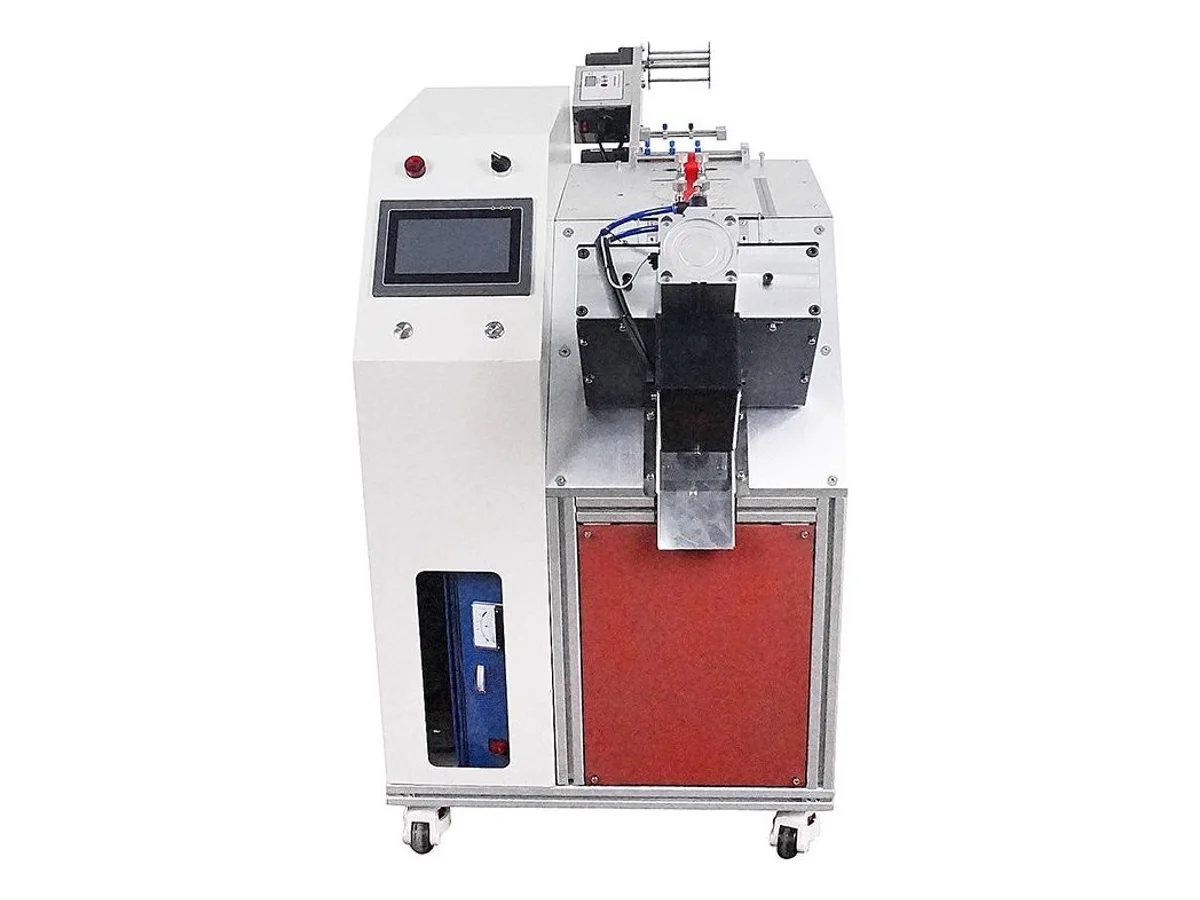
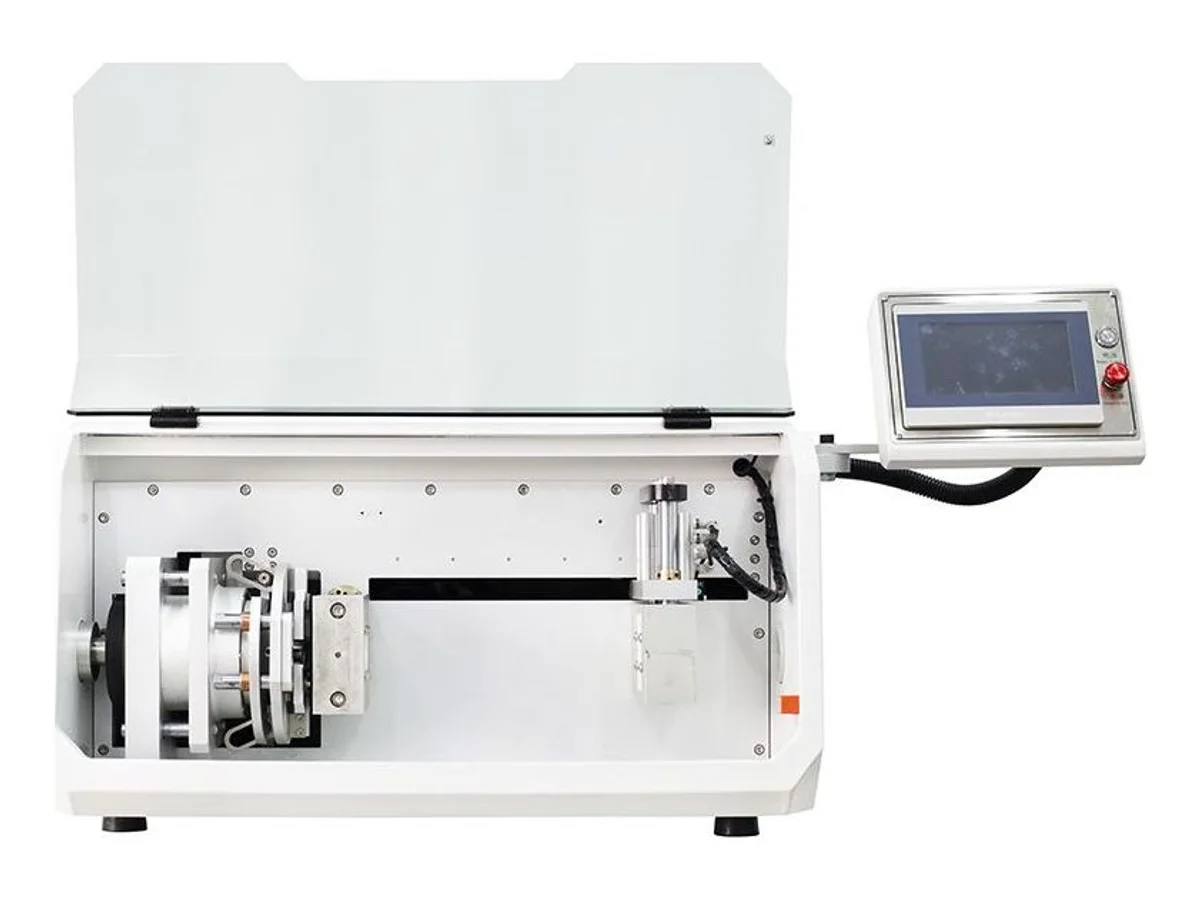
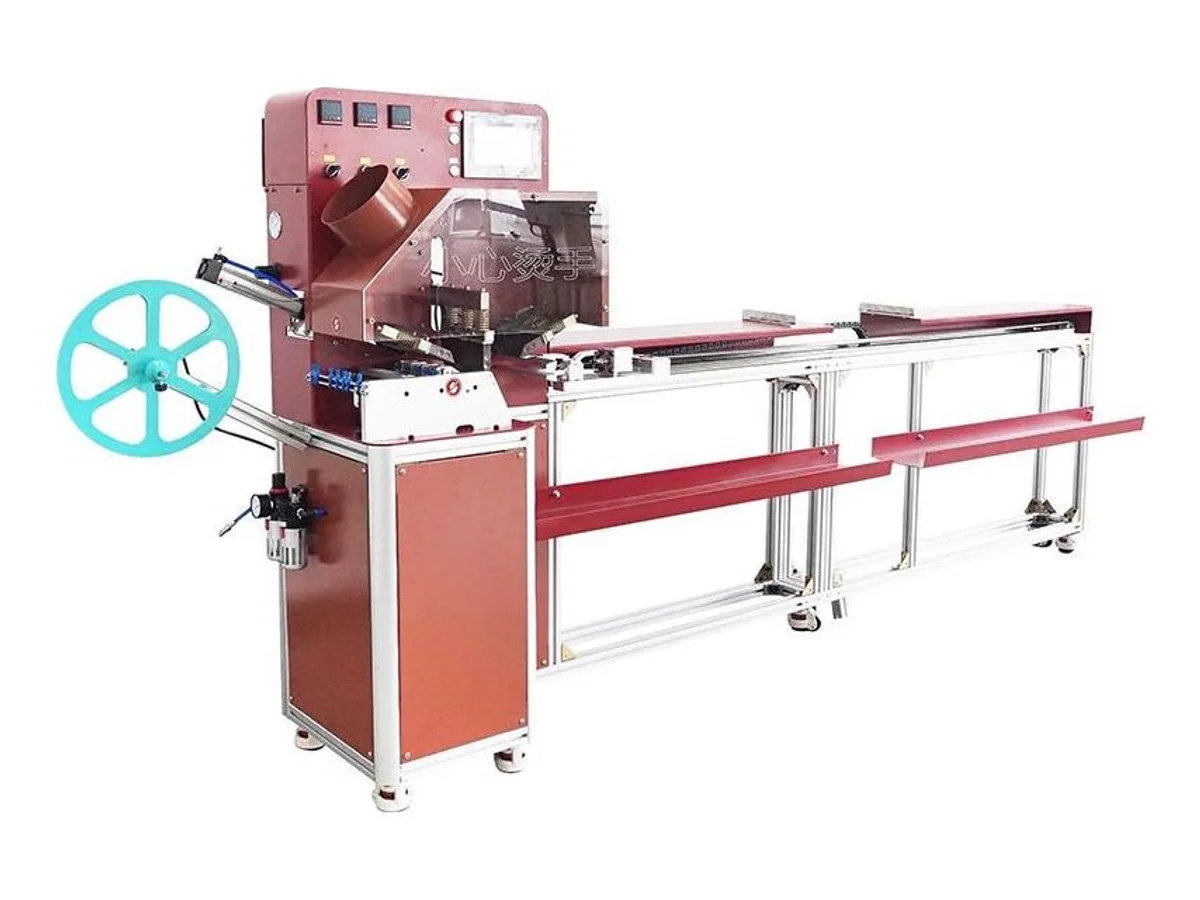
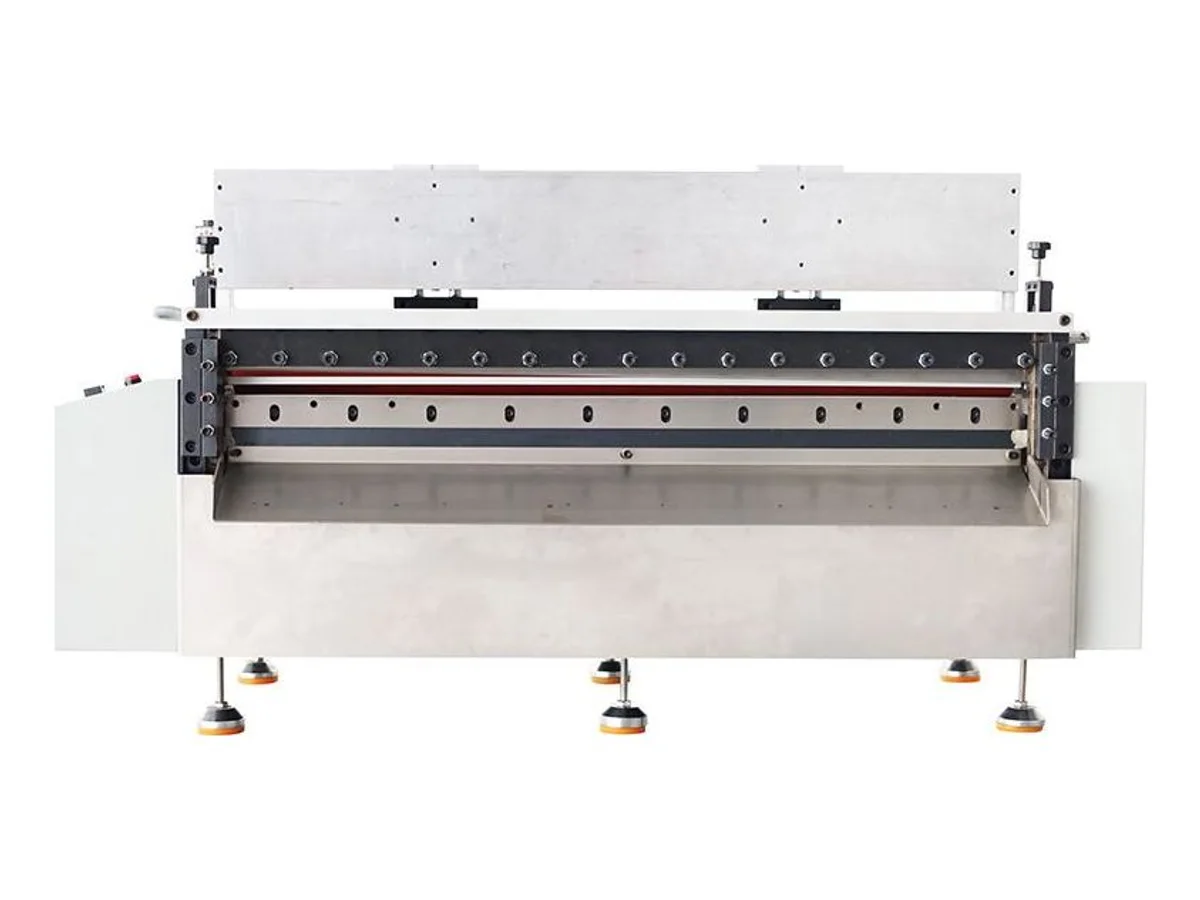
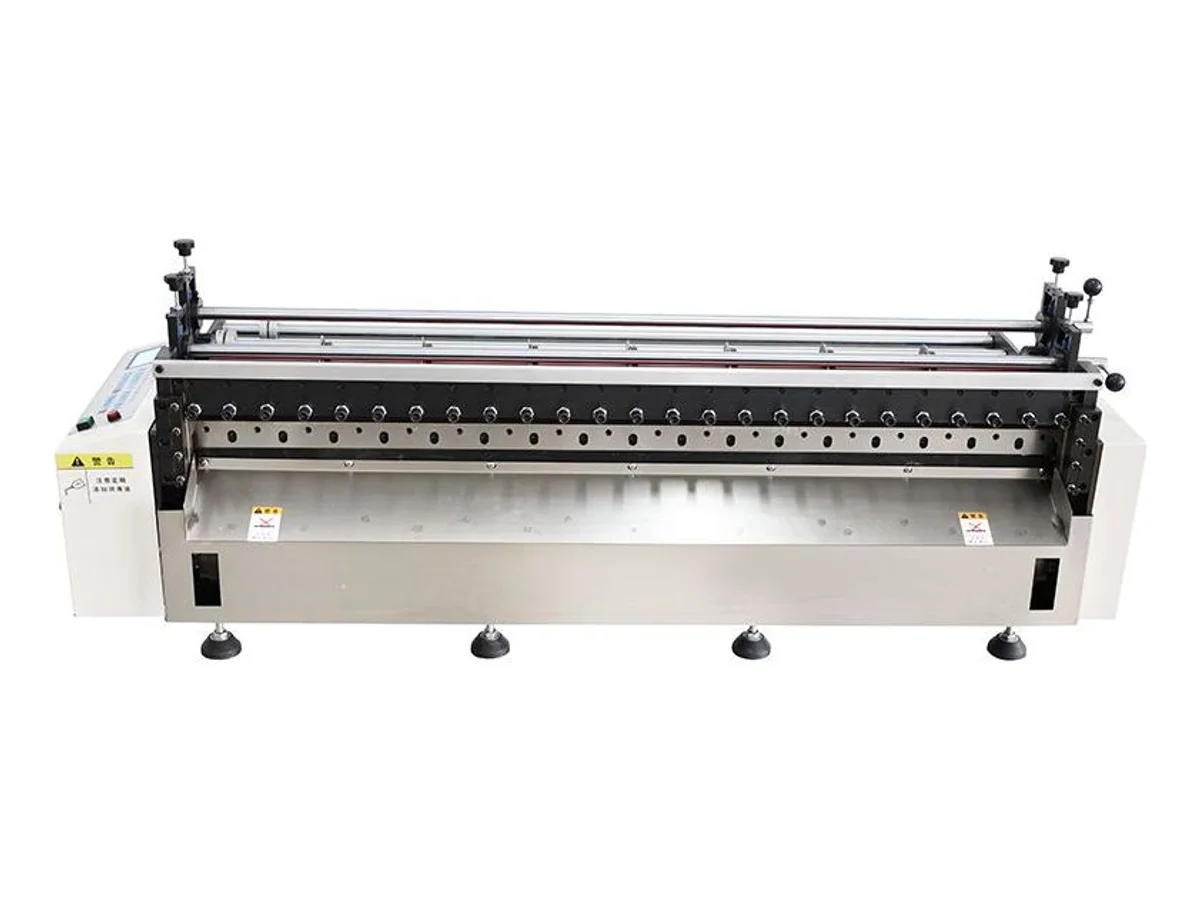
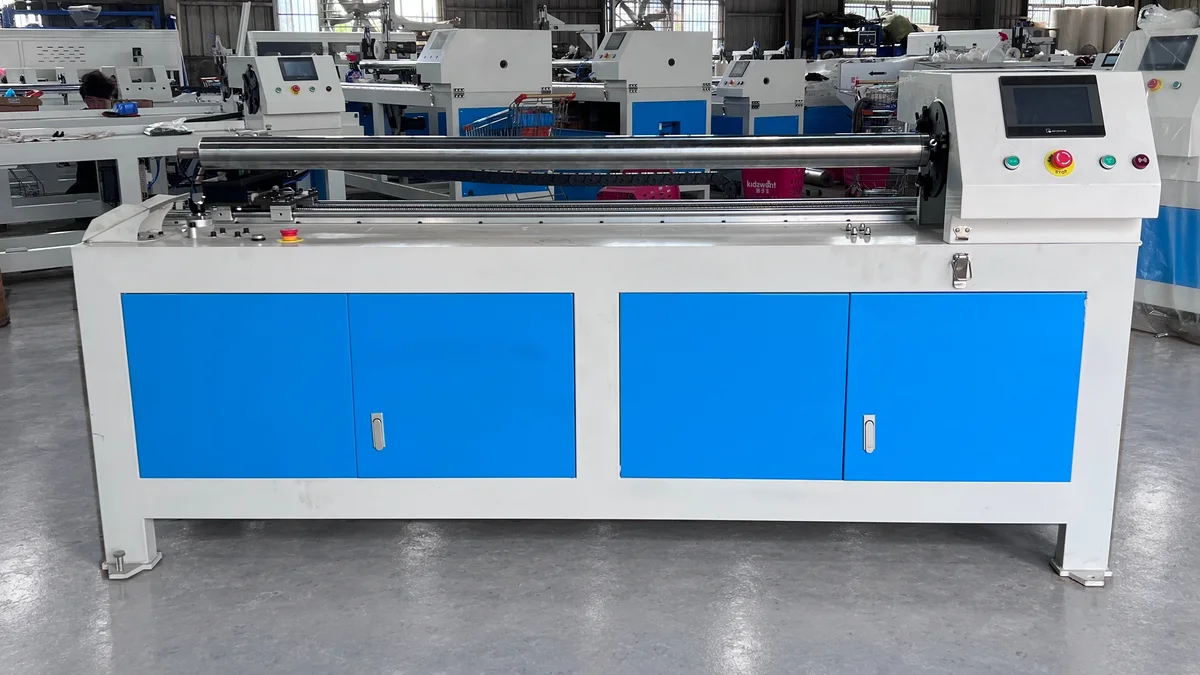
Choose roll-to-sheet cutting for bubble wrap and paper by feed pressure, unwind control, complete separation and collection, rather than textile sealing.
Read engineering guide →Start with your material and the finished part. The tube and hose, webbing and tape, and metal pipe and wire rope collections compare machines by operation and size. Paper and film use the roll-to-sheet filter. For a shortlist, send your material and its dimensions. We can also run a sample to check the cut edge and fit.
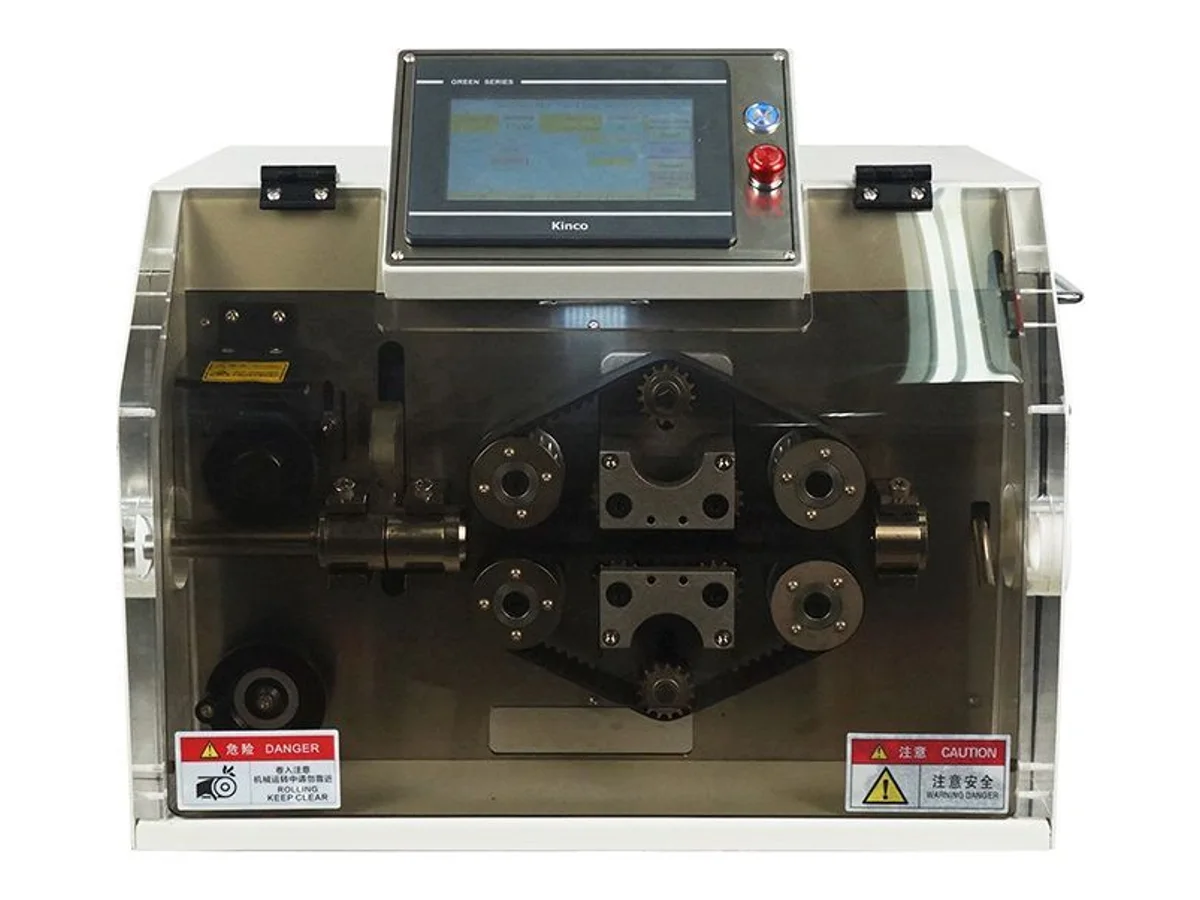
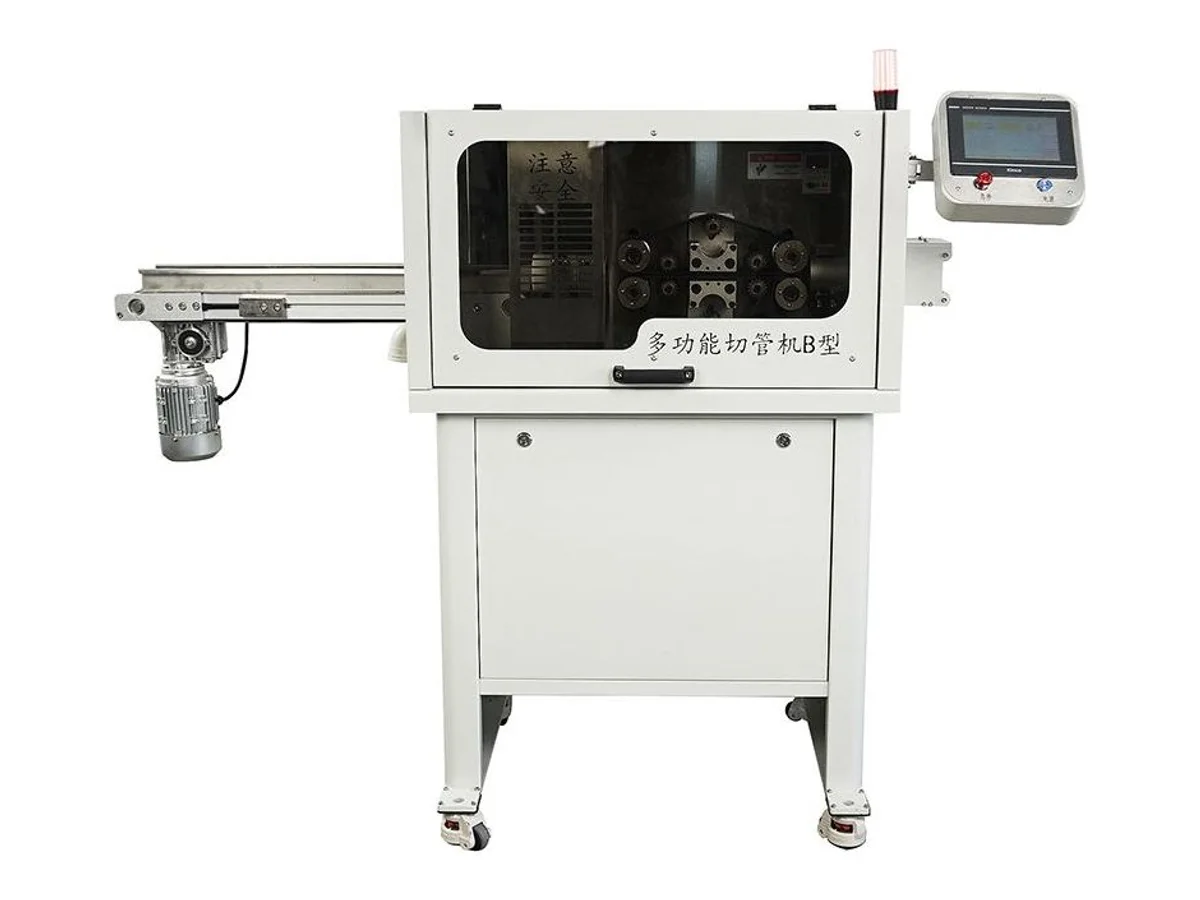
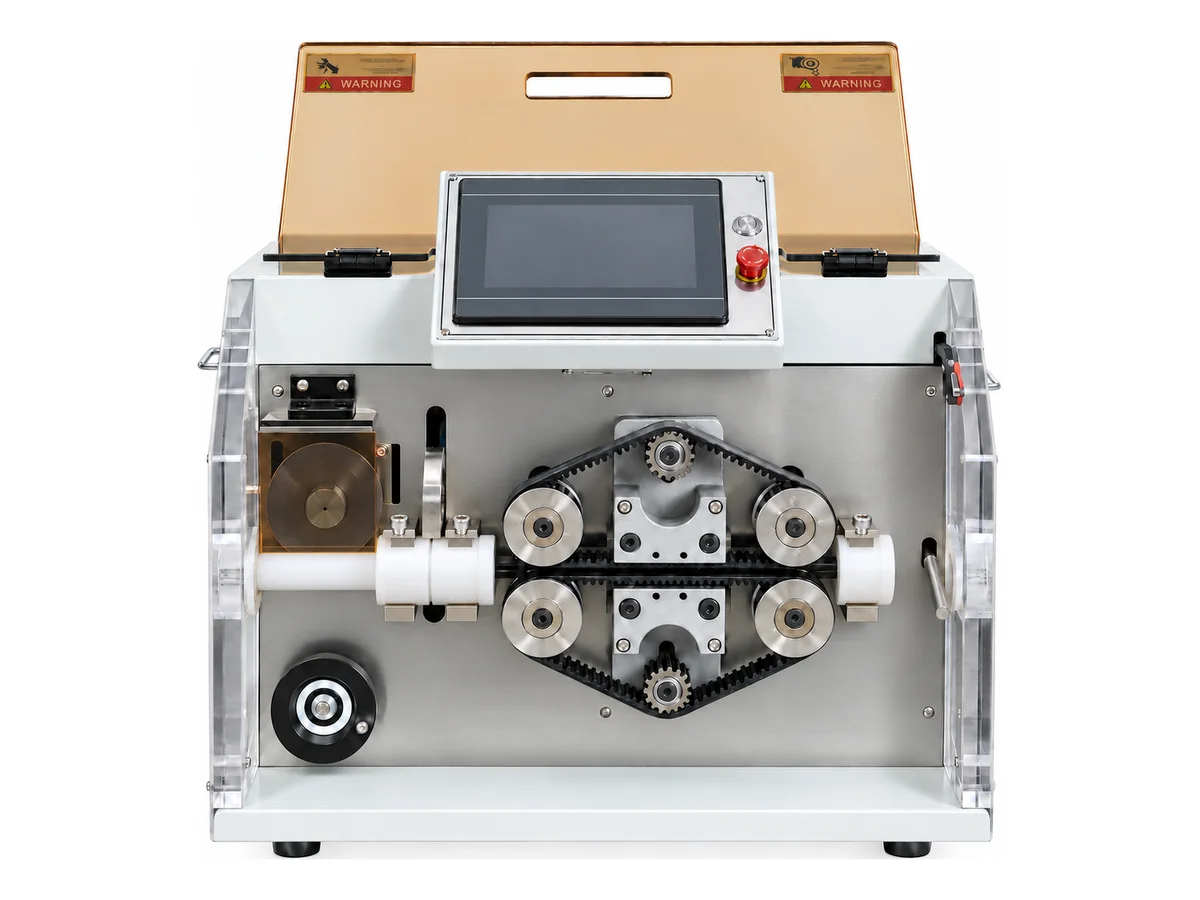
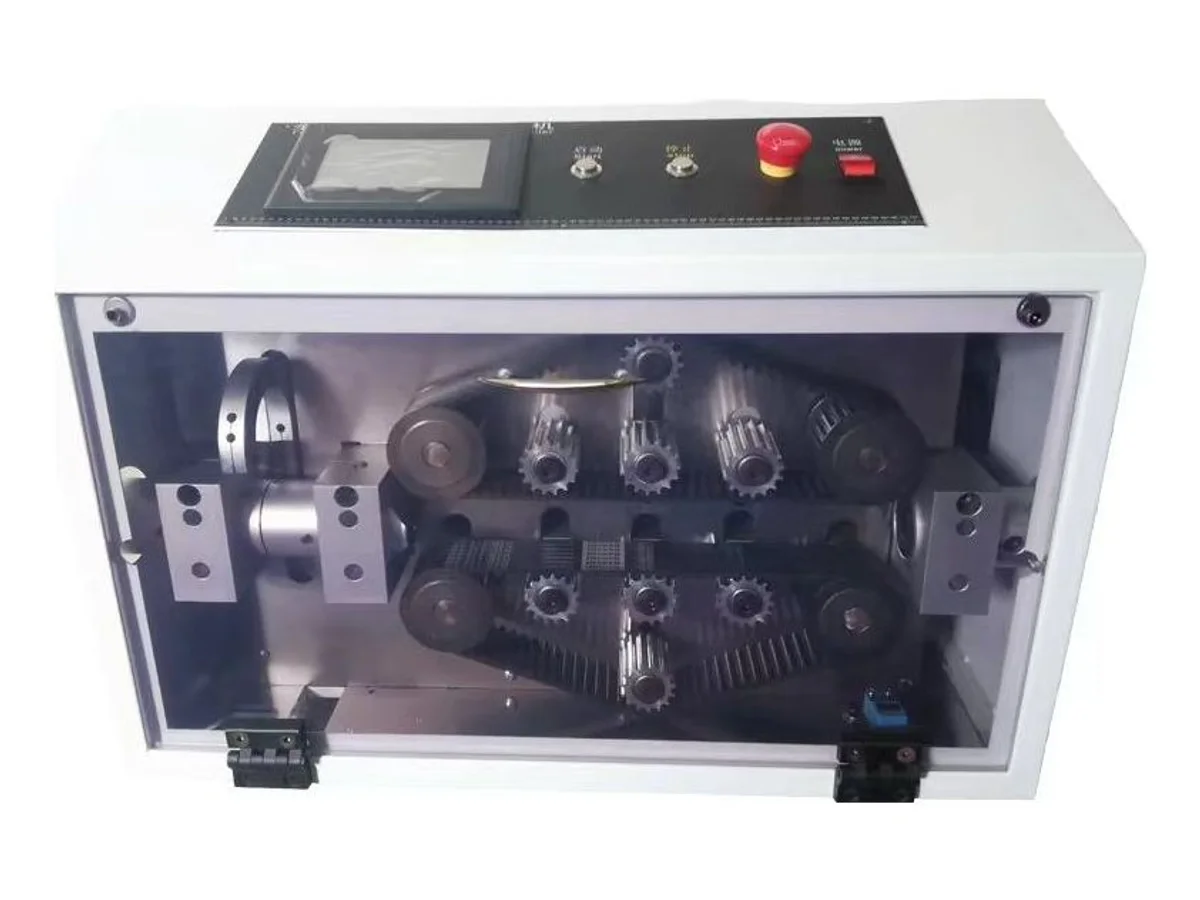
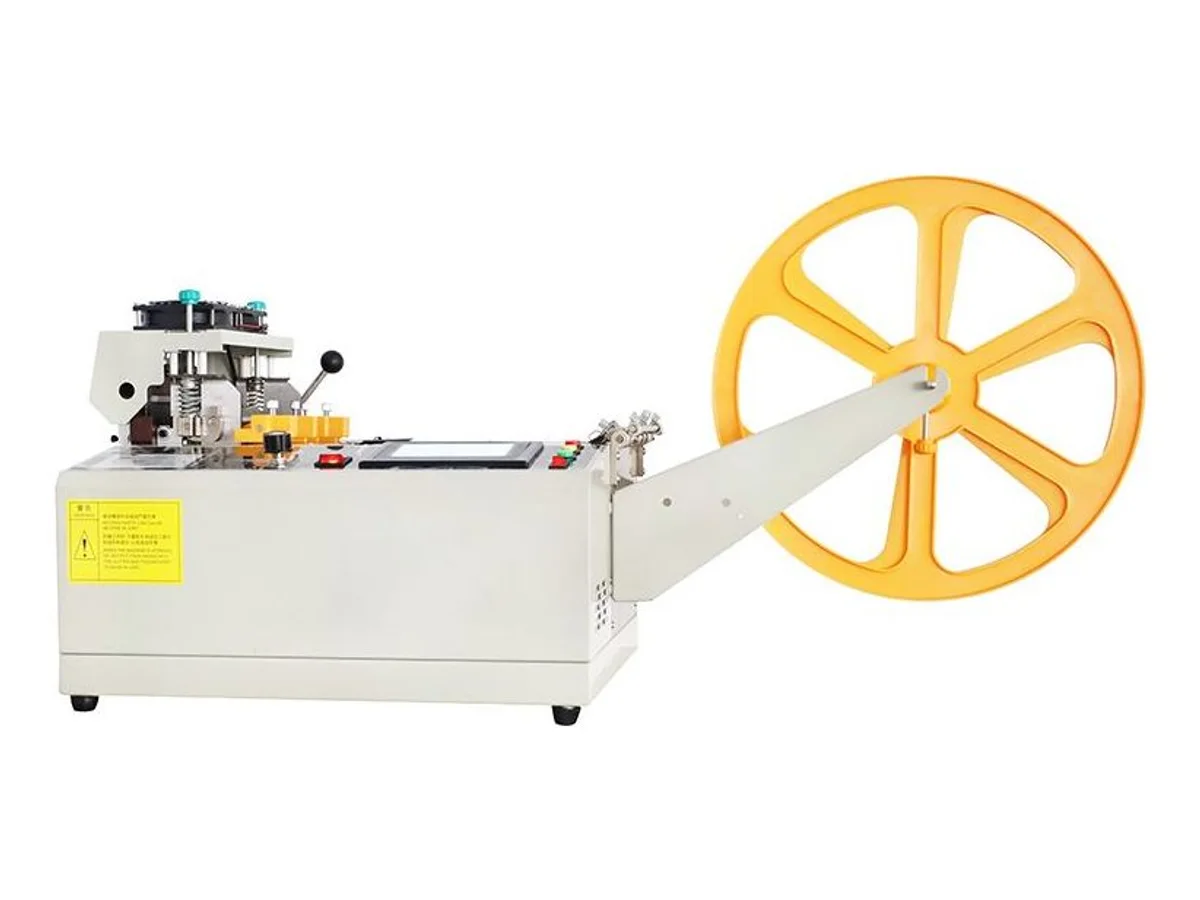
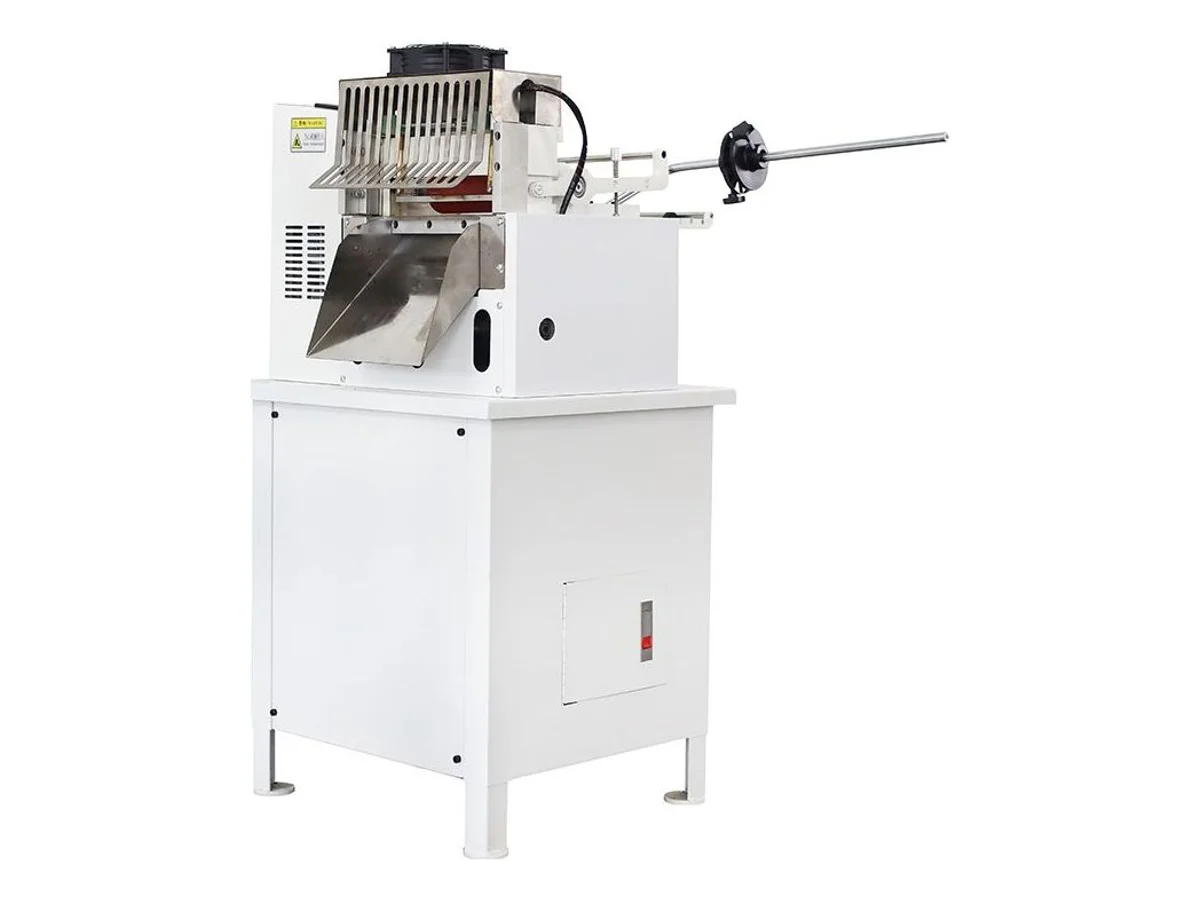
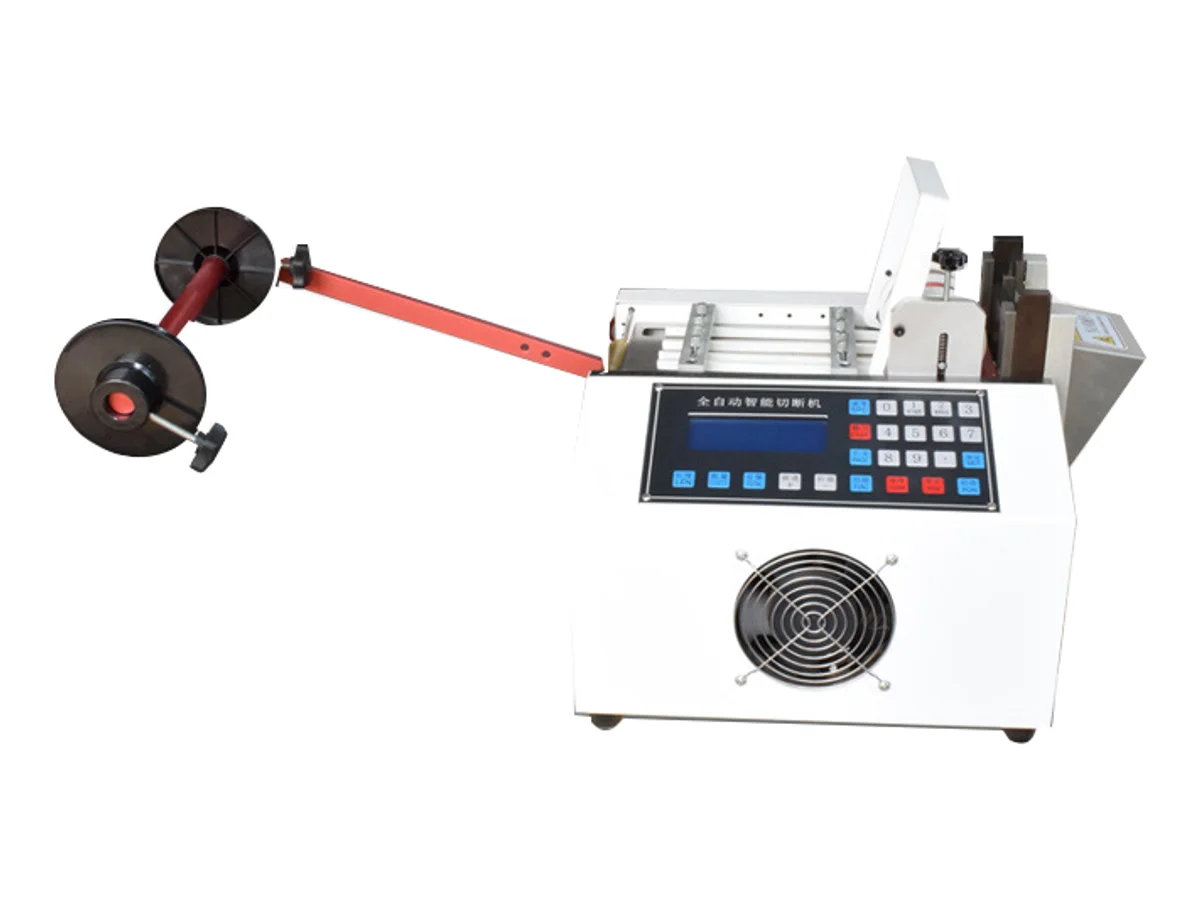
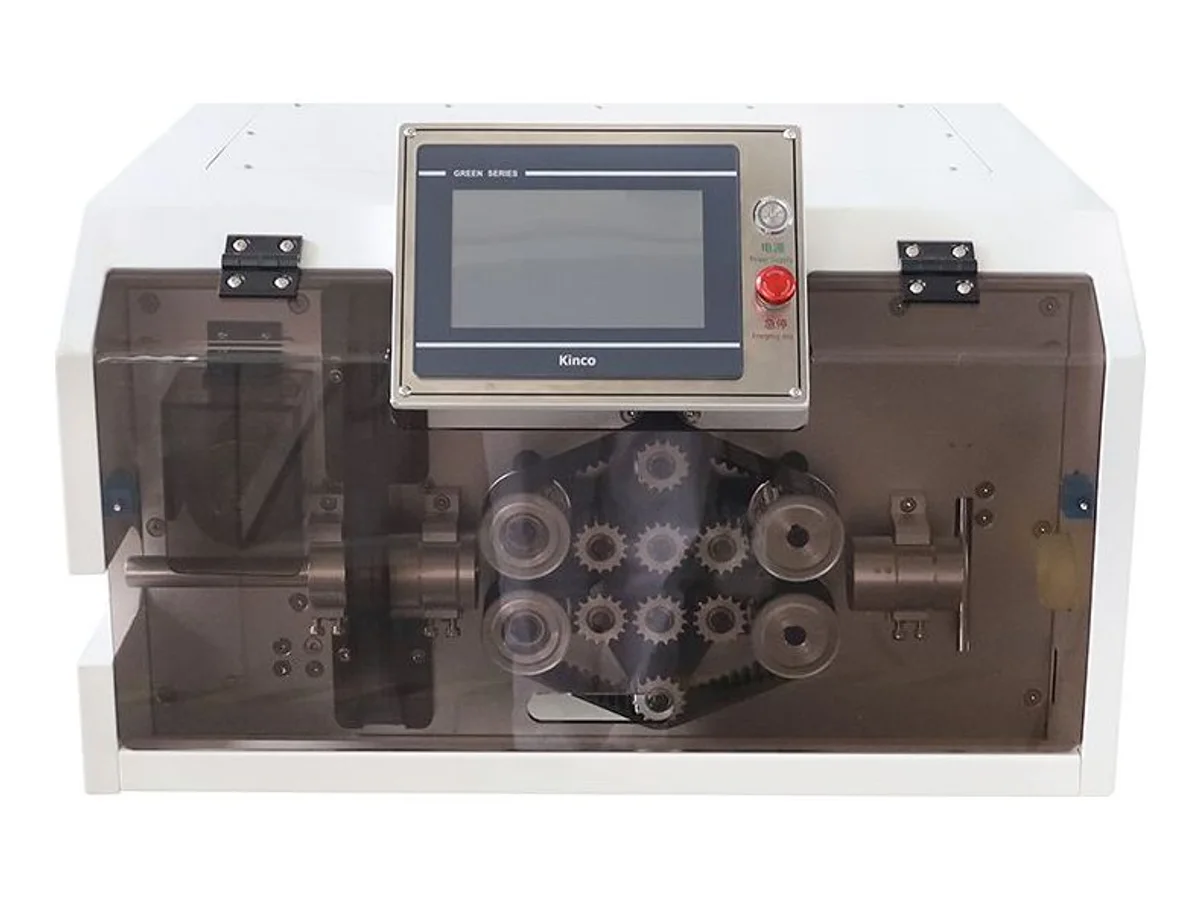
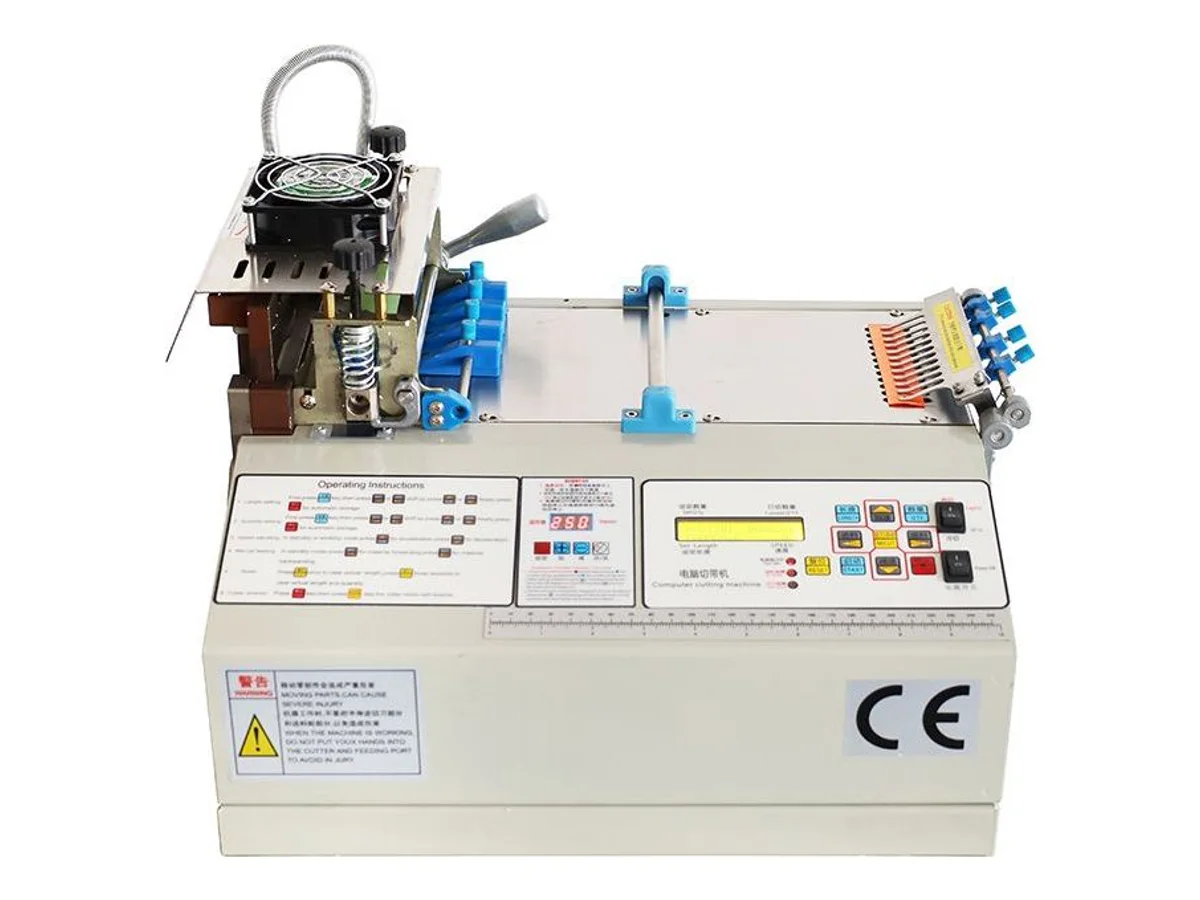
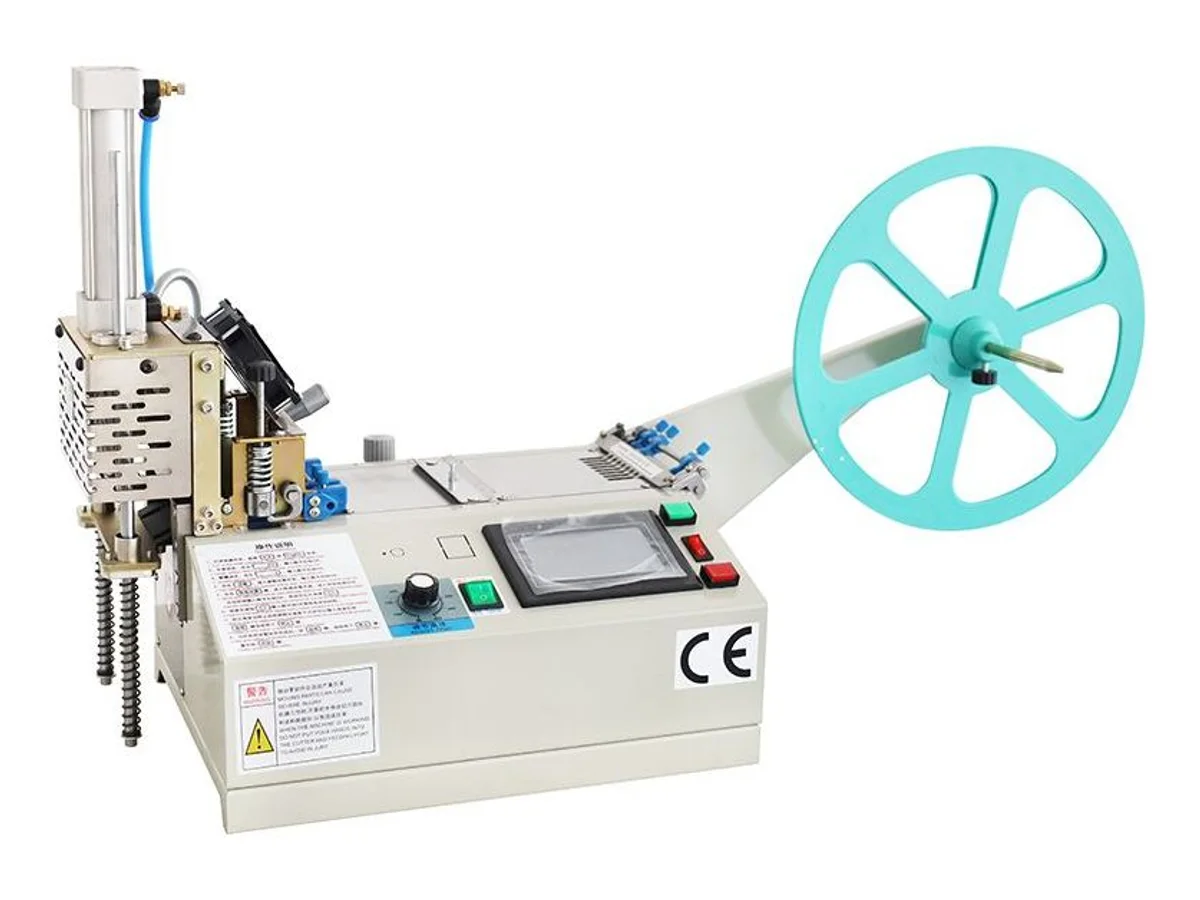
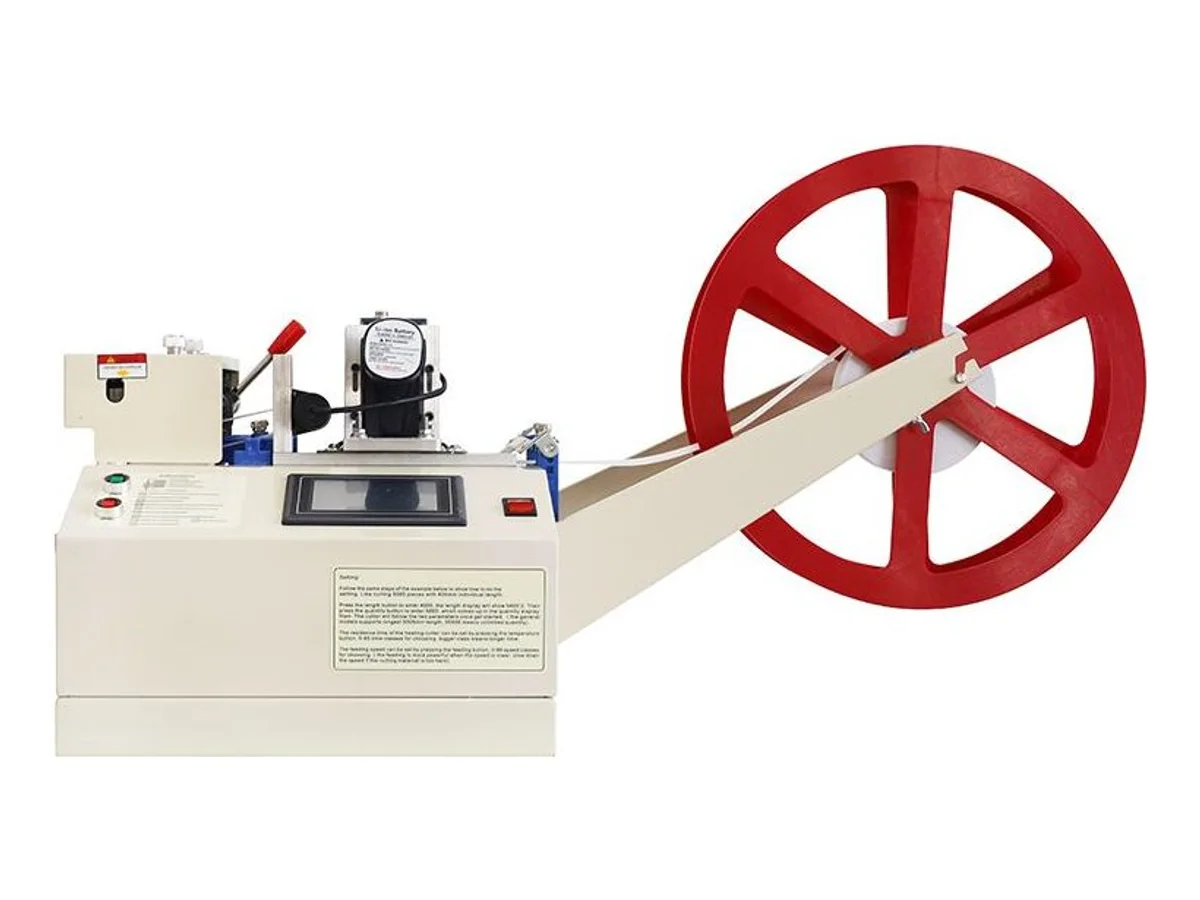
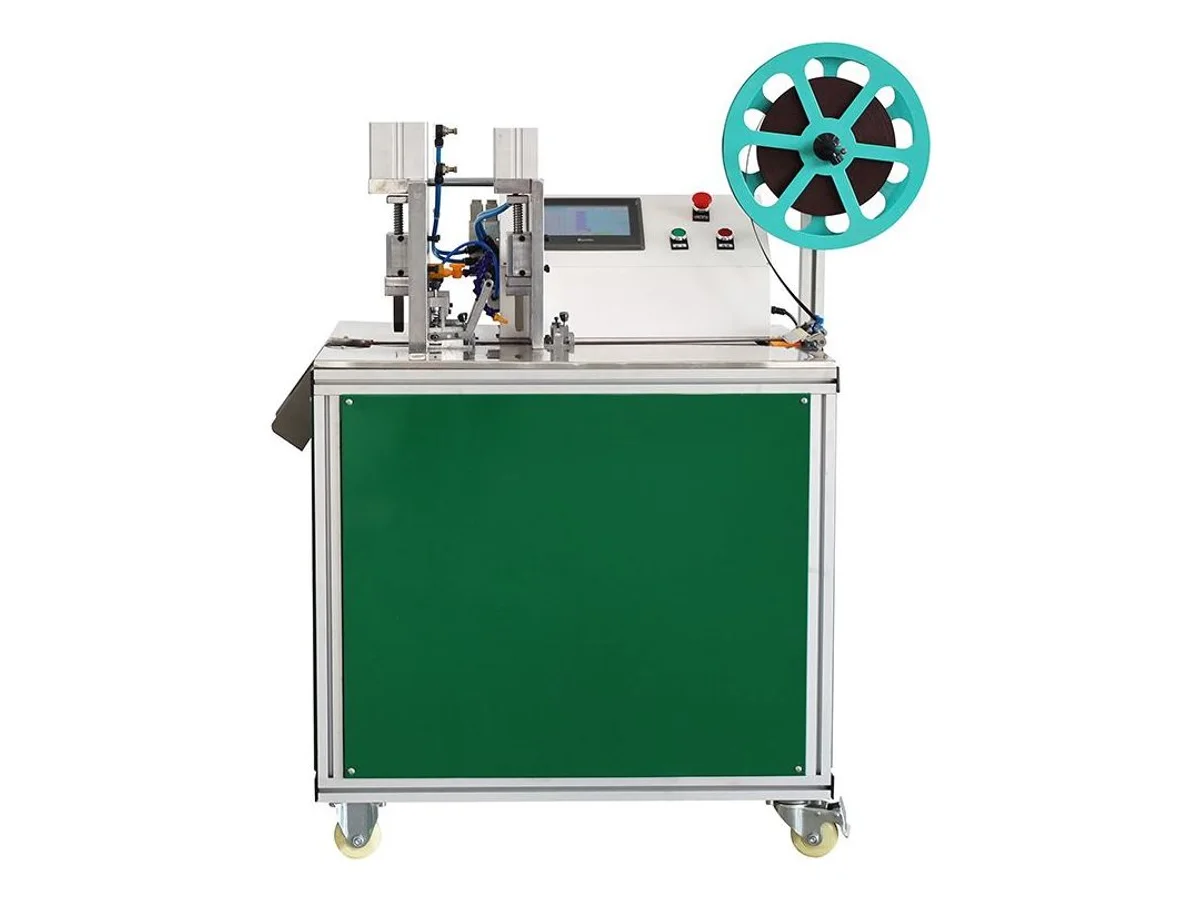
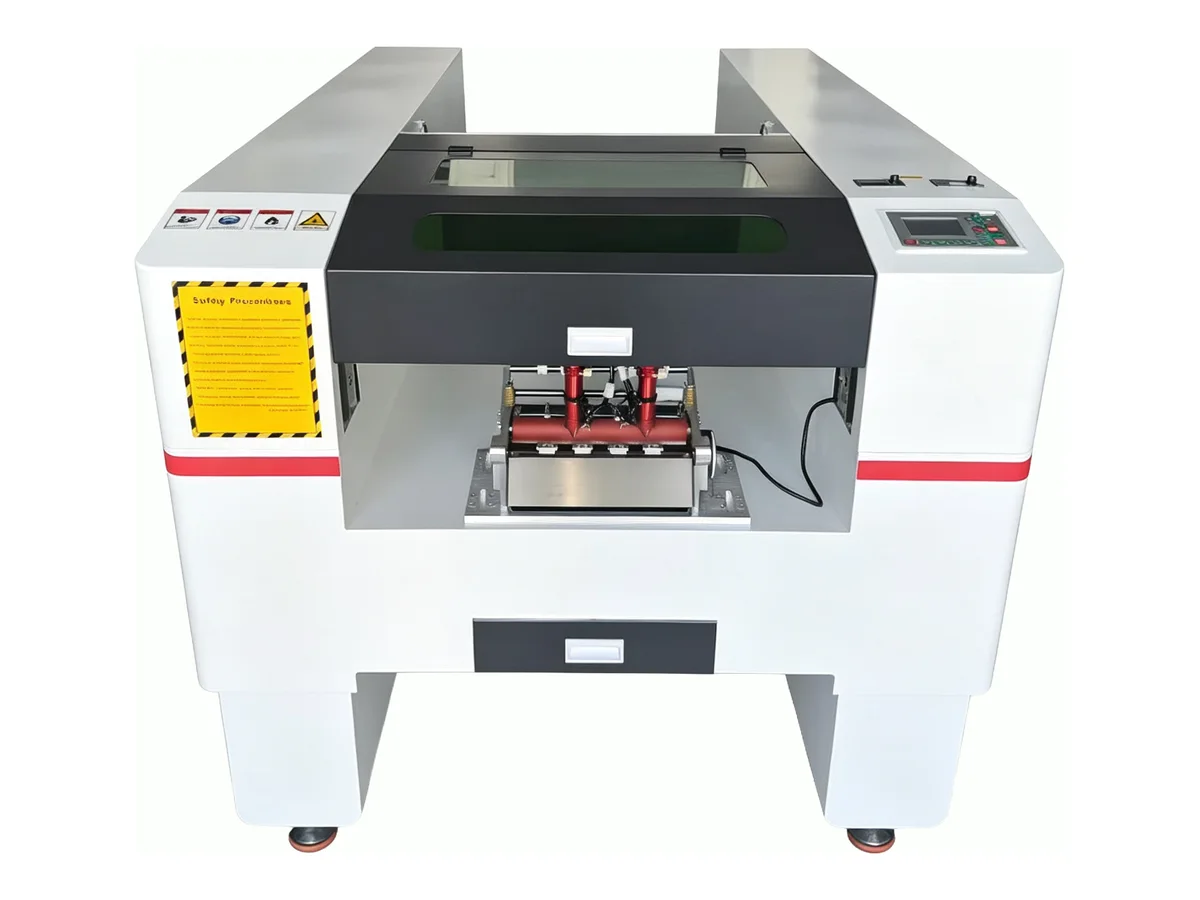
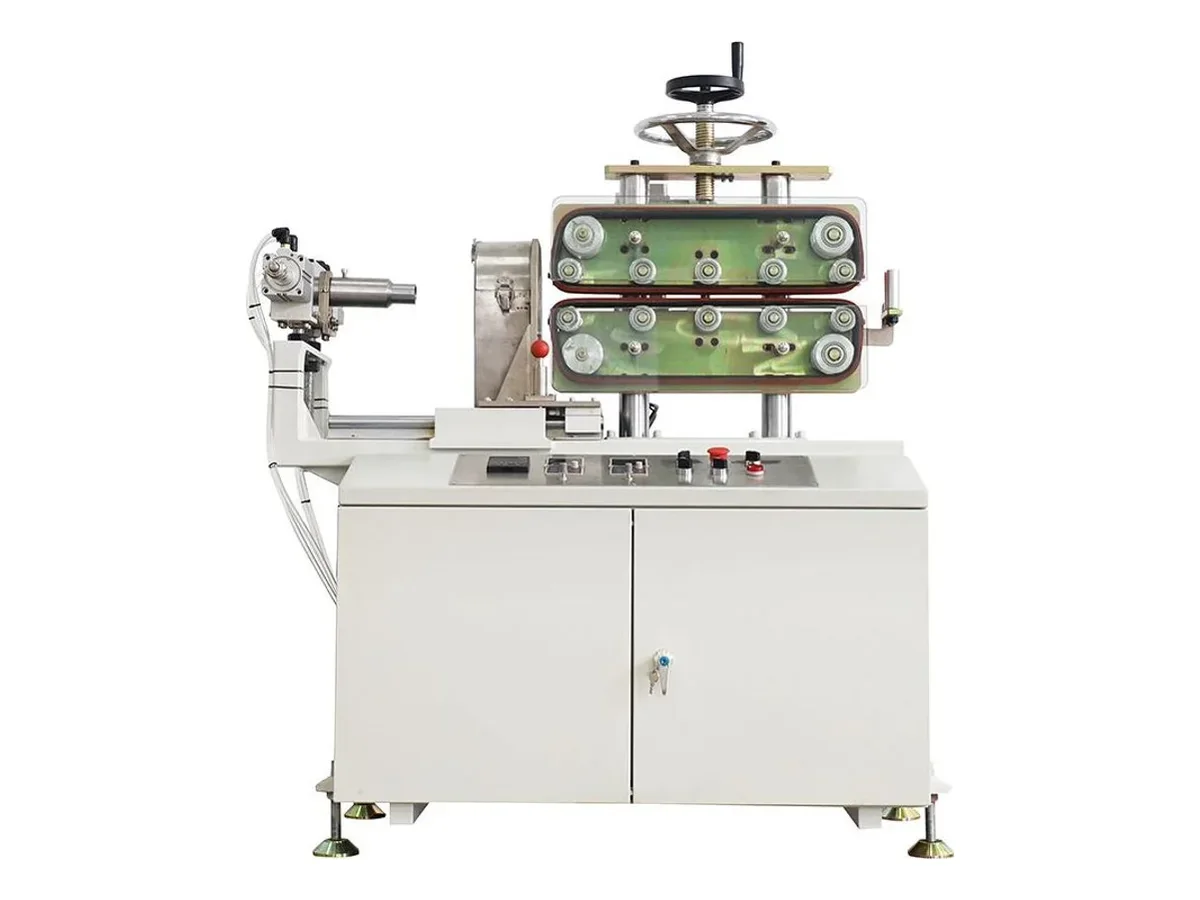
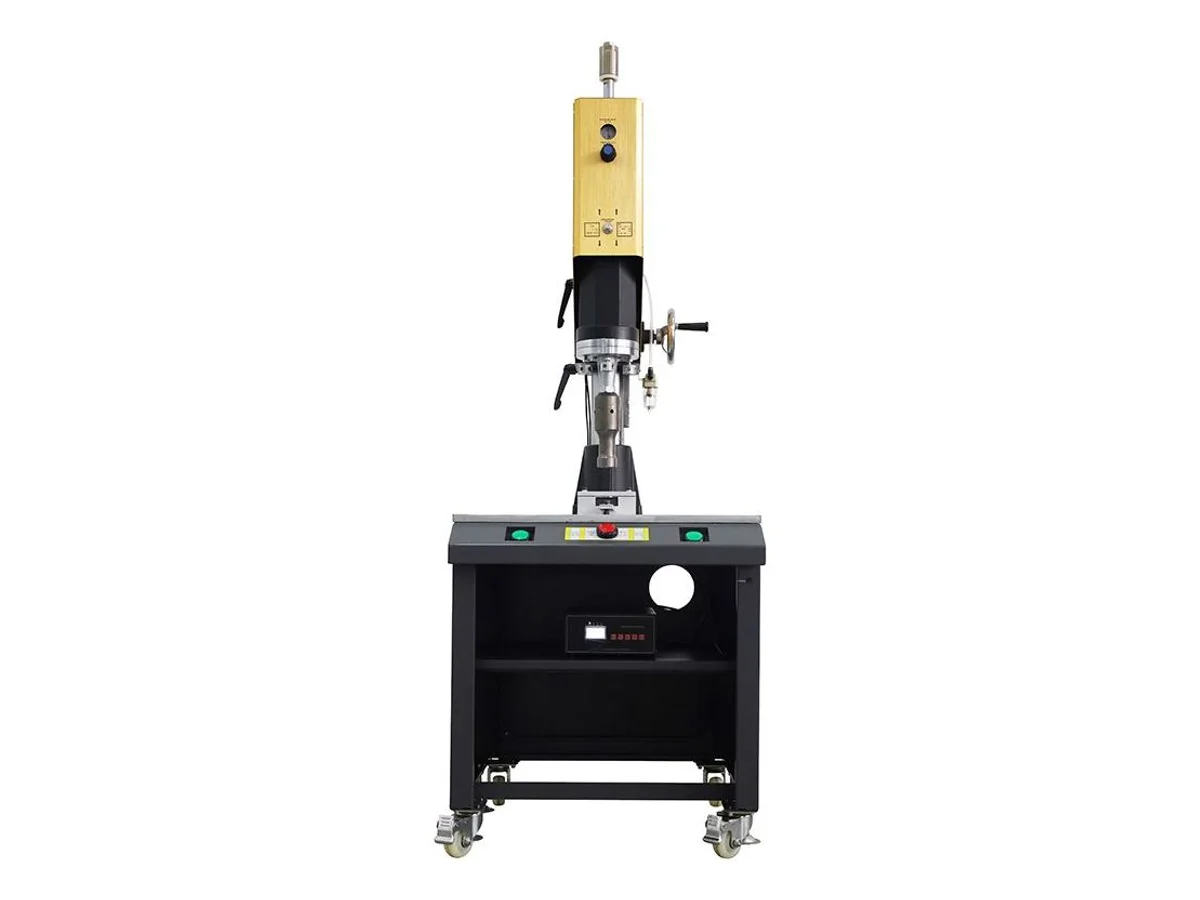
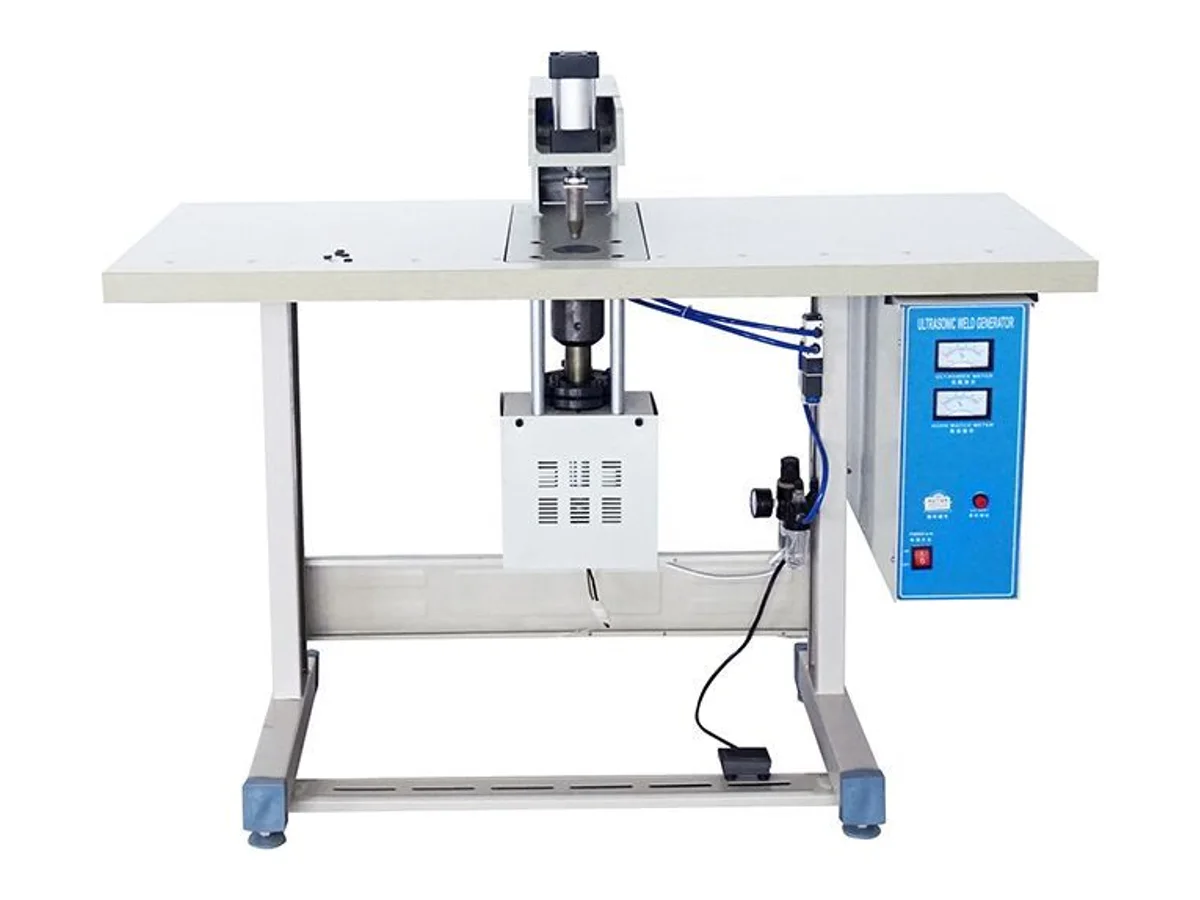
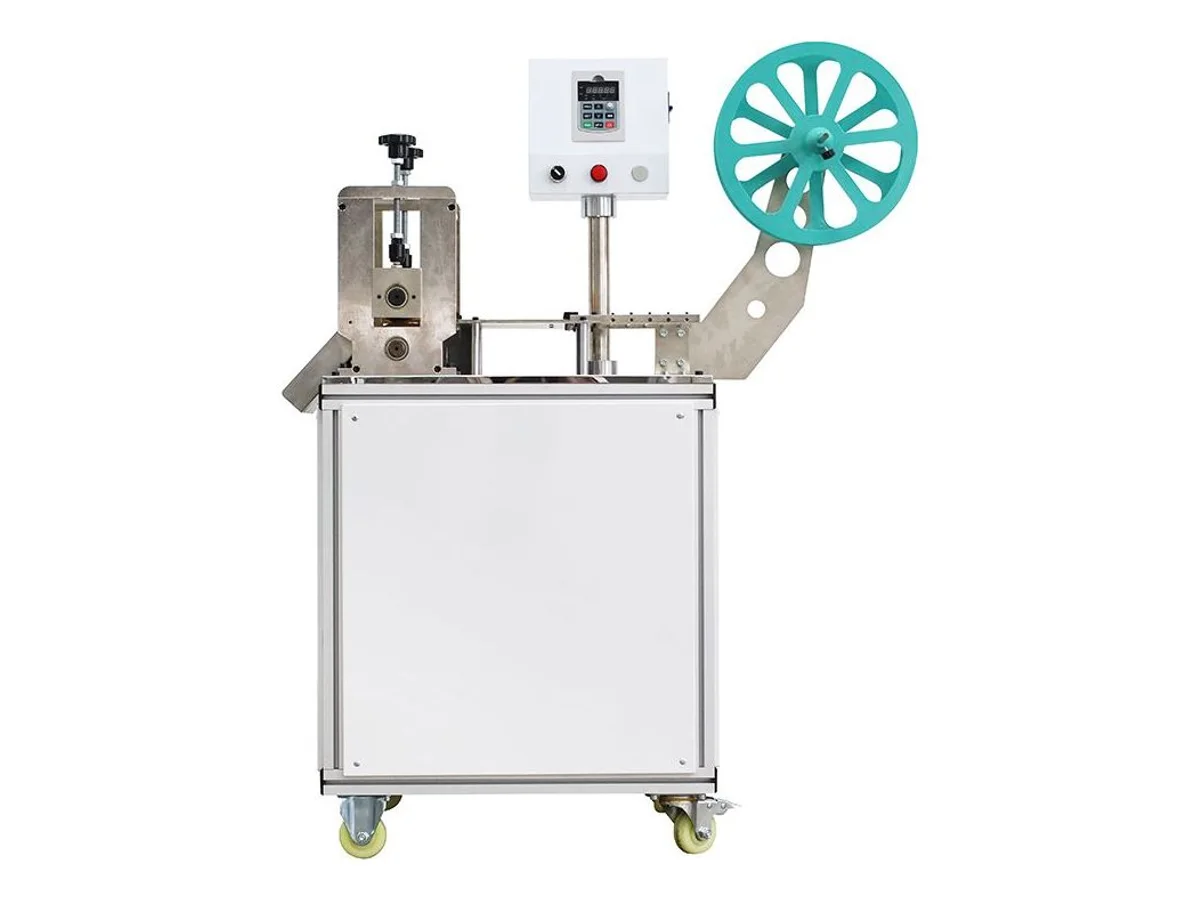
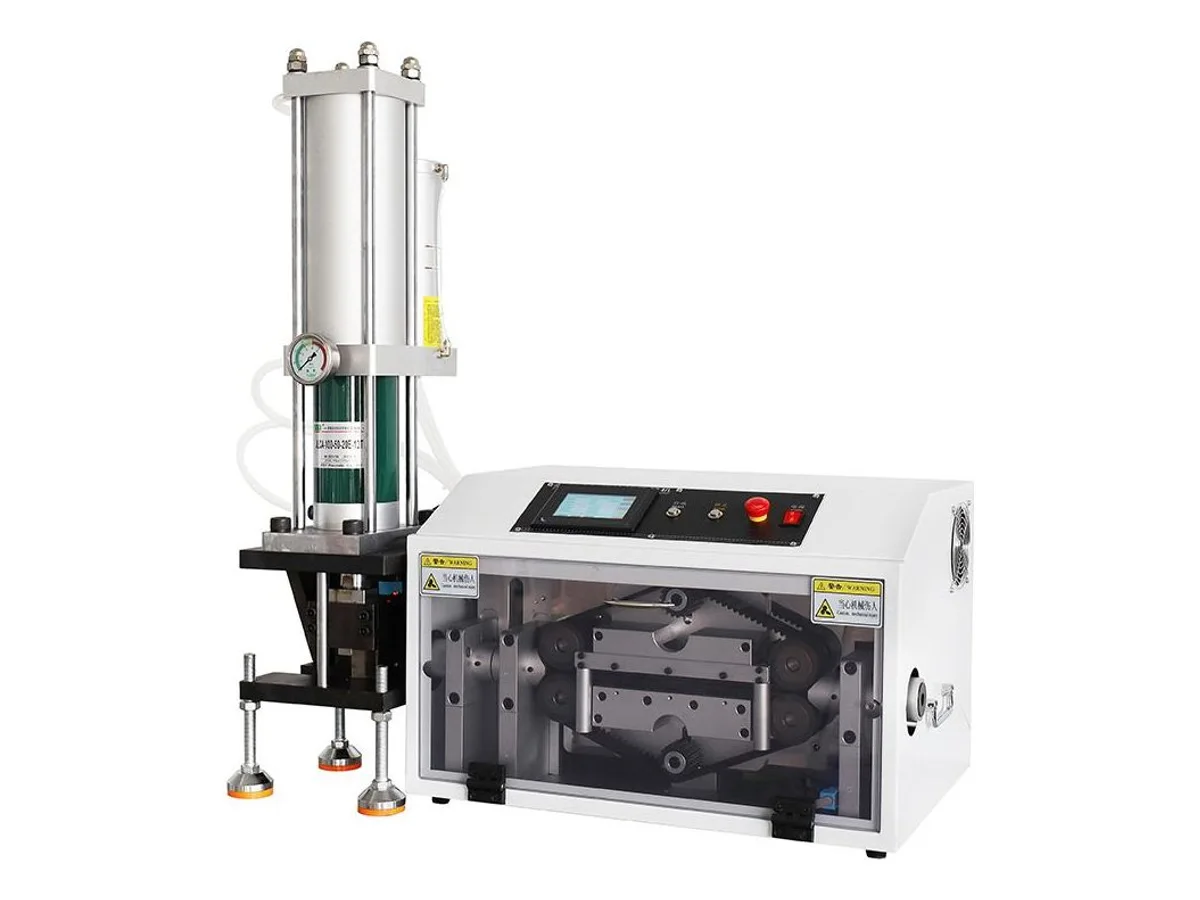
The material decides the blade. Cold blade is a starting point for corrugated loom, PVC and silicone tube; confirm squareness and deformation on the actual material. Hot knife can cut and seal compatible synthetic braid and webbing in one stroke; check blends, coatings and the cooled edge — the WM-568 does 1–100 mm widths at 7,200 cuts/hour, the WM-576 takes 200 mm widths on a floor cabinet at 6,600/hour, the WM-572A reaches 220 mm, and the WM-579 adds a stacker so pieces leave counted and piled. Ultrasonic can cut and locally seal compatible thermoplastics, including shaped work; local heat, edge quality and achievable tolerance need a sample trial: the WM-574 cuts custom shapes in rope and webbing, the WM-581 makes V-cuts, the WM-598 punches holes in zipper tape and hook-and-loop, and the WM-580 positions cuts to printed marks on satin ribbon. Rotary chipless parts metal and rigid pipe by displacement rather than removing chips; check burrs and deformation on a sample: the WM-593 covers Ø10–100 mm with 0.5–6 mm walls. Toothless saw handles armored and copper/aluminum/stainless tube of Ø1–30 mm on the WM-183, with the WM-562CNC feeding 6 m brass and aluminum bar through a 3 kW CNC head at Ø0.6–48 mm. And laser: the WM-575 punches and cuts webbing with two 10.6 µm heads, no blade to wear.
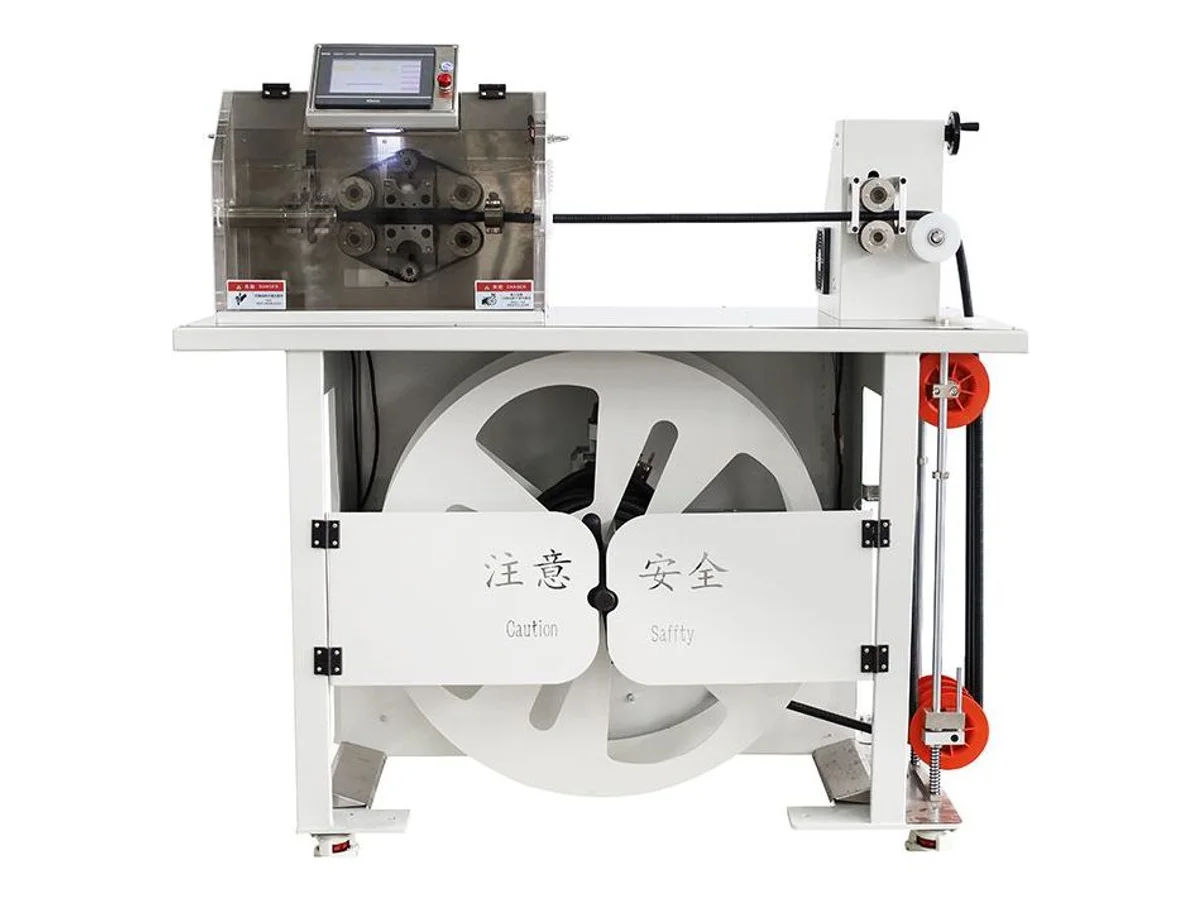
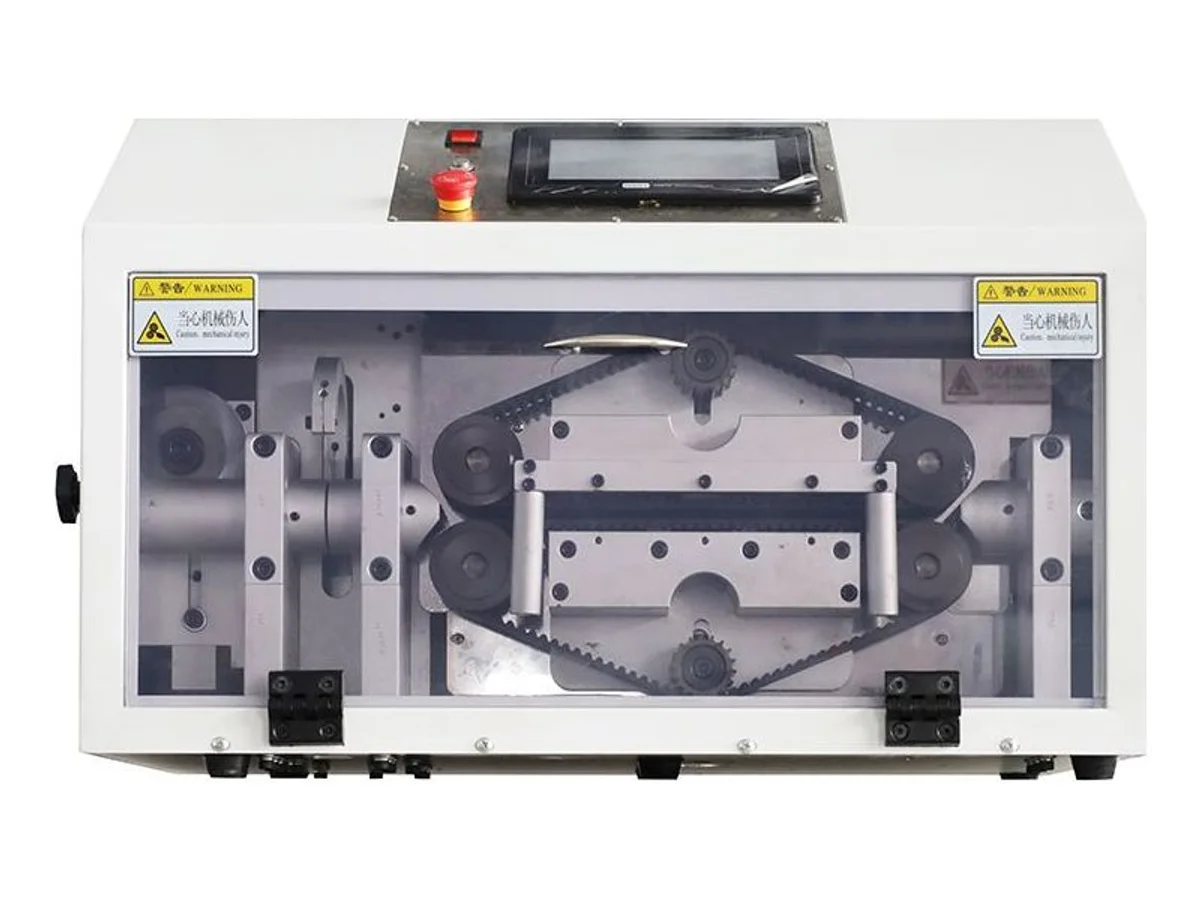
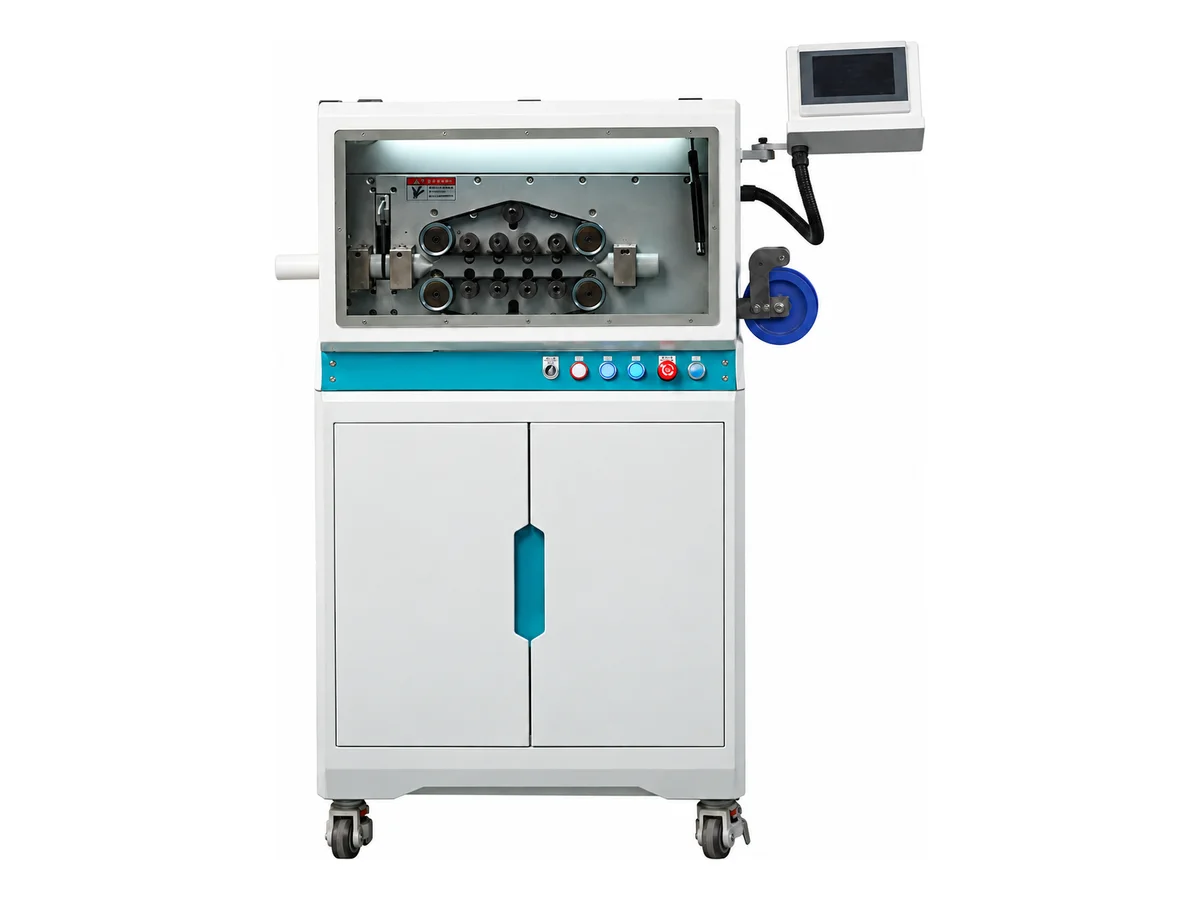
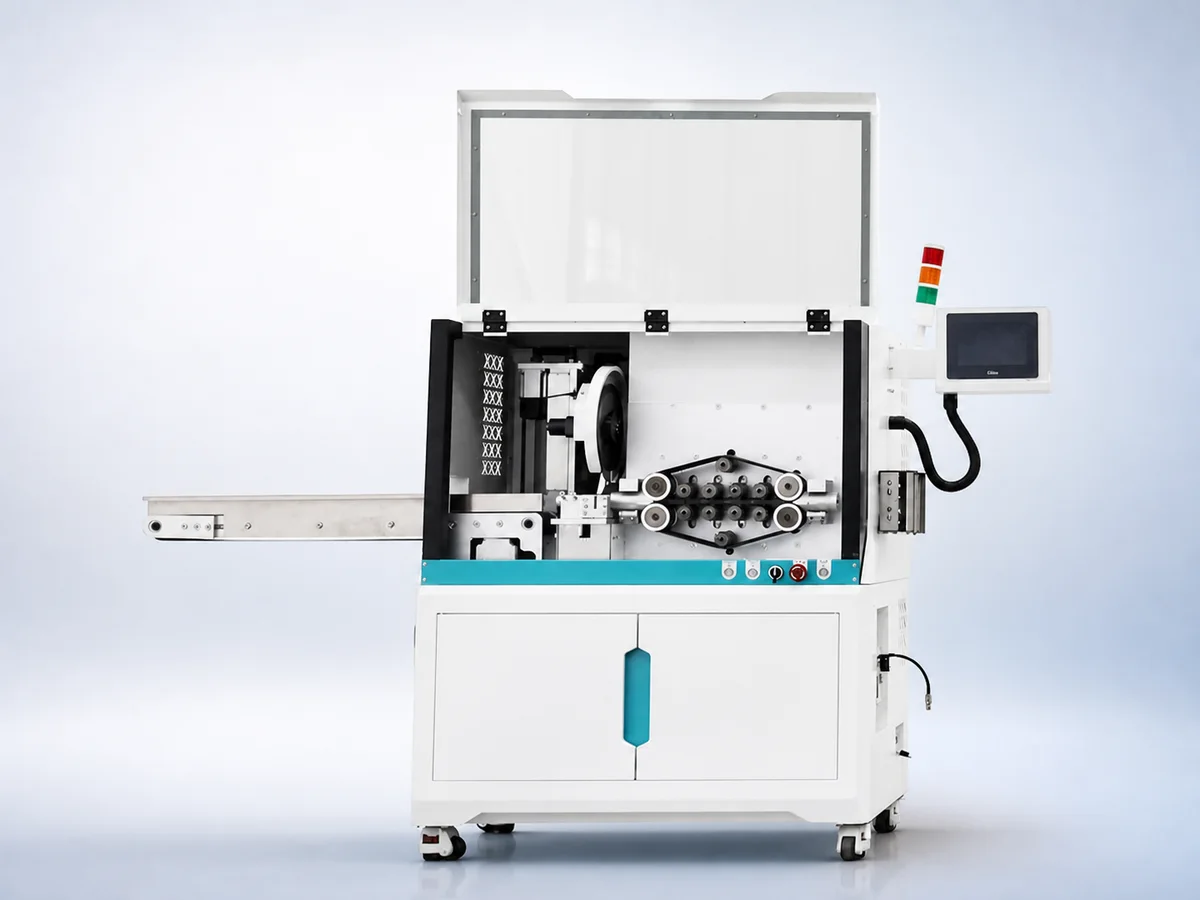
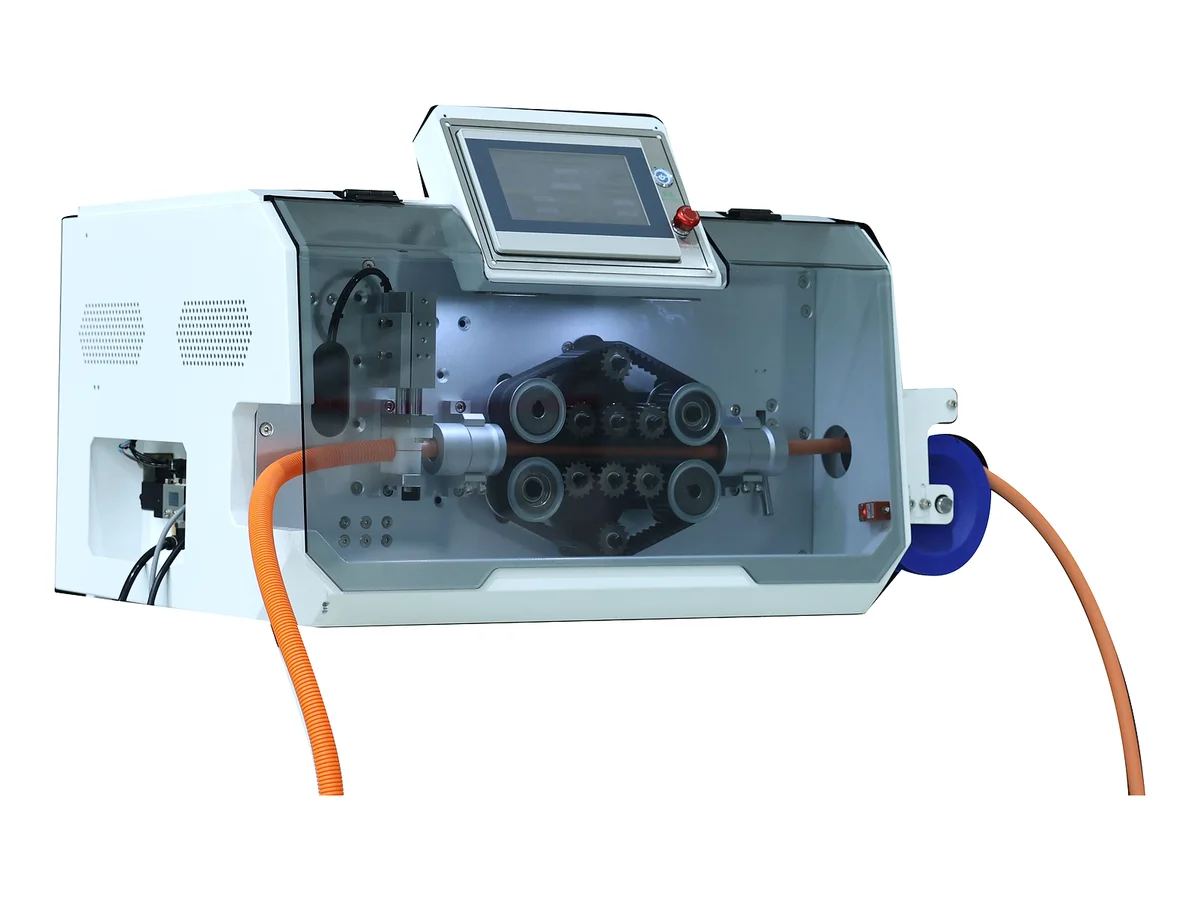
Wire loom usually needs a lengthwise slit as well as a cut, so the wire can be laid in later. The splitting knife rides inside the tube while the cutter works outside — one pass, both operations. By size and speed: the WM-176 covers Ø4–32 mm, the WM-583 extends to Ø60 mm with powered feeding at 10–60 pcs/min, the WM-584 takes mixed soft tubes to Ø38 mm, and the WM-587 is the high-speed build holding tolerance to 0.003 × L through Ø35 mm. The WM-162 integrates the pay-off reel into the cabinet for reel-fed work. For heat shrink tubing specifically, the WM-565N cuts to ±0.1 mm up to Ø38 mm and the WM-585 covers Ø1–30 mm — and once the pieces are cut, the heat shrink processing category has the machines that put them on the wire and shrink them.
| Machine | Technology | Capacity | Speed / tolerance | Pick it for |
|---|---|---|---|---|
| WM-587 | Cold blade, cut + slit | Corrugated ≤Ø35 mm | 0.003 × L tolerance | The high-speed loom line |
| WM-583 | Cold blade, cut + slit | Ø5–60 mm | 10–60 pcs/min | The biggest corrugated diameters |
| WM-176 | Cold blade, cut + slit | Ø4–32 mm | — | The standard loom machine |
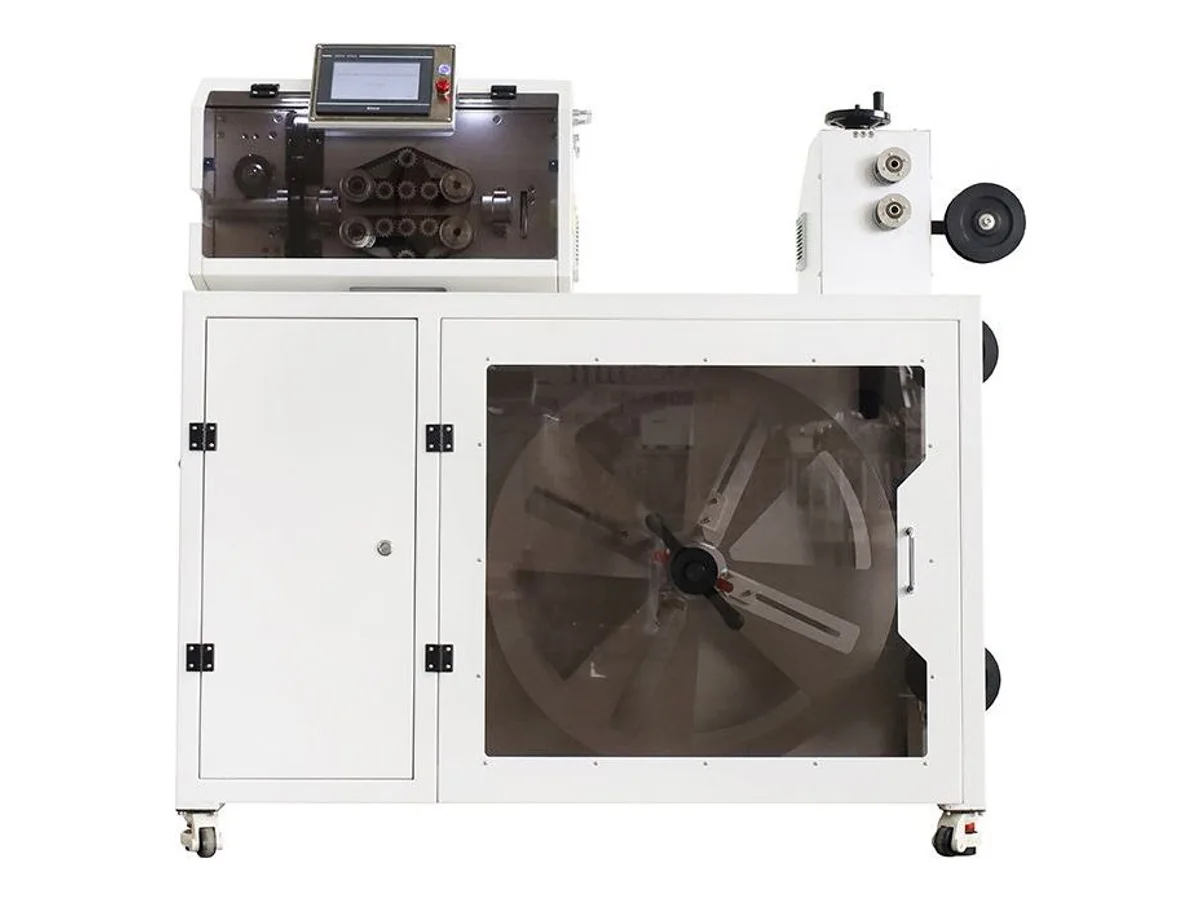
| WM-162 | Cold blade + built-in pay-off | Ø5–30 mm | 1.1 kW | Reel-fed loom, one cabinet |
| WM-582 | Rotating round knife | Hose & conduit Ø1–40 mm | Tolerance and unit confirmed on the quote | Mixed soft tube on one machine |
| WM-565N | Cold blade | Heat shrink ≤Ø38 mm | ±0.1 mm | Precision shrink tube pieces |
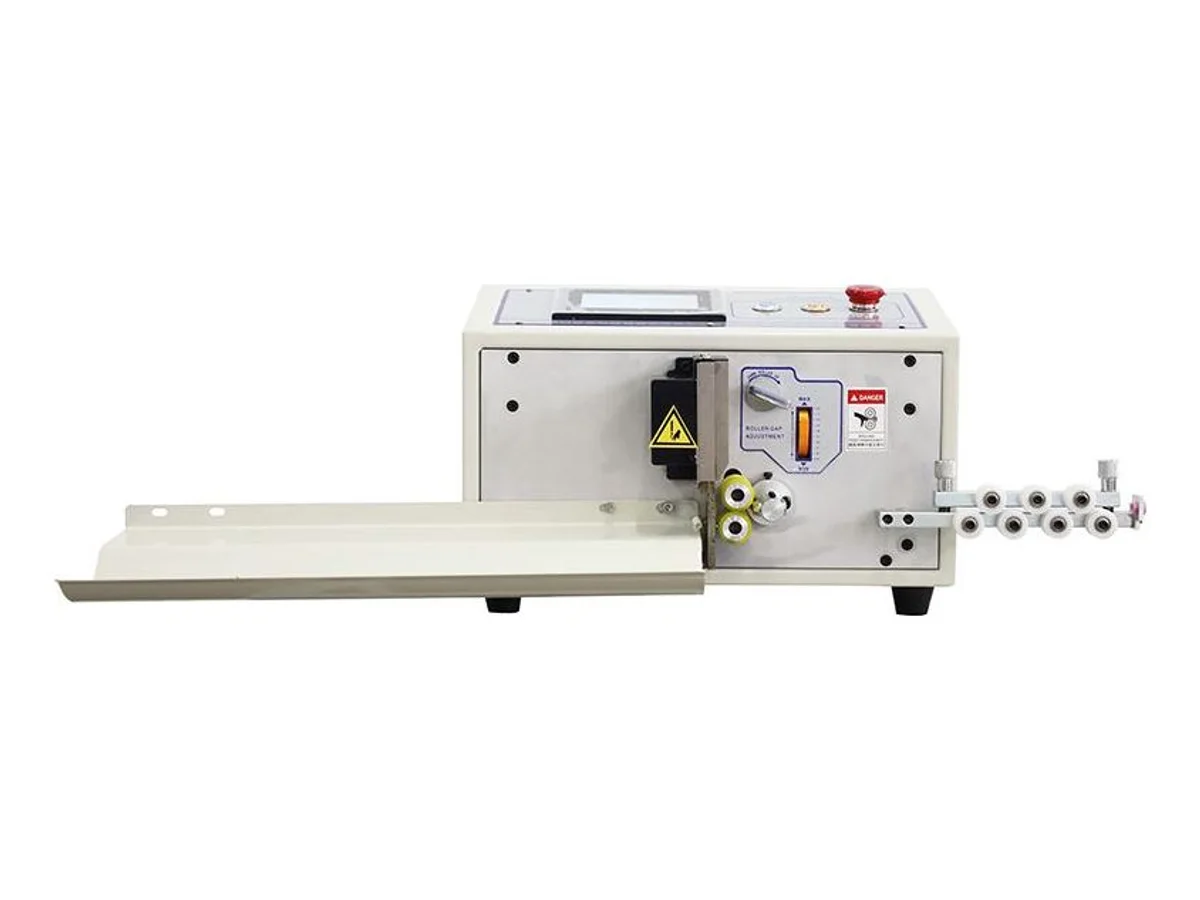
| WM-585 | Pneumatic blade | Heat shrink Ø1–30 mm | — | Shrink tube with 90 mm lay-flat |
| WM-576 | Hot knife, floor | Sleeve & webbing ≤200 mm | 6,600 cuts/h | Wide sleeve with sealed ends |
| WM-572A | Hot knife | ≤220 mm | 121 pcs/min | The widest hot cut here |
| WM-568 | Hot knife | 1–100 mm | 7,200 cuts/h | Braided sleeve at volume |
| WM-579 | Hot/cold + stacker | 1–98 mm | — | Pieces counted and stacked |
| WM-574 | Ultrasonic, shaped | Rope & webbing | — | Custom shapes with sealed edges |
| WM-598 | Ultrasonic punching | Webbing, zipper tape | 2,000 W | Punch holes; verify melt buildup on the sample |
| WM-581 | Ultrasonic V-cut | Webbing | 2,600 W | V-shaped sealed ends |
| WM-593 | Rotary chipless | Pipe Ø10–100 mm, wall 0.5–6 mm | — | Metal tube without saw chips; check burrs |
| WM-183 | Toothless saw | Metal tube Ø1–30 mm | — | Armored and copper/stainless pipe |
| WM-562CNC | CNC saw | Brass/alu Ø0.6–48 mm, 6 m stock | 3.0 kW | Bar stock, programmed lengths |
| WM-591 | Rotary knife, precision | Rigid pipe processing range 1–50 mm | 0.05 mm at 100 mm | The tightest tolerance in the category |
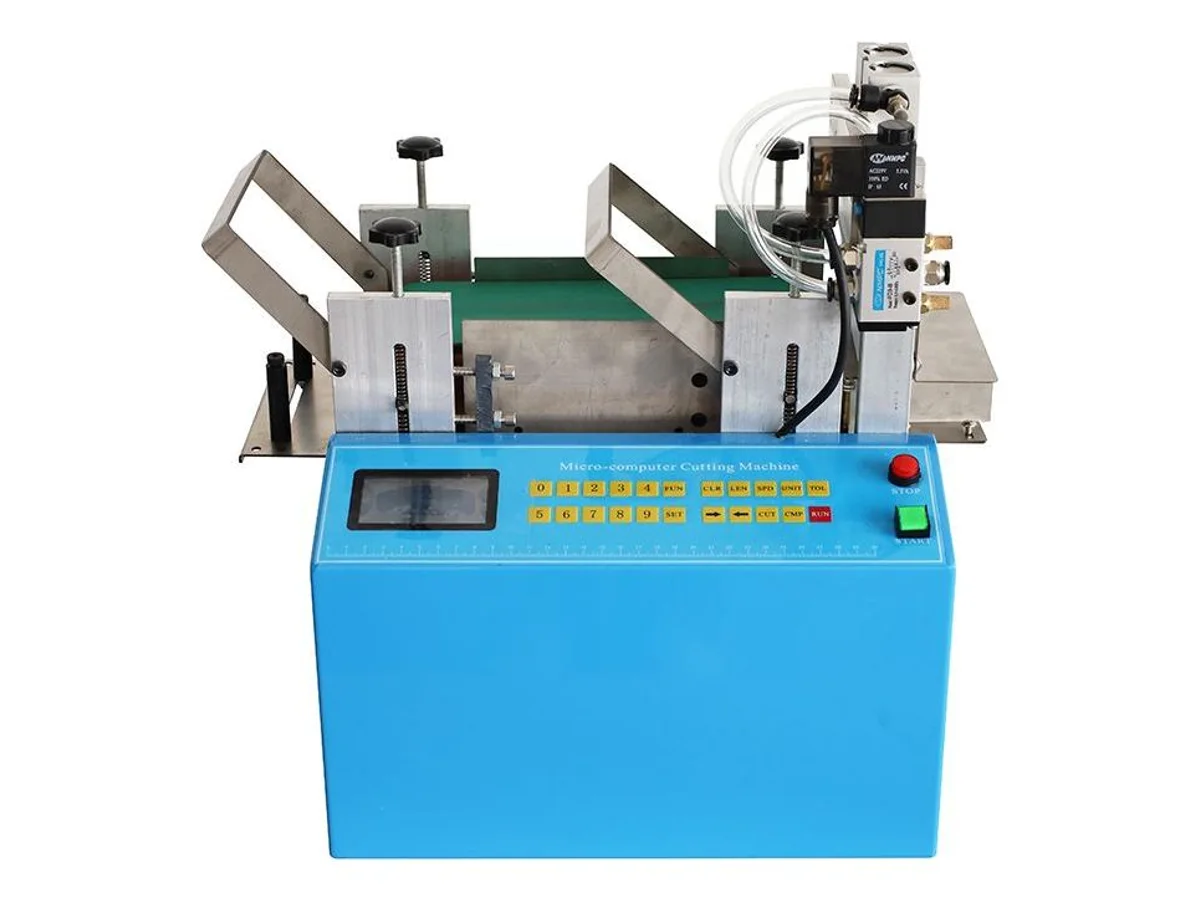
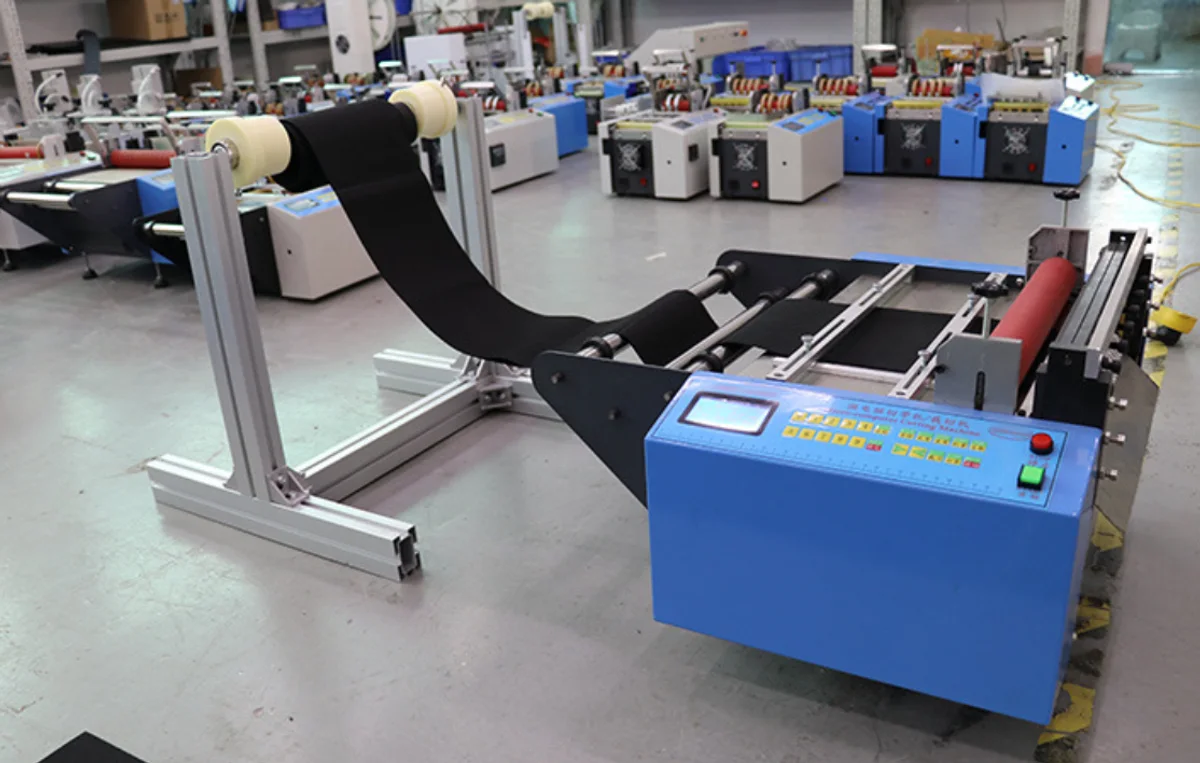
| WM-575S | Roll-to-sheet | Film & sheet ≤1,220 mm wide | 0.1 mm | Cutting roll goods into sheets |
Compare the outside diameter, wall thickness and finished cut length. For corrugated tubing, identify the cut position on the corrugation and whether the tube needs a longitudinal slit. For soft tubing, we can check the finished length and cut edge on your sample.
Choose by the material and the required finished edge. A cold blade separates tube, hose or tape without deliberately melting it; check squareness, deformation and fraying on your sample. A hot knife can cut and seal compatible synthetic braid or webbing, but coatings and blends can change the edge. Ultrasonic cutting can seal suitable thermoplastic fibers and support shaped cuts, V-cuts, holes or print registration in the relevant machine configuration. It creates local heat and does not inherently provide a tighter tolerance or a better edge than a hot knife. Cotton and other pure natural fibers do not fuse by these methods. Agree the acceptable edge and measure trial pieces before selection.
A rotary chipless cutter parts the tube by displacing material, not removing it — avoiding saw chips inside the tube; check the cut edge for burrs and deformation on your sample. The WM-593 does this on Ø10–100 mm pipe with 0.5–6 mm walls. When the tube is armored or the section is small, a toothless-saw machine like the WM-183 (Ø1–30 mm) is the alternative; for programmed cutting of 6 m brass or aluminum bar, the WM-562CNC.
Yes — that is the standard build in this category. A splitting knife rides inside the tube while the cut-off works outside, so every piece leaves cut to length and slit lengthwise, ready for wire to be laid in. The WM-176 (Ø4–32), WM-583 (Ø5–60), WM-584 (≤Ø38) and high-speed WM-587 (≤Ø35, 0.003 × L) all cut and split in one pass.
The WM-565N cuts shrink tube up to Ø38 mm at ±0.1 mm; the WM-585 covers Ø1–30 mm with pneumatic cut-off. Cutting is only half the job — inserting the pieces onto wire and shrinking them is its own machine family, in the heat shrink processing category, including lines that cut, insert and shrink in one pass.
The material (and whether it is synthetic — that decides hot versus cold cutting), diameter or lay-flat width, cut length and tolerance, whether corrugated tube needs splitting, and target pieces per hour. Then courier 2–3 meters of the actual material: edge quality is a material property as much as a machine property, so we cut yours on video before you order.
Engineering guidance for choosing this process and correcting the defects that affect finished-wire quality.
Selection guide
Choose roll-to-sheet cutting for bubble wrap and paper by feed pressure, unwind control, complete separation and collection, rather than textile sealing.
Read engineering guide →Selection guide
Separate programmed tube length from usable short-ring capacity. Check support, wall deformation, blade clearance, release and collection on actual material.
Read engineering guide →Troubleshooting guide
A U.S. customer sent 1/8-inch 316 stainless wire rope for a 152.4 mm cut trial. See the cut ends and the checks needed for ferrule fit and length.
Read engineering guide →Troubleshooting guide
A U.S. customer's 60 mm-ID silicone hose left stepped ends with a straight cut. We changed to shaft-supported circumferential cutting on WM-613.
Read engineering guide →Selection guide
Use the bore, outside diameter, wall and finished width to compare paper core cutters. Check the cut edge and run the core on your winding shaft.
Read engineering guide →Selection guide
Choose the machine for the missing step in split loom assembly. Compare conduit cutting and lengthwise slitting with fitting the loom to a terminated harness.
Read engineering guide →Selection guide
Specify the long edge, short edge and cut direction on a strap drawing. Compare two angle cutters and check the cooled strap in its buckle.
Read engineering guide →Selection guide
Set heat shrink tubing cut length from required coverage, material length change and measured samples. Separate cutter accuracy from recovery behavior.
Read engineering guide →Selection guide
Choose corrugated-conduit cut position by the fitting, rib profile and finished length. Compare length feeding with camera positioning and verify assembly fit.
Read engineering guide →Selection guide
Specify PTFE tube cutting by wall thickness, end squareness, bore condition and cleanliness. Build a sample trial before choosing an automatic cutter.
Read engineering guide →Troubleshooting guide
Prepare pneumatic tubing for push-in fittings by checking square cuts, sealing surfaces, insertion depth and routing length. Specify an automatic-cutting trial.
Read engineering guide →Selection guide
Compare full-cut and half-cut wire marker sleeves by picking sequence, separation, print orientation and assembly checks before choosing a marking line.
Read engineering guide →Selection guide
Set relaxed-length acceptance for elastic webbing: control reel tension, compare repeat cuts, and verify recovery before changing feed compensation.
Read engineering guide →Selection guide
Choose a rope-cutting process by fiber and construction. Check nylon, polyester, aramid and HMPE separately, including core retreat and the cooled end.
Read engineering guide →Selection guide
Check printed ribbon cutting by finished length and print-to-cut offset. Trial mark contrast, glossy material, splices, missing marks and restarts.
Read engineering guide →Selection guide
Specify coated steel rope cutting by metal diameter, coating, strand containment and actual sleeve fit. Keep cutting acceptance separate from termination strength.
Read engineering guide →Selection guide
Choose steel wire rope cutting equipment by rope construction, end restraint, tooling and measured cut quality—not diameter alone.
Read engineering guide →Troubleshooting guide
Control soft-hose cut length by checking relaxation, reel drag, feeding and measurement. Assess open bore and cut quality alongside length.
Read engineering guide →Selection guide
Compare cold, hot-knife and ultrasonic cutting for webbing and tape by fiber composition, edge finish, stretch, width and cut shape.
Read engineering guide →Selection guide
A 5 mm silicone-tube inquiry shows why a rotating blade does not prove spiral-cut capability. Define the helix, support and sample acceptance.
Read engineering guide →Selection guide
Choose tube and pipe cutting equipment by material, diameter, wall thickness, rigidity, cut mechanism, tolerance, end quality and chip-control requirements.
Read engineering guide →Troubleshooting guide
Troubleshoot angled cuts, crushed tube, burrs, stringing, length drift, corrugated-tube splitting errors and feed slippage.
Read engineering guide →