Benchtop Wire Stripping and Insulated Ferrule Crimping Machine WM-3246
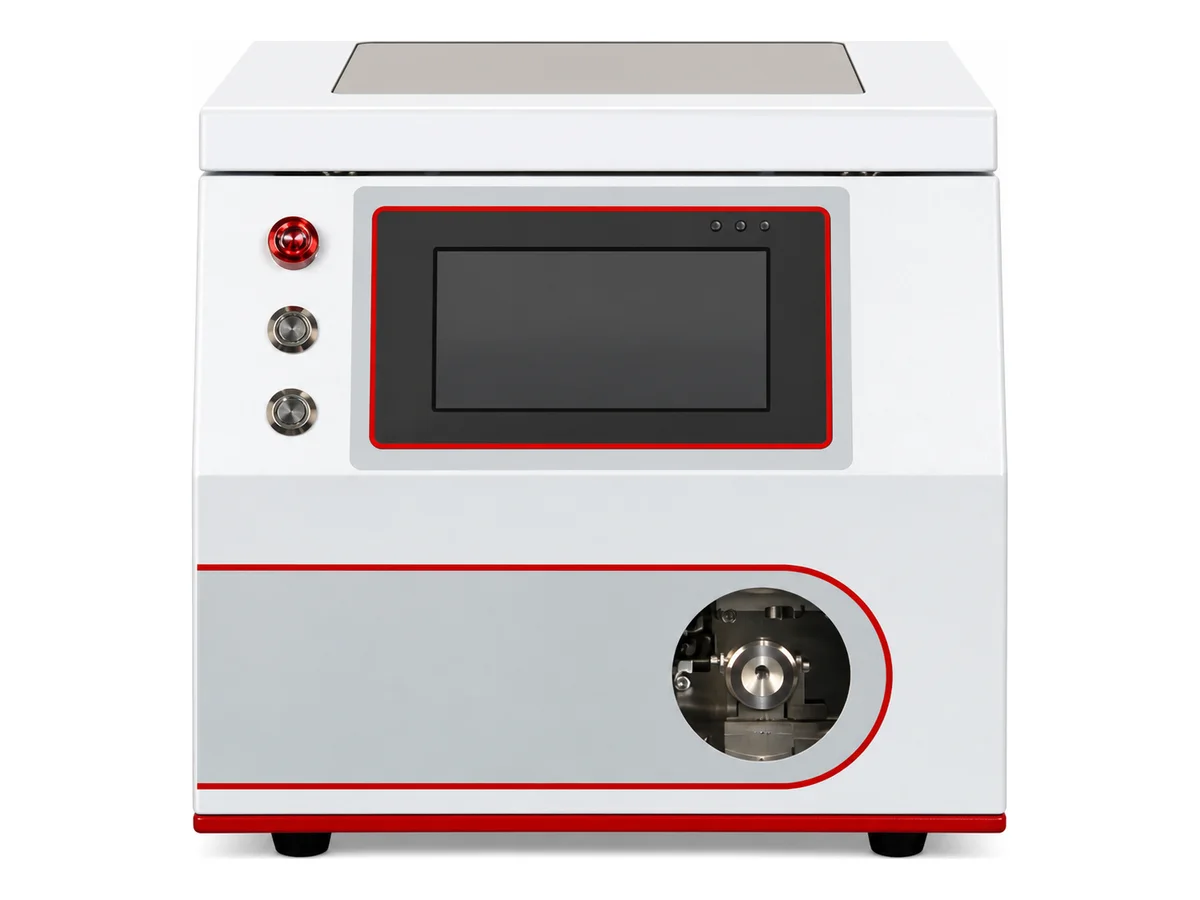
We supply the WM-3246 as an operator-loaded wire stripping and insulated ferrule crimping station for prepared cable ends. It combines vibratory ferrule feeding, touchscreen setup and a square crimp in a 350 × 450 × 400 mm benchtop enclosure. The datasheet lists BVR wire sizes from 0.5 to 4 mm² and a 2.5-second machine cycle; tooling and other range configurations are confirmed on the quote.
Specifications
| Process | Wire-end stripping and insulated tubular ferrule crimping, with operator loading |
|---|---|
| Wire sizes — datasheet | BVR wire: 0.5, 0.75, 1.0, 1.5, 2.5 and 4.0 mm² |
| Range — configuration table | 0.3–4 mm² tubular-terminal configuration; optional enlargement to 16 mm². Confirm the selected range and tooling before ordering. |
| Crimp profile | Four-sided square crimp |
| Ferrule dimensions | Pre-insulated tubular ferrule with round insulating collar, collar length ≤7.5 mm |
| Machine cycle | 2.5 s per wire, stated as one machine operating cycle |
| Control | Touchscreen HMI, electronic and pneumatic control |
| Operating modes | Automatic triggering and manual operation |
| Changeover | Manual replacement of relevant fixtures, vibratory bowl adjustment and electronically stored settings |
| Detection | Ferrule presence and right-side safety door opening |
| Stroke — tubular-terminal configuration | 30 mm (configuration table) |
| Crimp force — tubular-terminal configuration | 2000 N (configuration table) |
| Ambient temperature | 10–20 °C |
| Ambient humidity | 30–80% RH, non-condensing |
| Electrical supply | AC 220 V, 50/60 Hz, 10 A; internal DC 24 V and DC 12 V |
| Compressed air | 0.6–0.8 MPa, stable, clean and dry; inlet pressure must remain ≥0.6 MPa |
| Dimensions | W350 × L450 × H400 mm, excluding protruding parts |
| Machine weight | Approximately 40 kg |
| Packed weight | 55 kg (packing information); packing dimensions confirmed on the quote |
| HS Code | 8463.90 (common reference — final classification confirmed by your customs broker) |
| Certification | CE (certificate provided with shipment) |
Key features
- Bring ferrule feeding, stripping and crimping to one benchtop station so the operator can present each prepared cable end without moving between separate hand tools.
- Use a square crimp and tooling matched to your ferrule to prepare a termination that can be checked against the intended terminal block. We inspect strand capture, conductor exposure and finished fit during sample setup.
- Recall stored settings for repeat work; change the relevant fixtures and adjust the vibratory bowl when the wire or ferrule changes. This gives the operator a defined setup to check before starting a batch.
- Ferrule-presence and right-side door detection help identify missing material and access to the working area during operation.
- Send your wire, ferrules and terminal-block details. We fit the tooling and send you a video of the stripping and crimping result before you order.
What it processes
- Control-panel wiring with insulated bootlace ferrules on prepared wire ends
- Multicore cable tail preparation after the outer jacket has been removed
- Electrical equipment assembly with repeat ferrule sizes and operator-paced loading
A ferrule should contain the strands and fit the receiving terminal. We start with your actual wire and ferrule so the stripping setup and crimp tooling work together. Checking the first sample for trapped insulation, stray strands and terminal-block fit gives the operator a practical reference for the batch.
This workstation suits prepared cable ends and operator-paced production. For a shop that changes wire sizes repeatedly, count fixture changes and bowl adjustment alongside the cycle time when comparing the station with hand tools.
For leads that also need printed identification sleeves, see the WM-3244 number tube printing and ferrule workstation. Compare the WM-3116 servo ferrule crimping machine for a different tooling and wire-range requirement.
Send your wire sizes, ferrule dimensions and usual batch quantities. We will confirm the build and tooling with a sample-run video and an itemized quote.
Engineering knowledge
Choose and troubleshoot this process
- Ferrule Crimping: Strip Length, Terminal Fit and Chain-Fed vs Loose-Fed MachinesCompare chain-fed and loose-ferrule crimping machines by wire preparation, changeover, terminal fit and batch output. Check WM-3243 and WM-3246 specifications.
- How to Choose a Terminal Crimping MachineChoose a terminal crimping machine by terminal presentation, wire range, applicator standard, required process steps, inspection method and production mix.
- Terminal Crimp Defects: Causes, Inspection and Corrective ActionsTroubleshoot low pull force, incorrect crimp height, strand loss, bellmouth defects, insulation support problems and inconsistent terminal feeding.
WM-3246 — common questions
Is this a 0.5–4 mm² or a 0.3–4 mm² machine?
The datasheet lists six BVR wire sizes from 0.5 to 4 mm². The configuration table lists 0.3–4 mm² and an optional enlargement to 16 mm². We confirm the selected build, fixtures and sample results before ordering; the optional range is not the standard range shown in the summary.
What determines whether my ferrules will run?
The insulating collar must be round and no longer than 7.5 mm. We also check the barrel dimensions, wire insulation and conductor construction when matching the feeding and crimping tooling. Send the actual ferrule and wire, together with the terminal block it must fit.
Does a 2.5-second cycle mean 1440 finished wires per hour?
The 2.5 seconds describes the machine cycle. Operator loading, cable handling, changing parts and inspection add time. We record a sample run using your cable preparation and batch sequence so you can assess practical output.
Does it print or insert identification sleeves?
This configuration strips and crimps insulated ferrules. For integrated number-tube printing and insertion, compare our WM-3244 workstation linked below.
What inspection is included?
The listed checks cover ferrule presence and right-side safety-door opening. Presence detection does not measure crimp strength. We agree the required sample checks, including pull testing where needed, with your wire and ferrule specification.
How are training and replacement parts handled?
We set the voltage for your country and ship the English interface and manual. For blades, gripping parts and crimp-tool wear parts, every quote lists them with unit price and the location they ship from. We confirm the installed wire range and tooling on that same quote.
Related machines in Crimping & Connector Assembly

10-Ton Servo Terminal Crimping Machine, 100 kN Bench Press
Model WM-3110T

20-Ton Servo Cable Lug Crimping Machine, 200 kN and 40 mm Stroke
Model WM-3120T

2-Ton Servo Terminal Crimping Machine, 20 kN Touchscreen Bench Press
Model WM-3102S