Single-Side Infrared Heat Shrink Machine with 200 mm Teflon Conveyor WM-662A
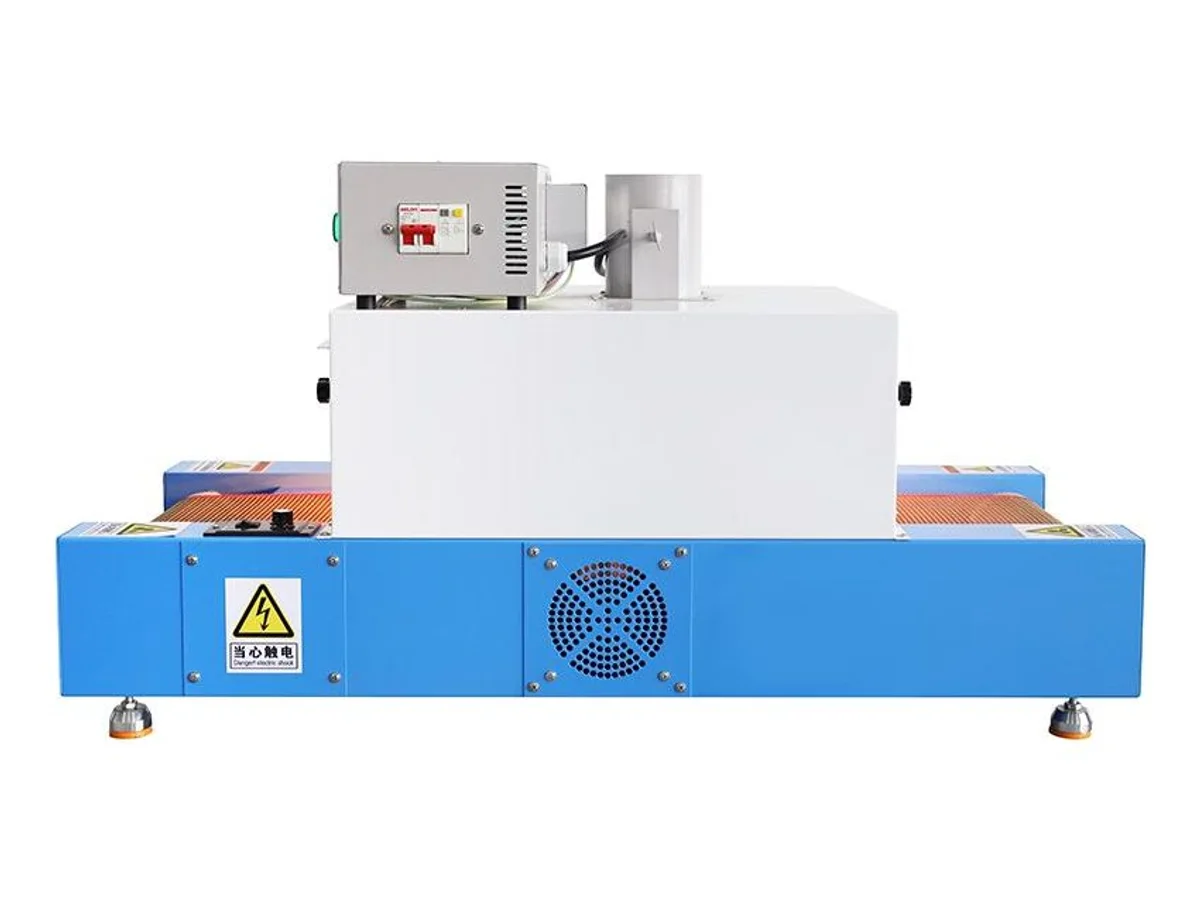
The WM-662A shrinks tube in continuous flow — parts ride a 200 mm Teflon mesh belt under six 300 W infrared tubes that heat from the top down. Belt speed is steplessly adjustable from 0.5 to 3 m/min over a 520 × 460 mm heating area, so dwell time is set once per product. The controller holds temperature to ±2 °C with a ceiling above 200 °C, and the throat passes work up to 250 mm wide and 100 mm high. The bench unit measures 1000 × 460 × 465 mm and draws 1,860 W on 220 V.
Specifications
| Function | Conveyor-fed infrared shrinking of heat shrink tube, single-side (top-down) heating |
|---|---|
| Heating element | Infrared heating tubes, 300 W × 6 |
| Heating direction | Top down, single side |
| Heating area | 520 × 460 mm |
| Maximum temperature | > 200 °C |
| Temperature accuracy | ± 2 °C |
| Conveyor belt | Teflon mesh, 200 mm wide, 0.5 – 3 m/min stepless |
| Belt motor | 25 W, stepless speed regulation |
| Max. workpiece | 250 mm wide, 100 mm high (height adjustable) |
| Machine size | 1000 × 460 × 465 mm |
| Control box | 200 × 150 × 200 mm |
| Power | 1,860 W, 220 V |
| HS Code | 8419.89 (common reference — final classification confirmed by your customs broker) |
| Certification | CE (certificate provided with shipment) |
Key features
- Parts flow through on the belt instead of being presented one by one to a gun — loading and unloading is the only manual work left in the shrink step
- Belt speed dials dwell time from 0.5 to 3 m/min, so the exposure can be adjusted for each product; verify part temperature and shrink quality during the trial
- ±2 °C control under a 200 °C-plus ceiling lets you set the process for marker sleeves and thin-wall tube; confirm shrink quality and legend readability on your material
- The Teflon mesh belt neither sticks to softened tube nor shields it from heat, and parts up to 250 mm wide and 100 mm high pass straight through
What it processes
- Shrinking pre-cut tube over cable ends, plug joints and handle grips in continuous batches
- Sleeving cylindrical parts and small assemblies where the shrink zone faces up on the belt
- Post-print shrinking of identification sleeves at steady, repeatable temperature
Suited for: continuous-flow shrinking of parts that lie flat with the shrink zone facing up — cable ends, sleeved cylindrical parts, printed marker tube — at one proven temperature and belt speed per product. Not suited for: thick bundles and long sheathing that need heat from all sides at once — for harness sections up to Ø100 mm, pick the WM-664 infrared harness oven with its enclosed chamber — nor for cutting or positioning the tube itself; cutting tube to length is the WM-565N cutter’s job.
Shrink results depend on your tube and part together, so we prove them as a pair — send a handful of your parts with the exact tube you use, and we run them through this machine on video and mail the shrunk samples back before you order.
Engineering knowledge
Choose and troubleshoot this process
- Heat Shrink Defects: Causes and Corrective ActionsTroubleshoot incomplete recovery, wrinkles, splits, scorching, sleeve movement, trapped air, uneven adhesive flow and heat damage.
- How to Choose Heat Shrink Processing EquipmentChoose heat shrink equipment by sleeve material, recovered dimensions, adhesive requirement, harness geometry, heating method, takt time and validation plan.
WM-662A — common questions
What does single-side heating mean in practice?
All six infrared tubes sit above the belt and radiate downward. Work laid flat with the shrink zone facing up — cable ends, sleeved parts, printed markers — shrinks evenly as the tube conducts heat around itself. There is no heat source under the belt, so the carrier side stays gentler.
How do I set it up for a new tube size?
Two adjustments — temperature on the ±2 °C controller and belt speed between 0.5 and 3 m/min across the 520 mm-long heating zone. Slower belt for thick-wall or large-bore tube, faster for thin marker sleeves. Both settings are visible on the panel, so a proven recipe is written down and repeated next batch.
What is the WM-662A not the right machine for?
All-round chamber shrinking of thick harness bundles and long sheathing runs, where heat must surround the part — the tunnel ovens with enclosed chambers in the heat shrink processing category do that. It also does not cut or position tube; it only shrinks what is already in place.
Related machines in Heat Shrink & Tube Insertion
Bench-Mount Hot Air Heat Shrink Machine with Through-Table Air Outlet
Model WM-667ZM
Crawler Belt Heat Shrink Tunnel Oven for Continuous Wire Sleeve Shrinking
Model WM-666
Double-Sided Far-Infrared Heat Shrink Conveyor Oven with Teflon Mesh Belt
Model WM-670PH