Roll-In Cable Reel Pay-Off Machine, 250 kg Capacity WM-9334
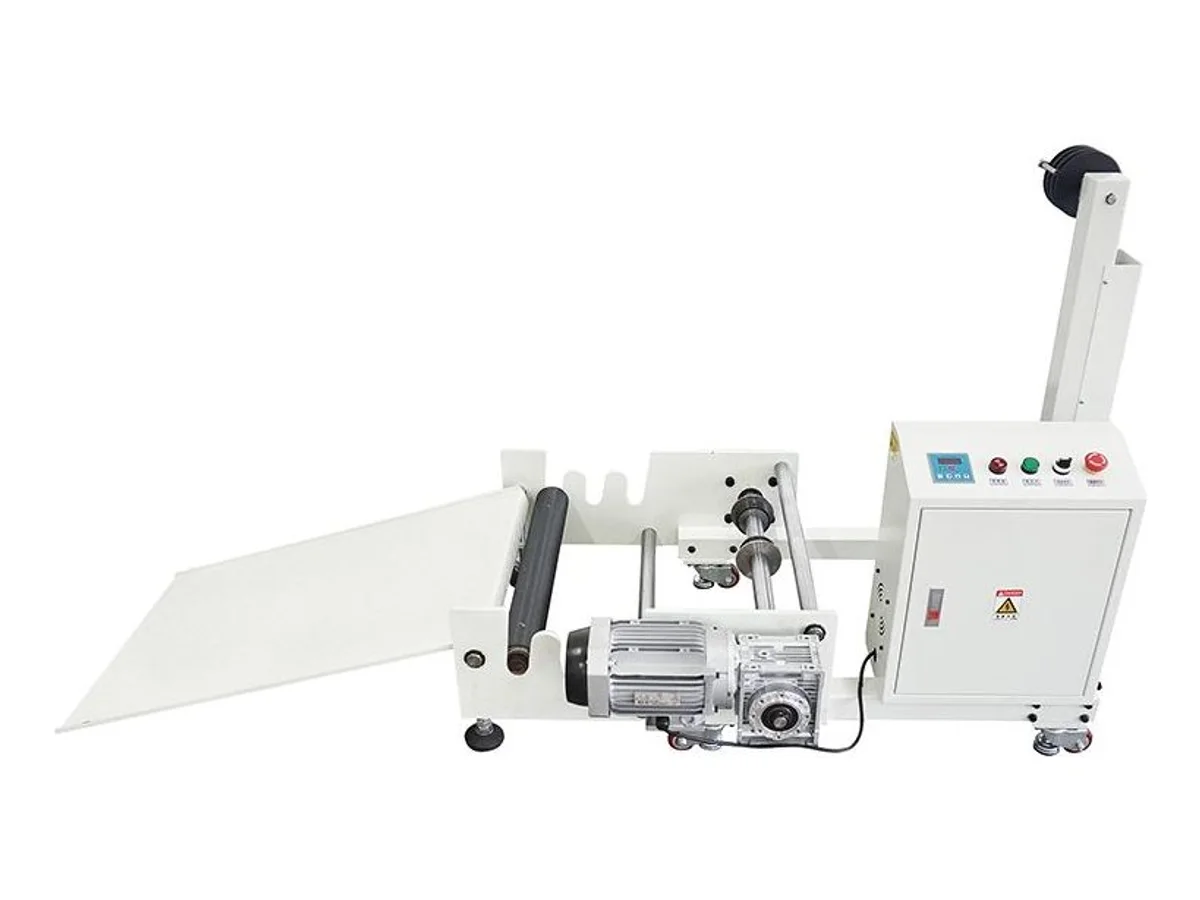
The WM-9334 is a motorised wire spool dereeler for spools up to Ø450 mm carrying 250 kg, feeding wire and cable up to 16 mm at speeds to 3 m/s. Instead of a through-shaft the spool sits in a notched roller cradle that is loaded from a tread-plate ramp, so a full spool is rolled into position rather than lifted. Speed is infinitely variable with no manual setting, and active feeding with automatic induction and a brake starts and stops the spool with the machine downstream. The reference supply is 220 V and the frame measures 800 × 600 × 1,000 mm.
Specifications
| Model | WM-9334 |
|---|---|
| Function | Automatic wire spool dereeling (powered pay-off / prefeeding) |
| Downstream machines | Fully automatic terminal crimping machine, wire cutting machine, wire stripping machine, wire soldering machine |
| Wire size | ≤ 16 mm |
| Spool diameter | 450 mm |
| Load-bearing | 250 kg |
| Speed | 3 m/s |
| Speed control | Infinitely variable — no manual speed adjustment needed |
| Feeding | Active wire feeding; automatic induction with brake; guide rail at constant speed, no resistance |
| Guide wheel | Adjustable to suit the wire diameter; low-noise operation |
| Power supply | Reference configuration: 220 V |
| Dimensions | 800 × 600 × 1,000 mm |
| Electrical configuration | We configure the machine’s electrical supply for your installation before shipment. Your quote confirms the voltage, phase, frequency, current and the power cord with plug or industrial connection for your site. Common site supplies are 120 V, 60 Hz with grounded Type B outlets in the US and Canada, with 208 V or 240 V also found at industrial sites. The UK and Ireland use 230 V, 50 Hz with Type G. Australia and New Zealand use nominal 230 V, 50 Hz with Type I, and some Australian sites list 240 V. Three-phase installations in the UK, Ireland, Australia and New Zealand commonly use 400 V at 50 Hz, with 415 V at some Australian sites. |
| Lead time | Your quote confirms the machine configuration, included accessories and dispatch date. |
| Warranty and support | One-year machine warranty and free remote video support for the life of the equipment. |
| Wear parts | For wear parts, every quote lists them with unit price and the location they ship from. |
| HS Code | 8479.89 (common reference — final classification confirmed by your customs broker) |
| Certification | CE (certificate provided with shipment) |
Key features
- 250 kg spool rating on the single-phase 220 V reference build — five times the 50 kg load of our next-largest 220 V pay-off, without moving up to a three-phase machine
- Takes spools up to Ø450 mm and pays off wire and cable up to 16 mm at speeds to 3 m/s
- Infinitely variable speed with automatic induction and brake, so the spool follows the downstream machine's demand instead of running at a fixed rate
- As pictured, the spool rests in a notched cradle on horizontal rollers rather than on a through-shaft — no shaft to thread through the hub and no sleeve set to keep in stock for different bores
- As pictured, a diamond-tread ramp plate on each side of the cradle, so a full spool is rolled up into position instead of lifted onto a shaft
- As pictured, a stacked multi-groove guide sheave on the outfeed shaft — pick the groove that matches the wire, no tooling change
- As pictured, the outfeed sheave rides on a vertical linear guide with a sensor bracket at the top of its travel, so the wire path can rise and fall between the spool's rotation and the cutter's intermittent pull
- Levelling feet and casters on the same frame, and a panel with inverter speed display, alarm, indicator, forward/reverse and mushroom-head power switch
What it processes
- Feeding automatic terminal crimping machines from full mill spools
- Prefeeding wire cutting and stripping machines that would otherwise have to drag a heavy spool
- Supplying automatic wire soldering and tinning cells
- Lines where cable arrives on Ø450 mm spools too heavy to lift onto a shaft-type stand but too small for a 1.5 t mill-spool pay-off
Suited for: powered pay-off of spools up to Ø450 mm and 250 kg, wire and cable up to 16 mm, at speeds to 3 m/s on the 220 V reference build — standing in front of a wire cutting and stripping machine, a crimping cell or a soldering machine. For other jobs and machine options: mill spools of Ø600–1,250 mm carrying up to 1.5 t, which need the three-phase 380 V WM-9151 heavy-duty large cable prefeeder and its Φ3–45 mm cable range. Loose coils delivered without flanges will not sit in this cradle — they belong on the 550 mm flat turntable of the WM-9309 prefeeding machine at 50 kg, or between the closing flanges of the WM-9332 compact pre-feeder and dereeler stand for Ø200–300 mm reels at ≥15 kg. If your reels are light and your line is faster than 3 m/s, the WM-9150 variable-speed pay-off runs 50 kg reels at 4 m/s. Corrugated tube, hose and PVC tube run on the WM-9120T cable and tube prefeeder at 20 kg, and tension-sensitive Ø0.6–5 mm coaxial cable needs the dancer loop of the WM-9105C coax prefeeder at 25 kg.
The gap this machine fills
Powered pay-off equipment splits into two clusters. Below it sit the bench-class stands — 15 kg, 20 kg, 25 kg, 50 kg — built around a shaft or a turntable, loaded by one person lifting one reel. Above it sit the mill-spool machines: 1.5 t, three-phase 380 V, shaftless cone chucks, five-and-a-half kilowatts of drive, and a footprint to match.
Between the two is the spool a buyer actually receives most often from a cable mill: around Ø450 mm, a couple of hundred kilograms, and awkward in both directions. It is far too heavy for a 50 kg stand and its operator, and it is undersized for a machine whose smallest listed spool is Ø600 mm. The WM-9334 is built for exactly that band — 250 kg on a Ø450 mm spool, on the reference single-phase 220 V build, still at 3 m/s.
Loading through the cradle ramp
The design consequence of 250 kg is visible in the gallery. There is no through-shaft. The spool lies in a cradle formed by two side plates cut with a row of notches; horizontal rollers drop into the notches, and the notch pair you choose sets the cradle width to the flange diameter in front of you. One roller is rubber-covered and driven through a worm gearbox, so the spool is turned by friction on its own flanges rather than by a mandrel through the hub.
Either side of the cradle is a hinged tread-plate ramp. A full spool is stood on edge and rolled up the ramp into the cradle. The cradle avoids a through-shaft and matching hub sleeve; handling equipment and personnel must be selected for the actual loaded reel and workshop conditions. Levelling feet take the load once the machine is positioned; casters let it be pushed to the next cell when it is not.
Following demand, then stopping
A pay-off matters most in the half-second after the cutter stops. Rotational inertia at 250 kg is unforgiving: an unbraked spool keeps turning, throws a loop of cable on the floor and hands the next cycle a length error.
Two mechanisms answer that. The drive is infinitely variable with no manual speed setting, so it tracks the rate the downstream machine is actually consuming rather than running at a preset. And the feed is active with automatic induction and a brake — the spool is driven up when wire is drawn and taken out of rotation when the line stops.
The buffer between them is the guide sheave at the outfeed end. It rides on a vertical linear guide with a sensor bracket at the top of its travel, so the wire path can rise and fall between the spool’s steady rotation and the cutter’s intermittent pull. The sheave itself is a stack of grooves of different widths: choose the groove that matches the wire and the pay-off point is set, without a tooling change. That is also what makes the 16 mm ceiling a working figure rather than a nominal one.
Reading the numbers before you order
Three of the published figures deserve a second look.
The 450 mm spool diameter is a hard limit set by the cradle geometry, not a guideline — a 600 mm spool will not sit between these side plates, whatever it weighs. The 250 kg rating and the 3 m/s speed are stated for the machine, not for your material: a 250 kg spool of stiff 16 mm cable and a 250 kg spool of fine wire accelerate very differently, and top speed is rarely the constraint on a heavy spool.
Net weight, motor rating in watts and feeding height are confirmed on the quote. If any of the three affects your layout — mezzanine floor loading, infeed height into an existing machine, or the supply budget for the cell — tell us with your inquiry so the configuration can be confirmed before you order. For a WM-9334 quote, share what you need to feed and the size of the reel or coil it comes on. We’ll check how the unit would fit your line.
Engineering knowledge
Choose and troubleshoot this process
- How to Choose a Wire Prefeeder and Pay-Off SystemChoose a wire prefeeder or pay-off system by reel mass, line speed, acceleration, allowable tension, accumulation, dereeling control and downstream interface.
- Wire Feeding Problems: Causes and Corrective ActionsTroubleshoot cable tension spikes, reel overrun, loops, jerking, twist, feed slip, encoder mismatch and downstream cut-length variation.
WM-9334 — common questions
How large a spool does the WM-9334 take?
The stated limits are a spool diameter of 450 mm and a load of 250 kg, with wire up to 16 mm. Send the spool drawing with flange diameter, width, hub bore and full weight before ordering — two spools of the same weight can behave very differently during acceleration and braking, and the cradle notch positions have to suit your flange diameter.
Why a roller cradle instead of a shaft?
A 250 kg spool cannot reasonably be lifted onto a shaft by hand. In the cradle the spool lies on horizontal rollers between notched side plates and is turned by the drive roller, so it is rolled up the tread-plate ramp into position. It also removes the need to stock sleeves for different hub bores, because nothing passes through the hub.
How does it keep pace with my cutting machine?
Speed is infinitely variable and the drive uses automatic induction with a brake, so the spool accelerates when wire is drawn and is braked when the line stops. The guide sheave on its vertical rail carries the buffer between the two. There is no data connection to configure, so the machine can stand in front of most wire processing equipment that pulls from a loop.
What supply does it need?
The reference supply is 220 V. We confirm the connection for your plant on the quote. Note that the machine sits below the three-phase 380 V class — if your spools are Ø600 mm or larger, that is a different machine, linked at the top of this page.
What is not published for this model?
Net weight, motor rating in watts and feeding height are confirmed on the quote. Tell us if floor loading, delivery height or cell power draw affects your layout so we can confirm these figures before you order.
Related machines in Wire Feeding & Pay-Off
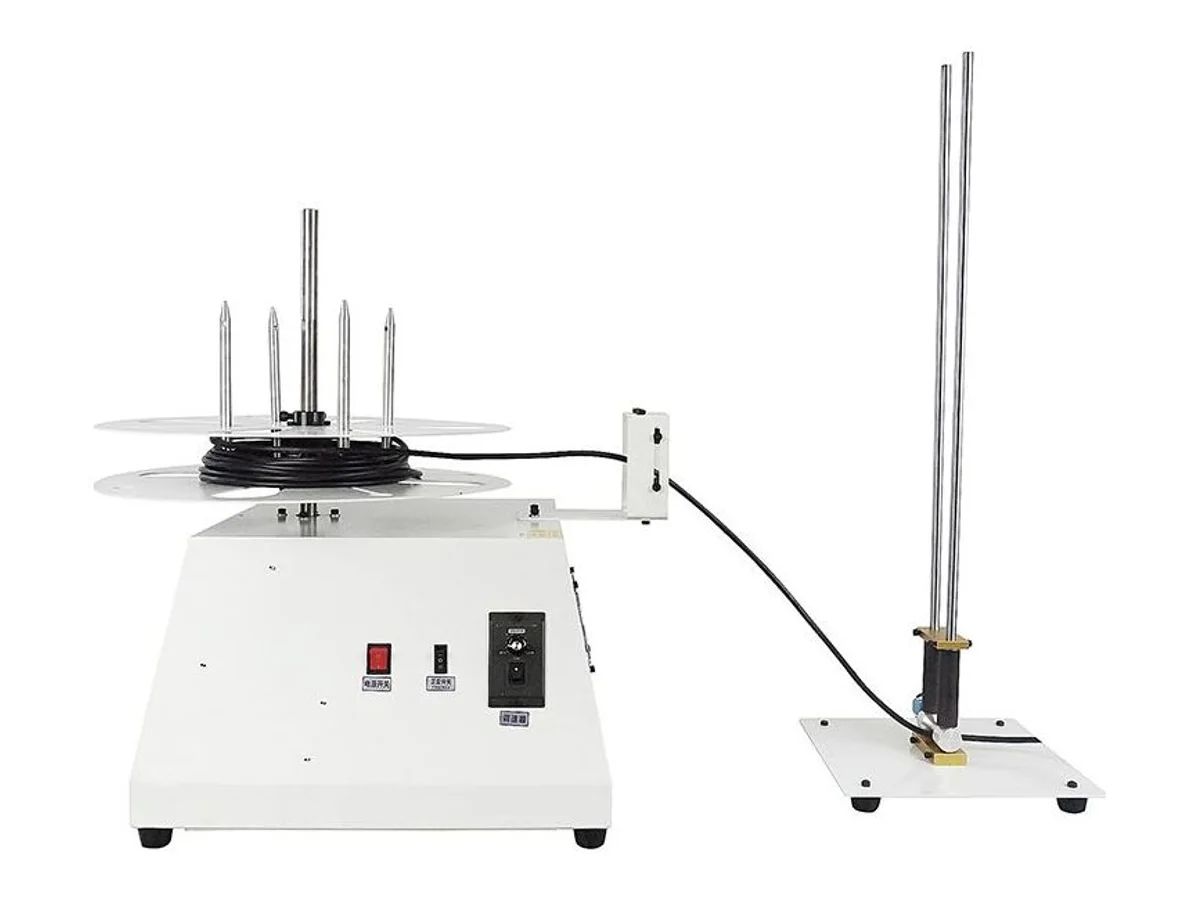
Automatic Cable and Tube Prefeeder with 20 kg Load Capacity
Model WM-9120T
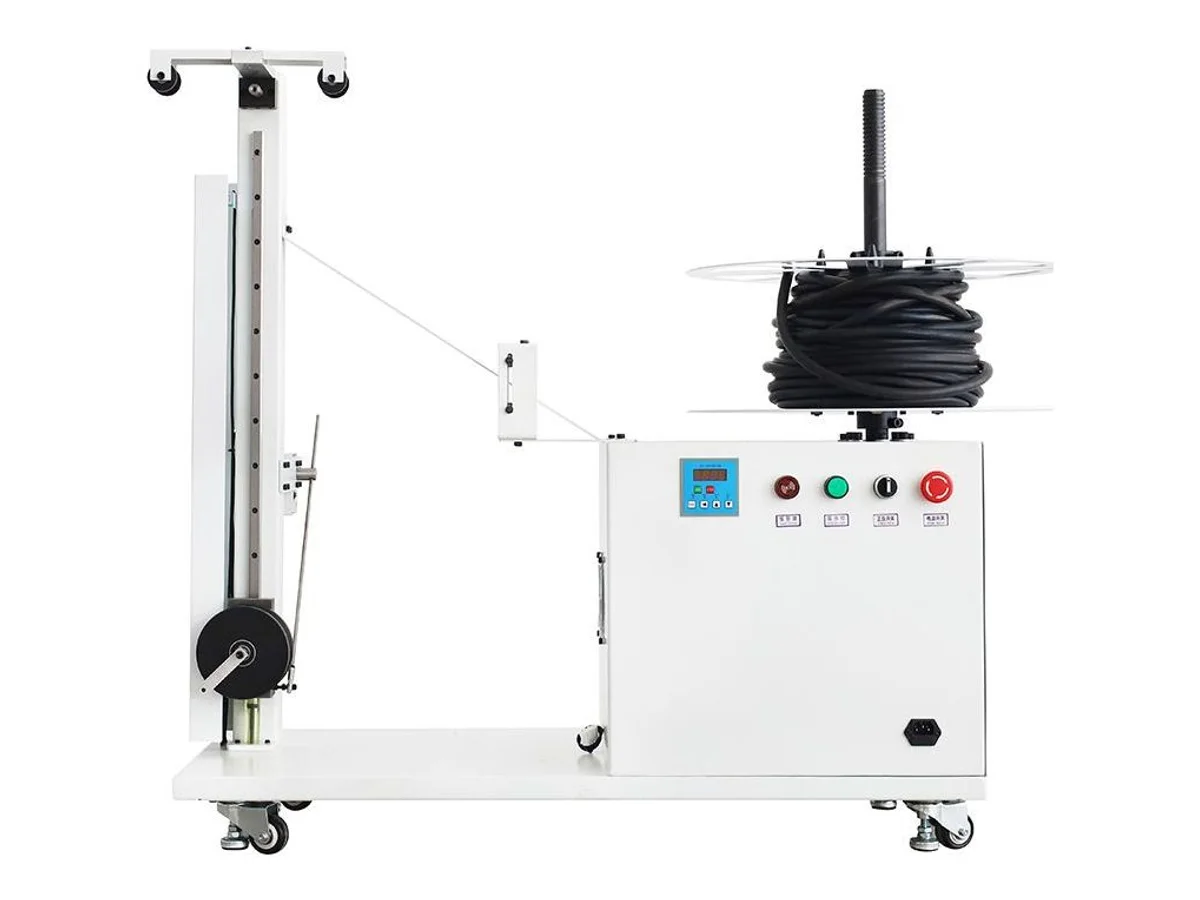
Automatic Variable-Speed Wire Pay-Off Machine with 50 kg Reel Capacity
Model WM-9150
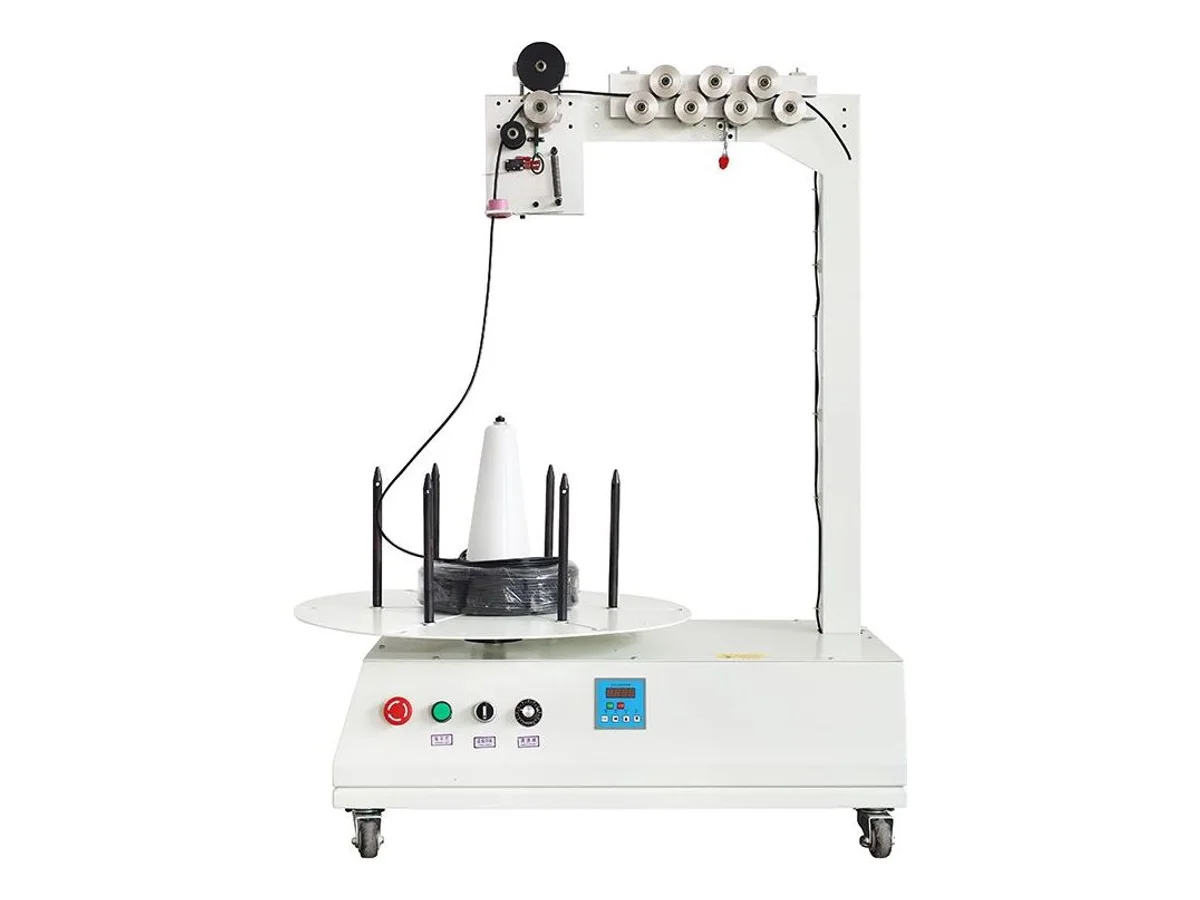
Automatic Wire Prefeeder for Reels and Loose Coils, 50 kg
Model WM-9309