Heat Shrink Tube Heating Machine with 400 × 200 mm Tunnel Furnace WM-674
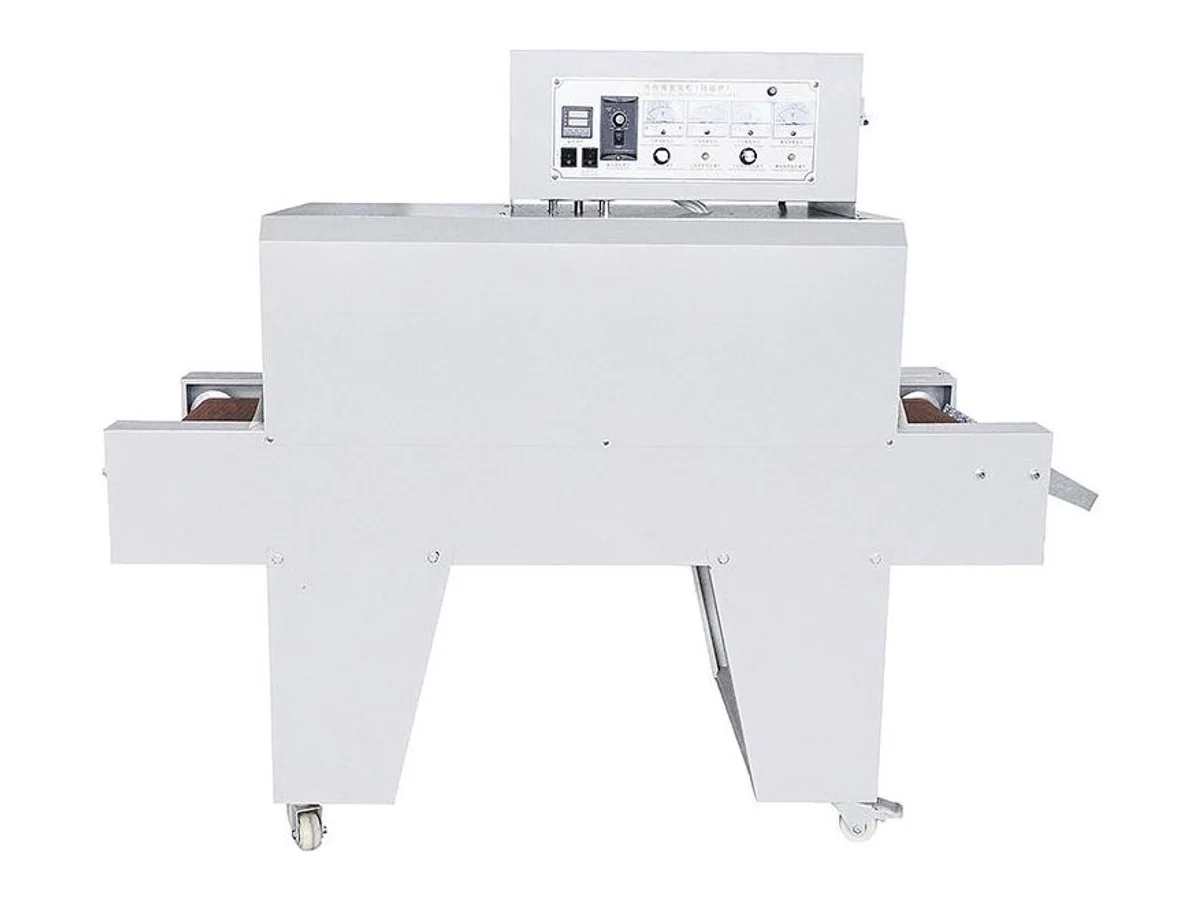
The WM-674 shrinks tube inside an enclosed tunnel furnace — a 1000 mm-long chamber with a 400 mm wide, 200 mm high opening that passes work up to 390 × 190 mm in cross section at any length. Heater banks above, below and at the sides work together with a hot-air circulation fan, so heat reaches the tube from all around instead of one face, with chamber temperature adjustable from 0 to 300 °C. A chain conveyor rated for 10 kg carries parts through (mesh and Teflon belt variants available), and the 8 kW, 380 V three-phase unit is built for round-the-clock production shifts.
Specifications
| Function | Tunnel furnace heating of heat shrink tube, conveyor fed |
|---|---|
| Tunnel opening (W × H) | 400 × 200 mm |
| Applicable product size | 390 × 190 × N mm (W × H × L) |
| Applicable materials | PVC, POF, PET, PP |
| Temperature control | 0 – 300 °C, adjustable |
| Furnace chamber size | 1000 × 400 × 200 mm (L × W × H) |
| Conveying mode | Chain type or mesh type; Teflon belt and net-through chain type as non-standard options |
| Conveying load | 10 kg |
| Voltage | 380 V, three-phase four-wire |
| Current | 22 A |
| Power | 8 kW |
| Machine size | 1500 × 550 × 1270 mm (L × W × H) |
| Machine weight | 90 kg |
| Packing volume | 1 m³ |
| HS Code | 8419.89 (common reference — final classification confirmed by your customs broker) |
| Certification | CE (certificate provided with shipment) |
Key features
- Heat comes from all around — upper, lower and side heater banks each have their own voltage dial and meter on the panel, and a circulation fan in the chamber roof evens the hot air out, so tube shrinks on the shadow side too
- The 400 × 200 mm opening is the point — bundles, connector bodies and assemblies up to 190 mm tall ride straight through, where flat belt ovens stop at a fraction of that clearance
- Chamber temperature adjusts from 0 to 300 °C and heating time is set to the product, so one furnace covers PVC, POF, PET and PP tube and film
- Chain conveyor as standard carries 10 kg of product through the 1-meter chamber; mesh, Teflon belt and net-through chain versions are available where the parts call for them
- 8 kW of three-phase heating power is sized for continuous shifts — the furnace holds temperature under a steady stream of parts instead of sagging after each batch
- Free sample test — send your parts with the tube already positioned, we run them through this furnace and send you the video plus the shrunk samples before you order
What it processes
- Shrinking sleeves and protective sheathing on wire harness bundles and cable assemblies too tall for flat conveyor ovens
- Heat shrinking PVC, POF, PET and PP tube or film over plugs, connector bodies and small assemblies in continuous flow
- Round-the-clock shrink lines where parts arrive steadily and the furnace must hold temperature all shift
Suited for: all-around shrinking of PVC, POF, PET and PP tube and film on bulky work — harness bundles, plug and connector bodies, assemblies up to 390 mm wide and 190 mm tall — fed continuously through an enclosed 300 °C tunnel on a 10 kg-rated chain conveyor, on lines that run all shift. Not suited for: high-count small end sleeves under Φ10 mm on individual wires — the WM-666 crawler belt tunnel oven feeds wire after wire at around 2,000 pieces per hour; nor for cutting and placing the tube itself — the WM-663 inserting and heating machine cuts, inserts and shrinks sleeve onto wire ends in one 2.5-second cycle. If your shop has no 380 V three-phase supply, the 220 V WM-670PH double-sided conveyor oven covers work up to 80 mm tall.
Shrink results depend on your tube, your part and the heat profile together — send a handful of parts with your tube positioned, and we run them through this furnace on video, with the panel settings in frame, and mail the shrunk samples back before you commit to the order.
Engineering knowledge
Choose and troubleshoot this process
- Heat Shrink Defects: Causes and Corrective ActionsTroubleshoot incomplete recovery, wrinkles, splits, scorching, sleeve movement, trapped air, uneven adhesive flow and heat damage.
- How to Choose Heat Shrink Processing EquipmentChoose heat shrink equipment by sleeve material, recovered dimensions, adhesive requirement, harness geometry, heating method, takt time and validation plan.
WM-674 — common questions
What size of work fits through the tunnel?
The opening is 400 mm wide and 200 mm high, and the usable product envelope is 390 × 190 mm in cross section at any length — the 1000 mm chamber heats long parts in a continuous pass. The conveyor is rated to carry 10 kg of product at a time. If your part clears 390 × 190 mm, it goes through; send us the dimensions and we confirm against the actual machine.
How is the heating adjusted for a new product?
Chamber temperature is set between 0 and 300 °C, and the panel gives each heater bank — upper, lower and side — its own adjustment dial with a voltage meter, plus a separate control for the hot-air circulation fan and conveyor speed. That lets you bias heat toward the top or bottom of the part until the tube recovers evenly, then the dial positions become the recipe you write down and repeat.
What is the WM-674 not the right machine for?
High-count shrinking of small end sleeves on individual wires — a wire-fed machine like the WM-666 crawler belt oven does thousands of pieces per hour with less energy. It also only heats — it does not cut tube to length or slide it onto the wire; upstream machines in the heat shrink processing category handle those steps.
Related machines in Heat Shrink & Tube Insertion
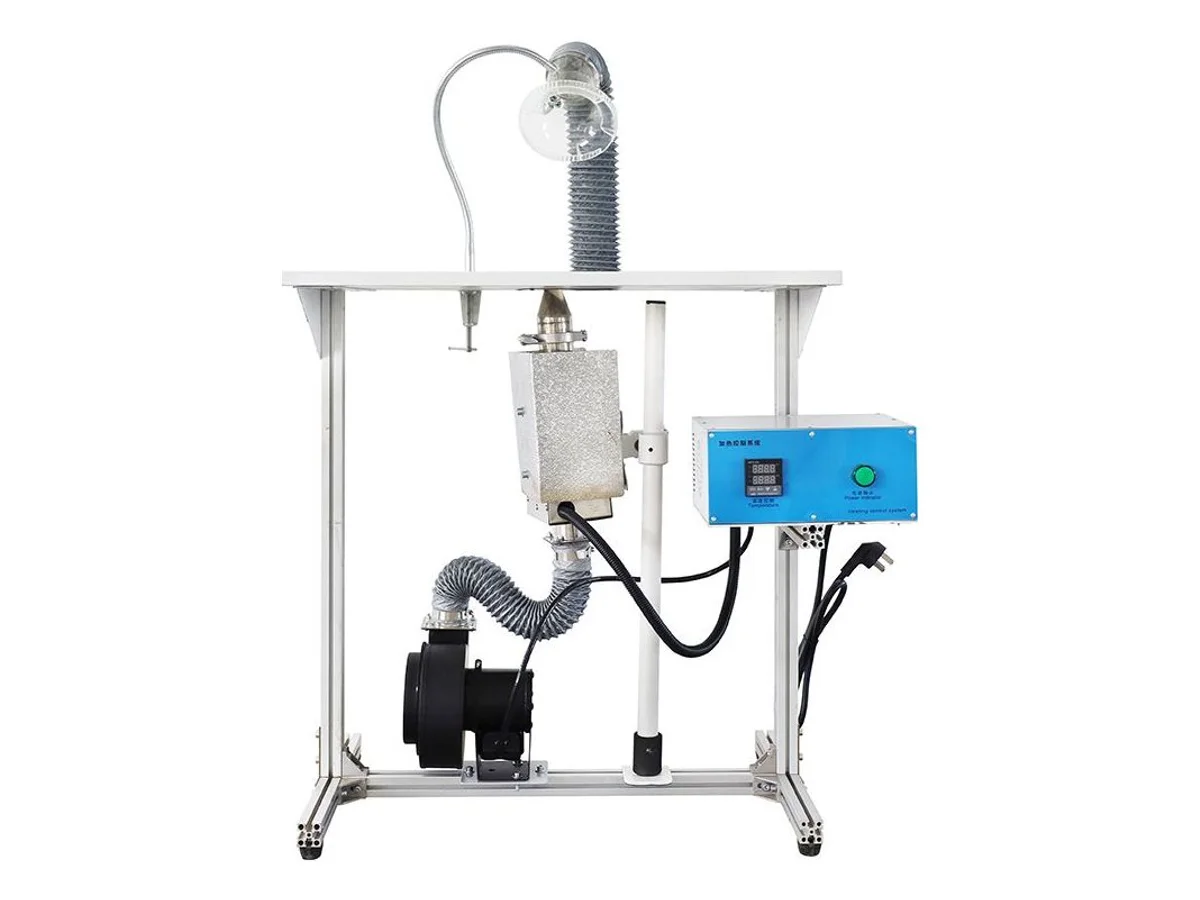
Bench-Mount Hot Air Heat Shrink Machine with Through-Table Air Outlet
Model WM-667ZM
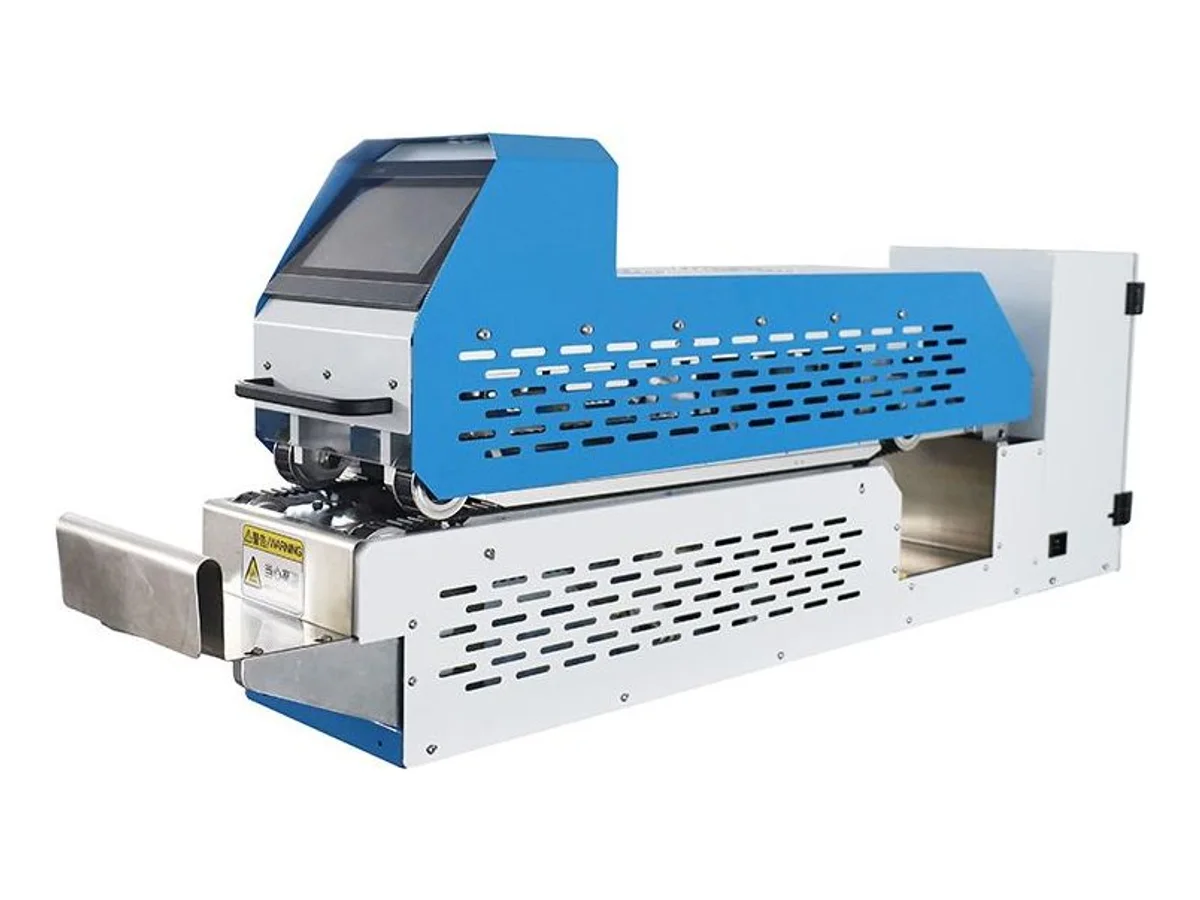
Crawler Belt Heat Shrink Tunnel Oven for Continuous Wire Sleeve Shrinking
Model WM-666
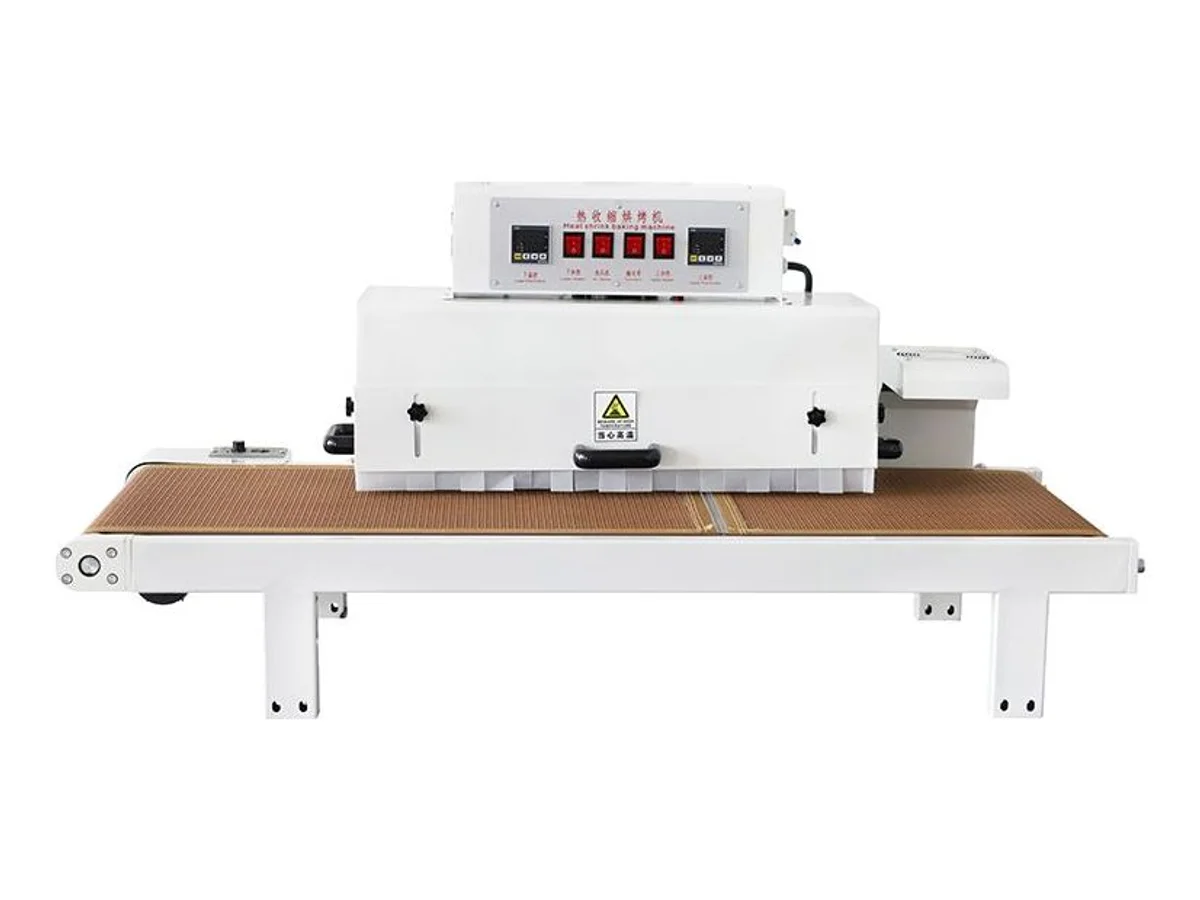
Double-Sided Far-Infrared Heat Shrink Conveyor Oven with Teflon Mesh Belt
Model WM-670PH